
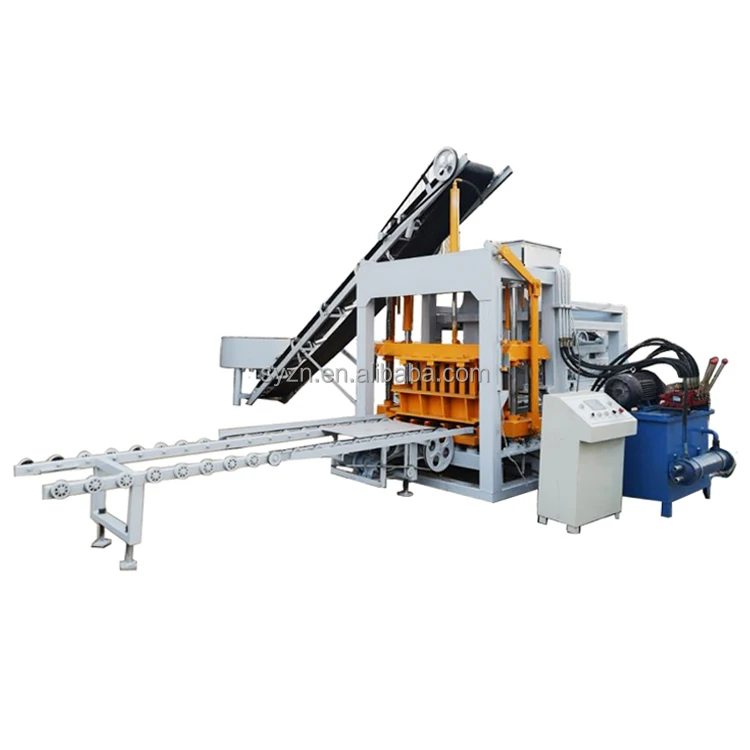
Matched System Integration — every upstream feeder and downstream pallet handler is specified to the QT4-20 cycle tempo so the press never starves or waits.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-20 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7100 × 1600 × 2610 mm |
| Rated Pressure | 16–21 MPa |
| Vibration Form | Platform Vibration |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 45 kN |
| Pallet Size | 1020 × 570 mm |
| Molding Cycle | 20–30 s |
| Overall Power | 27.5 kW |
| Total Mass | 6 T |
| Demolding Method | Hydraulic |
| General Water Consumption | 12 T/Day |
| Factory Area | 500 m² |
| Warranty | 1 year |
| Output Capacity | (basis to be confirmed) |
| Control System | (configurable — specify PLC or relay logic) |
| Voltage & Frequency | (configurable — confirm local supply before production) |
| Automation Level | (selectable from semi-automatic to fully automatic line) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, fly ash |
| Solid block manufacturing | Gravel, slag, cement blends |
| Paving block and colored paver runs | Fine aggregate with pigment additives |
| Interlocking brick and curbstone | Coarse aggregate with hydraulic compaction |
| Porous permeable brick | Open-graded aggregate with controlled water content |
Why Quoted Cycle Rates Rarely Survive the First Shift
A block making machine production line is only as fast as its slowest upstream or downstream station.
Suppliers routinely quote the QT4-20 at a 20–30 second molding cycle and leave it there. But if the mixer batch takes 45 seconds to discharge, or a worker is still hand-stacking the previous pallet when the press is ready to eject, the real output drops noticeably below the catalogue figure. I have walked onto sites where the press sat idle for a third of every hour simply because pallet return and block stacking were never part of the original quotation [NEED_CITE: common causes of block line throughput loss]. The turnkey concrete block plant concept exists to close exactly those gaps.
How Station Cycle Times Must Align Around the Press
Every station in a block making machine production line — raw material batching, mixing, pallet feeding, pressing, block stacking, and pallet return — has its own cycle. The QT4-20 completes a press cycle in 20–30 seconds, which means the mixer must deliver a fresh batch within that same window and the pallet feeder must place a new pallet before the press opens again. When any single station runs slower, the press waits and daily output shrinks proportionally.
Sizing the Pallet Circuit to Your Curing Layout
The QT4-20 runs on 1020 × 570 mm pallets, and the total pallet count must cover the press output plus the full curing rack inventory plus the return path. If the curing area is undersized or the forklift cannot handle that pallet dimension, wet blocks pile up at the press exit and the line stalls. Confirming pallet compatibility with existing racking and handling equipment before production avoids costly on-site improvisation [NEED_CITE: pallet handling best practices in block plants].
Reading the Specs That Actually Shape Output
Platform vibration at 4600 r/min combined with 45 kN force and 16–21 MPa hydraulic pressure determines block density and green strength. These three values must be matched to the buyer’s specific mix design — a fly-ash-heavy blend behaves differently under vibration than a pure crushed-stone mix. The 27.5 kW total power draw dictates the transformer and dedicated circuit requirements on site. A 500 m² factory area must accommodate raw material storage, the press, curing racks, and the pallet return loop without congestion, because cramped layouts force pallets to queue and the line tempo breaks down.
What Happens When Line Stations Are Specified Separately
When a buyer sources the mixer from one vendor, the stacker from another, and the pallet system from a third, nobody is responsible for the interfaces. The mixer discharge height may not match the hopper inlet. The stacker grip width may not fit the pallet. The result is a block making machine production line that technically runs but never reaches its designed rhythm, and the blame shifts between suppliers while the plant owner absorbs the downtime [NEED_CITE: risks of multi-vendor block line assembly].
Why the Line Is Quoted as One System Here
The QT4-20 is never treated as a standalone press in our proposals. Raw material feeding, mixing capacity, pallet circulation, stacking method, and curing rack handling are specified together so every station matches the press cycle. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Pallet dimensions are confirmed against the buyer’s existing curing area and forklift before production starts. Voltage, frequency, and control language are locked in writing so commissioning is not delayed by a mismatch at arrival. Installation includes operator training on the full line, not just the press.
Documentation & Verification
- Line layout drawing showing station positions, pallet flow path, and capacity per block format
- Machine specification sheet with hydraulic and electrical schematics for the QT4-20
- Pallet specification confirming material, thickness, and dimensional tolerance
- Voltage, frequency, and PLC display language confirmation sheet signed before production
- Factory test record documenting actual cycle times on the agreed block format
- Packing photographs and customs documentation support for the full line shipment
Installation, Commissioning & Support
- Foundation plan based on the QT4-20 footprint (7100 × 1600 mm) and 6 T operating mass
- Dedicated power circuit sized for 27.5 kW total load at the confirmed local voltage and frequency
- Pallet return conveyor aligned to curing rack height and forklift access route
- First-run commissioning with mix adjustment to achieve target block density at rated pressure
- Operator training covering mould change procedure, daily maintenance, and safety interlocks
- Wear parts list with hydraulic seals, vibration springs, and mould liner replacement intervals
What to Prepare Before Requesting a Quote
A turnkey concrete block plant proposal starts with your actual conditions. Provide the block formats you intend to produce and the target daily output per format. Share your local raw material sources — aggregate type, cement grade, and whether fly ash or slag is available. Confirm your site dimensions, existing curing racks, forklift specifications, and local voltage and frequency. If you already run upstream or downstream equipment, list it so the line can be designed around what you have.
Frequently Asked Questions
Q: How is daily output calculated, and which block format does the capacity figure assume?
A: Output depends on the block format, mould cavity count, and actual cycle time including pallet exchange. Any capacity figure must state the exact block dimensions and material assumed. We provide a line layout with per-format calculations so you can compare quoted output against your real production target before committing.
Q: What supporting equipment is included in the line quotation versus what I must source myself?
A: Our turnkey concrete block plant quotation lists every station — mixer, pallet feeder, stacker, curing rack handler — with model and specification. Items left to the buyer, such as the transformer or forklift, are flagged explicitly so there are no surprises when the line arrives on site.
Q: Is the 1020 × 570 mm pallet size compatible with my existing curing area and forklift?
A: Pallet dimensions must match your curing rack spacing and forklift tine width. We confirm pallet compatibility during the proposal stage and adjust the pallet specification if your existing equipment requires a different size, preventing costly modifications after installation.
Q: How do station cycle times align so the press is never left waiting?
A: Each upstream and downstream station is specified to complete its task within the QT4-20 molding cycle of 20–30 seconds. The line layout document shows the timing sequence so you can verify that no station creates a bottleneck before the equipment ships.
Q: What voltage, frequency, and control language will be configured before shipment?
A: These are confirmed in writing before production begins. The electrical schematic and PLC screen language match your local supply and operator requirements, so the line can be powered up and commissioned immediately on arrival without rewiring or reprogramming delays.



