
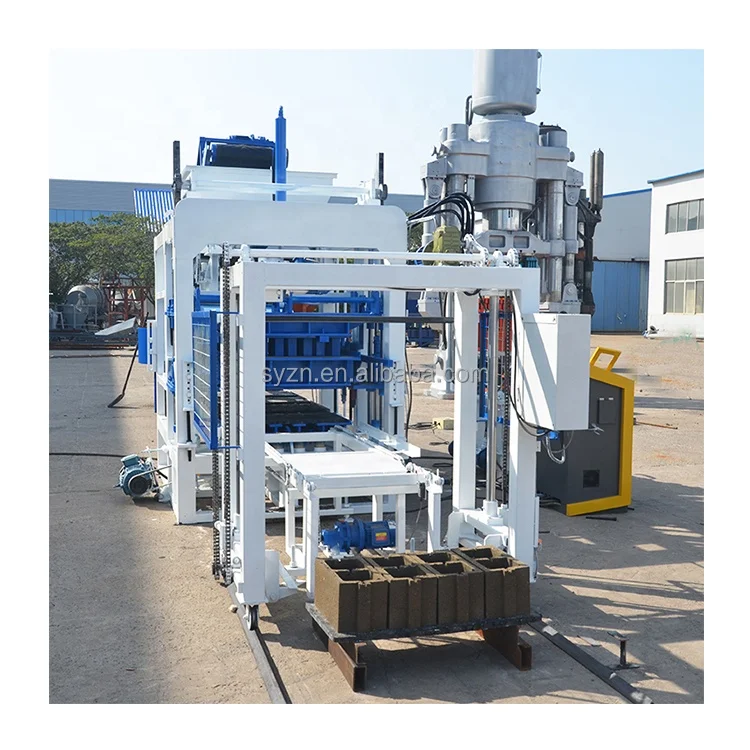
Matched Line Configuration — the QT4-18 press is specified alongside its JQ350 mixer, pallet feeder, brick conveyor, and self-loading stacker as one timed system, preventing stations from idling while upstream or downstream bottlenecks form.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Concrete Block Making Machine |
| Model | QT4-18 |
| Overall Dimensions (L×W×H) | 3900×1600×2300 mm |
| Total Weight | 3T |
| Rated Power | 24KW |
| Control System | PLC control system |
| Vibration Force | 40-50 KN |
| Pallet Size | 850×550×25 mm |
| Moulding Cycle | 15-25s |
| Output (Hollow 400×200×200mm) | 1200-1680 pcs/h (based on 15-20s cycle) |
| Output (Hollow 400×150×200mm) | 1800-2400 pcs/h (based on 15-20s cycle) |
| Output (Solid 240×115×53mm) | 3240 pcs/h (based on 15-20s cycle) |
| Included Line Equipment | Block making machine, hydraulic station, PLC control, pallet feeder, brick conveyor, block sweeper |
| Mixer Model | JQ350 |
| Stacking Method | Self-loading stacker |
| Mould Formats | Paver, solid block, hollow block, curbstone |
Application Suitability
| Application | Material or Output |
|---|---|
| Load-bearing hollow blocks | Crushed stone, cement, and local aggregate |
| Solid masonry bricks | Fly ash, dust, sand, and cement blends |
| Interlocking pavers | Fine aggregate with specific grading curves |
| Kerbstones for road edges | High-density mixes requiring high vibration force |
| First-plant setups | Complete line from raw feeding to stacking |
What "Pieces per Hour" Leaves Out About a Complete Block Production Line
A headline capacity figure is meaningless if the pallet feeder cannot keep up or the mixer runs dry.
I have seen block plants where the press sits idle for minutes every hour simply because the upstream batching or downstream stacking was never factored into the cycle time calculation. When planning a Concrete Block Production Line, the buyer often focuses entirely on the press. The reality is that if the JQ350 mixer cannot deliver a fresh batch every 15-25 seconds, the vibration force and hydraulic pressure of the QT4-18 are wasted on an empty mould box. Matching every station’s throughput is the only way to protect the investment [NEED_CITE: industrial line balancing principles for continuous manufacturing].
Synchronizing the Press with Upstream and Downstream Stations
This Concrete Block Production Line is built around the 15-25s moulding cycle of the QT4-18. The JQ350 mixer is selected specifically to match this rhythm, ensuring that the raw material feed never becomes the bottleneck that forces the press to idle.
Continuous Material Flow from Raw Feed to Curing Area
The inclusion of a dedicated pallet feeder and brick conveyor means the press does not wait for manual intervention. The self-loading stacker then removes the finished product, maintaining a steady flow from the vibration table through to the curing yard without manual pallet handling.
Verifying the Cycle Match Before Dispatch
Every station on this Concrete Block Production Line is tested together during the factory run. This confirms that the pallet feeding speed, the block sweeping mechanism, and the hydraulic station’s response time all align with the PLC-controlled press cycle, preventing the line from tripping its own sensors during continuous operation [NEED_CITE: PLC synchronization in automated block plants].
Interpreting the Pressure, Vibration, and Pallet Match
The 40-50 KN vibration force works in tandem with the hydraulic station to compact the mix into the mould. The 850×550×25 mm pallet size is a critical dimension; it must match the curing racks the buyer already has or plans to build. A mismatch here means buying new racks or forklifts. The PLC control system manages these timing sequences, but the operator must understand how the raw material moisture content affects the 15-25s cycle. If the local aggregate is too dry, the mix will not bind under the vibration force, and the block sweeper will clear debris that should have formed the block’s edge.
The Hidden Cost of Mismatched Line Stations
Buying a press without a specified pallet feeder often leads to operators hand-feeding pallets, which introduces a variable delay that the PLC cannot compensate for. This results in inconsistent block density. Furthermore, if the self-loading stacker is omitted, the curing area becomes a bottleneck where manual labor slows the entire Concrete Block Production Line to a crawl [NEED_CITE: manual handling bottlenecks in semi-automated plants].
Why Specifying the Full Line Matters Here
We specify the JQ350 mixer and the pallet feeder as part of the QT4-18 system because our single focus on block machinery means we do not assemble lines from unrelated suppliers. The line layout drawing we provide shows exactly where each station connects. The factory test record includes a run with your target block format, not just a generic hollow block. The hydraulic and electrical schematics confirm that the 24KW rated power is distributed correctly across all line stations. The pallet specification is confirmed against your curing area dimensions before production begins [NEED_CITE: importance of matched system integration in block making].
Documentation & Verification
- Line layout drawing showing station connections and cycle time matching points.
- Capacity calculation stated per block format with the assumed 15-25s cycle.
- Pallet specification confirming the 850×550×25 mm size and material grade.
- Factory test record on your target format before dispatch.
- Hydraulic and electrical schematic for the complete line stations.
Installation, Commissioning & Support
- Foundation requirements based on the 3900×1600×2300 mm footprint and 3T weight.
- Voltage and frequency confirmation for the 24KW PLC system before wiring.
- Assembly of the self-loading stacker and brick conveyor on site.
- Cycle time tuning of the JQ350 mixer to match the QT4-18 press rhythm.
- Operator training on mould change procedures for paver and hollow block formats.
- Wear parts list covering hydraulic seals and vibration table components.
Preparing Your Site and Material Data
To ensure the QT4-18 Concrete Block Production Line is configured for your facility, we need to know your local aggregate grading and moisture content. Please provide the dimensions of your existing curing area so we can verify the 850×550×25 mm pallet compatibility. Confirm the local voltage and frequency to ensure the PLC control system is programmed correctly before shipment.
Frequently Asked Questions
Q: How is daily output calculated per block format and what cycle time is assumed?
A: The output is calculated based on the specific block dimensions and a 15-20s moulding cycle. For a 400×200×200mm hollow block, the rate is 1200-1680 pcs/h. This figure assumes the JQ350 mixer and pallet feeder maintain a continuous feed without interruption.
Q: Are the mixer, pallet feeder, and stacker included in the line quotation?
A: Yes, the JQ350 mixer, pallet feeder, brick conveyor, block sweeper, and self-loading stacker are included as standard line stations. This ensures the Concrete Block Production Line is quoted as one matched system rather than separate, uncoordinated components.
Q: How do the cycle times of each station match so the press is not idle?
A: The JQ350 mixer batching speed is timed to the 15-25s press cycle. The pallet feeder and brick conveyor operate in sequence with the PLC control system to ensure the press always has a pallet ready and a clear path for the finished block.
Q: What pallet size is specified and how does it align with my curing area?
A: The line is configured for an 850×550×25 mm pallet. We require the buyer to confirm their curing rack spacing and forklift dimensions beforehand to ensure the self-loading stacker can place the pallets correctly without manual adjustment.
Q: What raw material mix design is the line configured for?
A: The vibration force and hydraulic pressure are set based on the buyer’s local aggregate and target block strength. If the local sand has high clay content, the mixer and press settings are adjusted during commissioning to maintain block density.



