
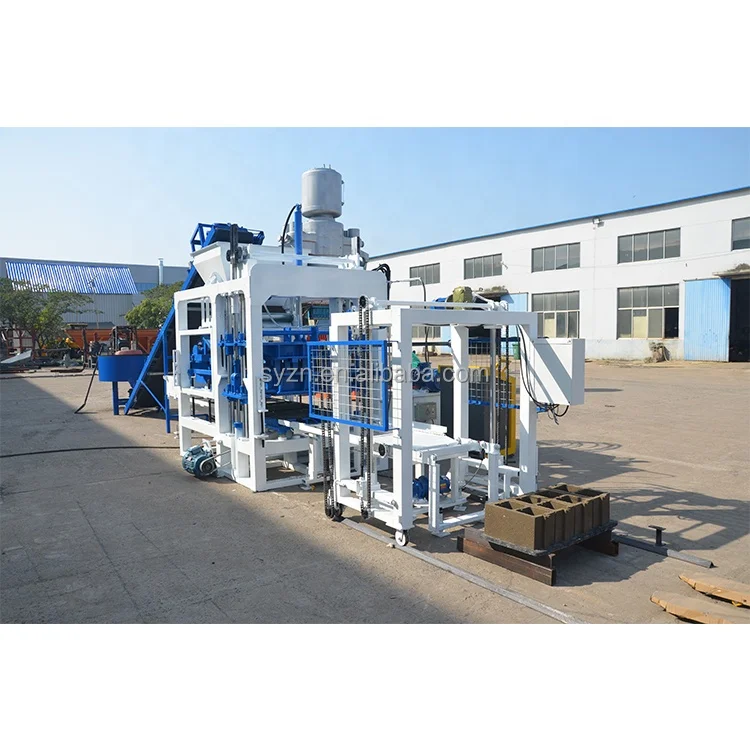
Pallet Feeder & Block Conveyor Specified With The Press — the QT4-18 quotation includes pallet feeding, block conveying and sweeping so downstream stations keep pace with the 15-25 second moulding cycle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 3900×1600×2300 mm |
| Total Weight | 3T |
| Rated Power | 24KW |
| Vibration Force | 40-50KN |
| Moulding Cycle | 15-25s (basis not stated in source) |
| Pallet Size | 850×550×25mm |
| Mixer Model | JQ350 |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Control System | PLC control system |
| Hydraulic Station | Included |
| Output Capacity (Hollow block 400×200×200mm) | 1200-1680 pcs/hr (basis: 400×200×200mm hollow block) |
| Output Capacity (Hollow block 400×150×200mm) | 1800-2400 pcs/hr (basis: 400×150×200mm hollow block) |
| Output Capacity (Solid brick 240×115×53mm) | 3240 pcs/hr (basis: 240×115×53mm solid brick) |
| Automation Level | Semi-automatic |
| Supporting Block Machine Equipment | Pallet feeder, brick conveyor, block sweeper included |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production plant | Crushed stone, sand and cement mix forming 400×200×200mm or 400×150×200mm blocks |
| Solid brick manufacturing | Cement and fine aggregate producing 240×115×53mm bricks |
| Paver and curbstone site production | Fly ash and dust blend for interlocking pavers and kerbstones |
| Contractor housing project plant | On-site block making using locally sourced sand and crushed stone |
What "Rated Output" Really Means When the Line Is Incomplete
A block press rated at 1200 pieces per hour means nothing if the pallet feeder cannot keep up and finished blocks pile up at the press table.
The most common complaint I hear on site is that the block production line equipment could not reach its quoted cycles because something upstream or downstream was choking the flow. A press sitting idle while an operator manually places pallets or clears finished blocks is a press running at half its capability [NEED_CITE: common causes of block line throughput shortfall]. The QT4-18 quotation addresses this by including the pallet feeder, brick conveyor and block sweeper as standard stations within the block production line equipment scope, so each station’s cycle time is matched to the moulding window before the machine leaves the factory.
Matching Pallet Feed to the 15-25 Second Moulding Window
The pallet feeder in this supporting block machine equipment package is timed to deliver an 850×550×25mm pallet to the press within the moulding cycle. When pallet delivery lags behind the press cycle, every missed beat accumulates across a shift. I have seen semi-automatic lines where the operator was the bottleneck simply because pallets were not arriving on time. Specifying the feeder alongside the press removes that variable before installation begins.
Clearing Finished Blocks Before the Next Cycle Starts
The brick conveyor and block sweeper work together to remove finished blocks from the press area within the cycle window. If blocks remain on the pallet at the press table when the next cycle begins, the operator must intervene manually and the entire sequence stalls [NEED_CITE: block line cycle synchronization requirements]. Including these stations in the supporting block machine equipment quotation means the line is planned as one connected system, not a press with afterthoughts.
Reading the Specs That Actually Determine Daily Throughput
The QT4-18 delivers a vibration force of 40-50KN through its hydraulic station, which together with the mould design determines block density and strength. The pallet size of 850×550×25mm dictates how many blocks are formed per cycle and whether that pallet fits the curing racks and forklift already on site. The 24KW rated power must be confirmed against the buyer’s local voltage and frequency before production starts, because a machine wired for the wrong supply will not run at all on arrival. Output capacity figures are tied to specific block formats: 1200-1680 pcs/hr based on a 400×200×200mm hollow block, and 3240 pcs/hr based on a 240×115×53mm solid brick, so daily planning must reference the format being produced.
The Cost of Specifying the Press Alone
When pallet handling and block removal are left for the buyer to source separately, the result is usually a line that cannot match the press’s rated cycle time. Buyers end up paying for a machine whose capability they cannot access because the supporting stations were never engineered to work together [NEED_CITE: hidden costs of incomplete block line specifications]. The press sits idle, the operator works overtime clearing blocks by hand, and the project schedule slips while the buyer tries to retrofit conveyors and feeders that were never part of the original plan.
Why Source the Line as One Package
Block machinery is our single focus, so the QT4-18 press, pallet feeder, conveyor and sweeper are specified as one matched system rather than assembled from separate suppliers after the quotation is signed. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. We provide a line layout drawing showing station positions and the pallet return path so the buyer can confirm the press will not be left waiting between stations. Pallet size and material are confirmed against the buyer’s curing area and forklift before production begins. Voltage, frequency and PLC display language are locked in before the machine enters production so commissioning is not delayed after arrival.
Documentation & Verification
- Line layout showing QT4-18 station positions and pallet return path
- Capacity calculation stated per block format produced on your line
- Pallet specification confirming 850×550×25mm against your curing racks
- Voltage and PLC language confirmation recorded before production
- Factory test record on your target block format before dispatch
- Operation and maintenance manual with wear parts list included
Installation, Commissioning & Support
- Foundation plan matching the 3900×1600mm QT4-18 footprint prepared before arrival
- 24KW power supply with dedicated circuit confirmed to local voltage and frequency
- Machine shipped dismantled with reassembly guidance provided on site
- PLC parameters set to your block format during commissioning
- Operator training on pallet feeder timing and mould change procedure
- Hydraulic wear parts and mould list supplied with first shipment
Before You Request a Quote
To spec the QT4-18 as a complete block production line equipment package, we need your target block formats and daily output target so we can calculate station cycle times. Share your curing area dimensions and forklift capacity so we can confirm pallet compatibility, along with your local voltage and frequency. Tell us about any existing mixers or conveyors you plan to keep so the supporting block machine equipment connects to your current setup without modification.
Frequently Asked Questions
Q: What stations are included in the QT4-18 line quotation and which are left for the buyer to source separately?
A: The quotation covers the QT4-18 press, hydraulic station, PLC control, pallet feeder, brick conveyor and block sweeper. The JQ350 mixer and raw material feeding system are also available as part of the line. Curing racks, forklifts and site civil works are buyer-scope. We provide a line layout drawing so you can see exactly where each station sits before ordering.
Q: How does pallet size 850×550×25mm align with my existing curing racks and forklift?
A: We confirm pallet dimensions against your curing rack spacing and forklift tine width before production starts. If your existing racks do not accommodate 850×550×25mm pallets, we adjust the specification so the pallet feeder delivers a size that fits your current curing area without requiring new infrastructure.
Q: What is the realistic daily output when producing a mix of hollow block and solid brick across one shift?
A: Daily output depends on the ratio of formats in your production plan. The QT4-18 produces 1200-1680 hollow blocks per hour based on 400×200×200mm format and 3240 solid bricks per hour based on 240×115×53mm format. We provide a capacity calculation showing realistic output for your specific format mix across an eight-hour shift.
Q: How are the conveyor speed and pallet feeder cycle matched to the moulding cycle so the press does not idle?
A: The PLC control system coordinates the pallet feeder delivery and brick conveyor removal with the 15-25 second moulding cycle. Each station is tested together at the factory to confirm synchronization on your target block format before dispatch, so the press runs continuously without manual intervention between cycles.
Q: What line layout documentation is provided before shipment so foundation work can be prepared?
A: You receive a line layout drawing showing QT4-18 station positions, conveyor length, pallet return path and utility connection points. This allows your contractor to prepare foundations, power supply and drainage before the machine arrives, reducing the time between delivery and first production run.



