
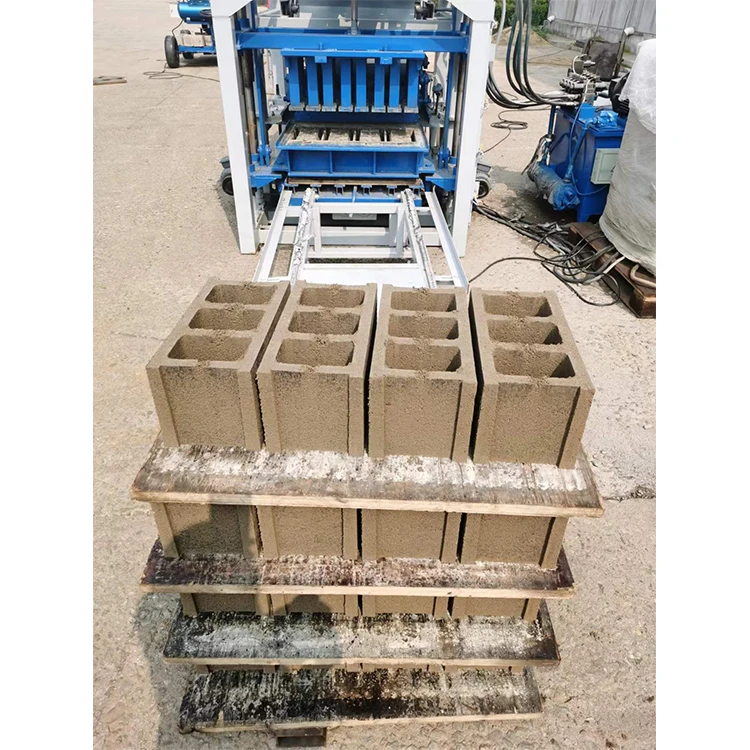
Line-Level Coordination — The QT4-15A is quoted as a complete production line, not a standalone press, so raw material feed, pallet handling, and block conveying are matched to the press cycle from day one.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Molding Cycle | 15-25s (basis not stated in source) |
| Vibration Frequency | 4600 r/min |
| Vibration Force (Exciting Power) | 40-50 kN |
| Total Power | 18.45 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Total Weight | 3 T |
| Control System | PLC control system |
| Hydraulic Station | Included |
| Applied Products | Paver, solid block, hollow block, curbstone (via mould change) |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output Capacity — Hollow Block 400×200×200 mm | 4 pcs/mould, 408 pcs/hr, 3264 pcs/8hr |
| Output Capacity — Hollow Block 400×150×200 mm | 5 pcs/mould, 510 pcs/hr, 4080 pcs/8hr |
| Output Capacity — Solid Brick 240×115×53 mm | 18 pcs/mould, 2100 pcs/hr, 17000 pcs/8hr |
| Included Auxiliary Equipment | Pallet feeder, brick conveyor, block sweeper, manual hydraulic trolley |
| Automation Level | Automatic (PLC-controlled with pallet feeder and conveyor) |
| Stacking Method | (basis to be confirmed) |
| Mould Change Time | (basis to be confirmed) |
| Voltage & Frequency | (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow Block Production | Fly ash, crushed stone, sand, cement (400×200×200 mm or 400×150×200 mm formats) |
| Solid Brick Manufacturing | Sand, cement, dust, crushed stone (240×115×53 mm standard brick format) |
| Paver and Kerbstone Production | High-strength concrete mixes with specific aggregate gradations (via mould change) |
| On-site Construction Supply | Local river sand and crushed stone for project-specific block formats |
| Building Material Distribution | Multi-format output for regional distributors requiring diverse inventory |
Why "3264 Blocks per Shift" Means Nothing Without the Line Layout
The automatic hydraulic block making machine production line capacity figure only holds when the mixer output, pallet feed rate, and conveyor speed are synchronized to the press cycle.
I once worked with a plant that bought a block press based on a catalogue number, only to find their manual pallet handling could not keep up with the machine speed. The press spent half its time waiting for an operator to slide the next pallet into place. The quoted shift output was technically possible, but physically unreachable without the supporting stations. This is why the QT4-15A is specified with the JQ350 mixer, pallet feeder, brick conveyor, and block sweeper as a single matched set — so the cycle time on paper translates to actual blocks on the curing rack [NEED_CITE: industrial equipment line synchronization principles].
How Supporting Stations Prevent Press Starvation
The JQ350 mixer is included in this automatic hydraulic block making machine production line so raw material delivery matches the press demand. When the mixer capacity is undersized relative to the press cycle, the hopper runs dry mid-stroke and the vibration force produces under-compacted blocks. The pallet feeder removes the operator from the feed position, letting the PLC system trigger each cycle without manual timing variation. The brick conveyor then carries finished blocks away at a rate matched to the molding speed, preventing a bottleneck at the press exit.
Pallet Size and Curing Area Compatibility
The 850×550×25 mm pallet specification must align with your existing curing rack dimensions and forklift capacity before the line ships. A pallet that is too wide for your rack spacing means blocks must be restacked by hand after production — negating the efficiency the conveyor was supposed to deliver. Similarly, if your forklift forks are narrower than the pallet width, you cannot transport loaded pallets to the curing yard without a secondary handling step. We confirm pallet dimensions against your site layout so the automatic hydraulic block making machine production line integrates with what you already have on the floor [NEED_CITE: material handling equipment compatibility standards].
Vibration Force and Hydraulic Pressure in Block Density
The 40-50 kN vibration force and hydraulic station work together to compact the mix into a dense, consistent block. Vibration alone settles the aggregate, but without sufficient hydraulic pressure applied simultaneously, the cement paste does not fully bond around the stone particles. The 4600 r/min vibration frequency is tuned for the typical aggregate sizes used in hollow block and solid brick production. When a buyer switches to a finer fly ash mix without adjusting the pressure and vibration duration, block strength drops noticeably. The PLC control system allows these parameters to be stored per mould format so operators do not need to re-tune the press for every product change.
What Happens When the Mixer Is Left Out of the Quote
A buyer who sources the press and mixer from separate suppliers often discovers the mixer discharge rate does not match the press hopper intake geometry. Material spills onto the floor, the hopper starves intermittently, and the operator adds a manual shoveling step that was never in the production plan. Over a shift, this adds up to lost cycles and inconsistent block weight. The QT4-15A line includes the JQ350 mixer so the discharge height, volume per batch, and timing are coordinated with the press feed from the initial layout — not improvised after delivery [NEED_CITE: concrete batching equipment integration].
Why We Spec the Line, Not Just the Press
The QT4-15A is configured against your actual block format, local aggregate type, and target daily output rather than pulled from a default catalogue page. The supporting equipment — pallet feeder, brick conveyor, block sweeper, manual hydraulic trolley — is included in the quotation so there are no surprise line items after you sign. The pallet size is checked against your curing rack and forklift before production begins. The PLC display language and electrical voltage are confirmed to match your site, not assumed. Installation includes operator training on the full line, not just the press controls, so your team understands how each station affects the next.
Documentation & Verification
- Line layout drawing showing station spacing and material flow path for the QT4-15A configuration
- Capacity calculation sheet stating the block format and cycle time assumed for each output figure
- Pallet specification matched to your curing rack dimensions and forklift fork width
- Hydraulic and electrical schematic covering the press, mixer, pallet feeder, and conveyor circuits
- Factory test record showing the QT4-15A running with your specified mould before dispatch
- Voltage, frequency, and PLC display language confirmation document signed before production
Installation, Commissioning & Support
- Foundation plan based on the 7100×1600 mm footprint and 3 T total weight of the QT4-15A
- Electrical connection requirements for the 18.45 kW total power draw with dedicated circuit specifications
- Assembly sequence for the press, JQ350 mixer, pallet feeder, and brick conveyor on your floor
- First-run commissioning with mould installed and PLC parameters tuned to your mix design
- Operator training covering the full line from mixer loading through conveyor discharge
- Wear parts list including hydraulic seals, vibration motor bearings, and mould liner components
What We Need to Size Your Line
To configure the QT4-15A for your plant, we need the block formats your market sells, the daily output target per format, and the raw materials available locally — particularly whether you will use fly ash, river sand, or crushed stone. We also need your existing curing rack dimensions, forklift specifications, and the voltage and frequency at your site. If you have upstream or downstream equipment already in place, share the make and model so we can confirm interface compatibility.
Frequently Asked Questions
Q: How is the line capacity calculated for each block format?
A: Each output figure — such as 3264 hollow blocks per 8-hour shift for the 400×200×200 mm format — is based on a specific mould cavity count and an assumed cycle time within the 15-25 second range. The actual cycle depends on your mix design and target block strength, which we confirm during commissioning.
Q: Which supporting stations are included and which do I need to supply?
A: The quotation covers the QT4-15A press, JQ350 mixer, pallet feeder, brick conveyor, block sweeper, and manual hydraulic trolley. Curing racks, forklifts, and the stacking method beyond the conveyor discharge are typically buyer-supplied unless specified otherwise.
Q: How does pallet size affect my curing rack and forklift setup?
A: The 850×550×25 mm pallet must fit your curing rack spacing and be liftable by your forklift. If your existing racks or forklift do not match, blocks must be re-handled after production. We verify these dimensions against your site equipment before the line ships.
Q: Does the JQ350 mixer feed rate match the press cycle?
A: The JQ350 is sized so one batch supplies enough material for multiple press cycles without the hopper running dry. The exact batch timing is tuned during commissioning based on your specific mix and the block format being produced.
Q: How are voltage, frequency, and PLC language confirmed before shipment?
A: We request your site electrical specifications and preferred control language during the quotation stage. A confirmation document is signed before production begins, so the QT4-15A arrives with the correct motor windings and PLC display already configured for your operators.



