
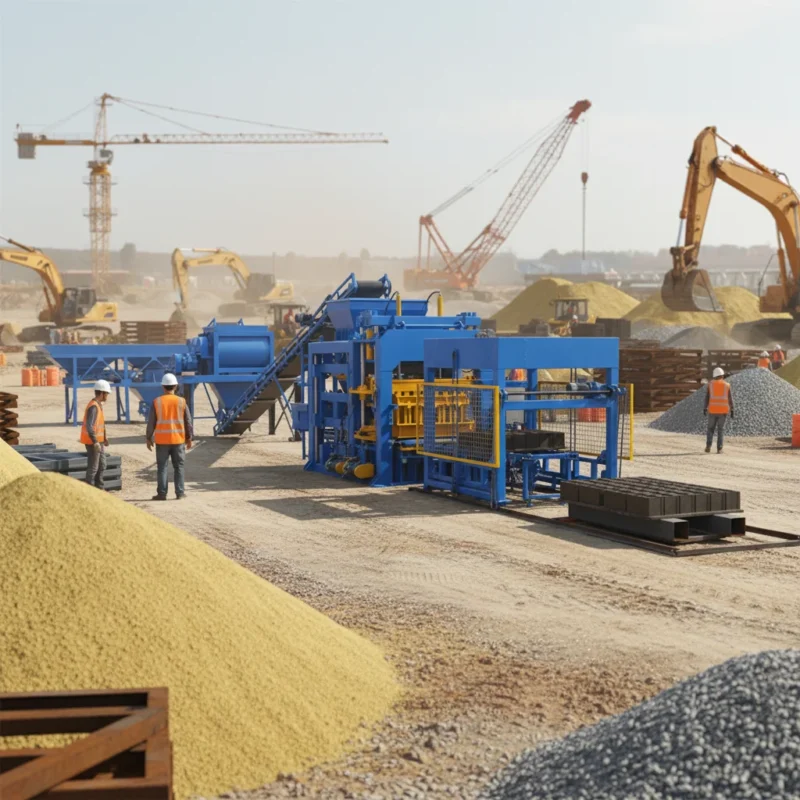
Matched Line Configuration — Every upstream feeder, mixer, and downstream stacker is calculated against the QT12-15 press cycle so no station sits idle during a shift.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT12-15 |
| Product Type | Hydraulic Block Making Machine |
| Total Power | 62 kW |
| Pallet Size | 1300 × 900 mm |
| Moulding Cycle | 15–30 seconds (basis not stated in source — confirm block format / material / thickness) |
| Vibration Type | Table vibration |
| Vibration Force | 120 kN |
| Voltage | Customized according to local industrial voltage (basis not stated in source — confirm voltage / frequency / phase) |
| Moulds | Customized according to target block format |
| Key Features | CE declaration where applicable, hydraulic press with four-axis table vibration, frequency conversion drive |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial walls | Crushed stone, sand, cement, fly ash aggregates |
| Solid block manufacturing for load-bearing structures | Dense aggregate blends with standard cement ratios |
| Paving block and interlocking brick for roads and walkways | High-strength mix designs with fine aggregate grading |
| Kerbstone and slope protection brick for infrastructure | Coarse aggregate with reinforced vibration compaction |
| Porous brick for permeable surface applications | Open-graded aggregate with controlled cement content |
| On-site production by construction contractors | Locally sourced raw materials matched to project specs |
What "Cycles per Hour" Leaves Out in a Hydraulic Block Making Machine Production Line
A press rating means nothing when the mixer cannot feed fast enough or the pallet return loop cannot keep up.
I spent years on workshop floors in Linyi watching lines stall. A Middle East buyer once installed a high-capacity press nearly identical to this class, but the batching station could not discharge a full charge within the press cycle. The main unit waited empty for several seconds every round, and by end of shift the actual output sat well below the quoted figure. Nobody had calculated the upstream and downstream timing before the order was placed [NEED_CITE: block production line cycle matching standards]. That loss repeats across dozens of plants I have walked through — the press is blamed, but the real failure lives in the stations nobody specified.
Station-to-Station Timing Across the Block Line
The QT12-15 press completes a moulding cycle in 15 to 30 seconds depending on the block format and mix, which means the raw material feeder must deliver a measured charge to the mixer, the mixer must discharge into the distributor hopper, and the pallet feeder must slide a fresh board under the mould — all within that same window. If any single station runs slow, the hydraulic block making machine production line loses that cycle entirely. We map every station interval against the press cycle during the proposal stage so the buyer sees where the constraint sits before metal is cut.
Pallet Return, Stacking, and Curing Rack Flow
Downstream timing matters just as much. Once the press ejects a loaded pallet, the wet block must travel to the curing racks without jolting, and the empty pallet must loop back to the feeder before the next cycle opens. A 1300 × 900 mm pallet determines the rack spacing, the forklift tine width, and the curing yard layout. When the pallet return conveyor or the stacker cannot clear the board in time, the press holds at top-dead-center and the whole hydraulic block making machine production line drifts below its rated tempo [NEED_CITE: pallet handling and curing logistics in concrete block plants].
Reading the Numbers That Actually Govern Output
The 120 kN table vibration force works with hydraulic pressure to compact the aggregate into a dense, consistent block. Four-axis frequency conversion keeps the vibration uniform across the full 1300 × 900 mm pallet area, which matters when a single board carries multiple hollow blocks or a full field of pavers. The 62 kW total power rating covers the press motor, hydraulic pump, and vibration drive combined — buyers need to confirm their site transformer can carry that load alongside the mixer, conveyor, and stacking motors before the line ships. Voltage and frequency must be locked in during the order stage because rewiring a control cabinet on arrival delays commissioning by weeks. Replaceable wear plates on the cloth platform cut maintenance windows down to a shift instead of a full day, keeping the line running through scheduled service intervals.
The Cost of Skipping Line Integration
Plants that buy the press alone and bolt on mismatched feeders and stackers later end up with a bottleneck that shifts position every month. First the mixer starves the hopper, then the pallet feeder jams, then the curing rack overflows because the stacker cannot cube fast enough. Each fix costs a downtime window, a fabrication bill, and lost production days that the buyer did not budget for [NEED_CITE: hidden costs of uncoordinated block line equipment]. A fully specified line quotation that names every station, its cycle time, and its interface point removes that risk before the first container is loaded.
Why Source the Full Line from One Integration Point
Block machinery is the single focus here, so the press, mould, pallet, feeder, mixer, stacker, and curing rack handler are specified as one matched system rather than assembled from separate vendors. The configuration is set against the buyer’s actual mix design, local aggregate, and target block format — not pulled from a catalogue default. Mould design covers the formats the buyer’s market actually sells, including custom drawings when a project calls for a non-standard kerbstone or interlocking profile. The automation level is selectable, meaning a buyer can start with semi-automatic pallet handling and add a full stacker and cubing station later without replacing the press. Factory testing runs the entire line under load before dispatch, catching timing mismatches that would otherwise surface on the buyer’s floor.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format
- Machine specification sheet covering press, feeder, mixer, and stacker ratings
- Mould drawing and format list for every block profile in the order
- Pallet specification matched to curing rack dimensions and forklift capacity
- Hydraulic and electrical schematic for site utility integration
- Voltage, frequency, and PLC display language confirmation record
Installation, Commissioning & Support
- Foundation plan sized to the QT12-15 press footprint and vibration load
- Dedicated 62 kW circuit with confirmed voltage and frequency before energizing
- Press, mixer, and conveyor arrive dismantled with labeled reassembly points
- First-run cycle test across every station with operator present at each position
- Operator training covers mould change procedure, wear plate replacement, and daily greasing
- Wear parts and mould list provided with reorder part numbers for local stocking
Before You Send the Inquiry
A complete line proposal starts with the block formats you intend to sell, the daily output you need per format, and the raw materials available within hauling distance of your site. Share your curing yard dimensions and the forklift model already on the floor so the pallet size and rack spacing align with what you have. Confirm your local industrial voltage, frequency, and the control language your operators will read — these three details decide whether the line runs on day one or sits waiting for an electrician.
Frequently Asked Questions
Q: How is line capacity calculated and which block format is assumed?
A: The moulding cycle of 15 to 30 seconds varies by block format, wall thickness, and aggregate density. We state capacity per format in the proposal — a hollow block cycle differs from a paver cycle — so the buyer sees realistic daily output for each product, not a single inflated number.
Q: How must the mixer and pallet feeder match the press cycle?
A: The mixer must discharge a full batch into the distributor hopper and the pallet feeder must deliver a fresh board within the press cycle window. We calculate each station interval and specify conveyor speeds so the QT12-15 never waits on upstream or downstream equipment.
Q: What supporting equipment is included in the line quotation?
A: The quotation covers raw material feeding, mixing, pallet feeding, stacking, and curing rack handling as named line items. Each station carries its own cycle time and interface specification so nothing is left to the buyer to source separately after arrival.
Q: How is voltage and control language confirmed before shipment?
A: We collect the buyer’s local voltage, frequency, and phase during the proposal stage and record the PLC display language before production starts. This prevents commissioning delays caused by incompatible electrical supply or unreadable control screens on site.



