
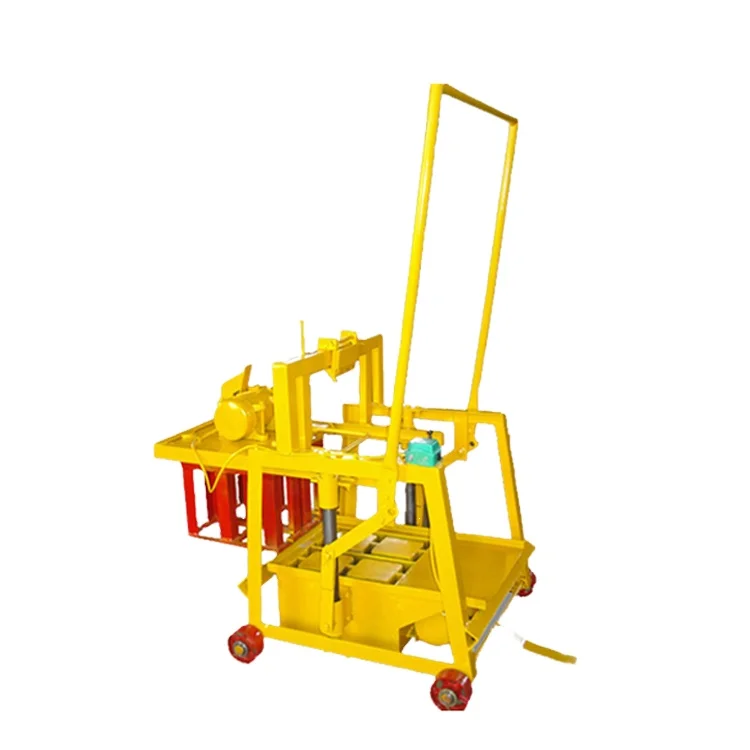
Matched System Design — every station around the QMJ2-45 is specified together so the press never waits on upstream mixing or downstream curing.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMJ2-45 |
| Product Type | Mobile Egg-Laying Block Making Machine |
| Rated Power | 1.5 kW |
| Voltage & Frequency | Configurable to buyer’s local standard (basis not stated in source) |
| Control System | Semi-automatic operation |
| Overall Dimensions (L×W×H) | 920 × 800 × 1258 mm |
| Net Weight | 150 kg |
| Standard Mould Format | 300 × 150 × 100 mm |
| Pieces per Mould | 2 |
| Cycle Time | 45 s |
| Output Capacity | 160 pcs/h (based on 300 × 150 × 100 mm solid block) |
| Daily Output | 1,280 pcs/8 hours (based on 300 × 150 × 100 mm solid block) |
| Vibration System | Bed mould vertical vibration + upper mould compression vibration, 2 vibrators per mould |
| Raw Material | Concrete, sand, cement |
| Assembly State | Mobile / egg-laying |
| Automation Level | Semi-automatic |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site block production for construction contractors | Solid concrete blocks from local sand and cement without fixed plant infrastructure |
| First block plant for entrepreneurs | 300 × 150 × 100 mm solid blocks with room to expand the line as demand grows |
| Local production for housing project contractors | Concrete blocks produced directly at the development site using locally sourced aggregate |
| Small-plant supply for building material distributors | Entry-level mobile egg-laying output for markets favouring hand-loaded operations |
Why the Line Around the Press Matters More Than the Press Itself
A mobile block making machine production line is only as fast as its slowest supporting station.
I have watched a contractor in West Africa lose an entire shift of output because the mixer could not feed the press fast enough. The QMJ2-45 finished its 45-second cycle and then sat idle while the operator shoveled concrete into the hopper by hand. The machine was rated for a specific output based on a 300 × 150 × 100 mm solid block, but the real daily number fell well short because nobody had matched the upstream mixing capacity to the press cycle. [NEED_CITE: typical mixer-to-press cycle matching in small-scale block plants]
Mapping Every Station From Raw Feed to Cured Block
The QMJ2-45 sits at the centre of a small-scale mobile block making machine production line that starts with raw material proportioning and ends with on-ground curing. A pan mixer or drum mixer feeds the press hopper, and its batch size must deliver enough concrete to fill the mould before the 45-second cycle completes. If the mixer takes longer than the press cycle to prepare the next batch, the operator is standing still and the daily count drops.
Synchronising Egg-Laying Pace With Curing Space
Once the QMJ2-45 lays a block on the ground, that block needs flat, level curing space nearby. The machine moves forward after each cycle, so the operator must plan a linear path that allows freshly laid blocks to cure undisturbed. [NEED_CITE: curing time and space requirements for concrete blocks in tropical climates] If the curing area runs out before the shift ends, the press stops regardless of how much concrete the mixer can supply.
Reading the Specs That Actually Affect Your Site
The dual vibration system — bed mould vertical vibration paired with upper mould compression vibration — compacts the concrete mix from both directions during the 45-second cycle. This matters on a construction site where the aggregate grading varies from one truckload to the next; consistent vibration keeps block density within tolerance even when the sand is slightly coarser than the previous batch. The 1.5 kW rated power means the machine can run from a small diesel generator, which is often the only power source available on a greenfield housing project. The compact 920 × 800 × 1258 mm footprint and 150 kg net weight allow two workers to relocate the press by hand when the work front moves to the next building plot. Semi-automatic control keeps the operator in the loop for mould filling and egg-laying, which suits sites where a full PLC cabinet would be exposed to rain and dust.
What Happens When Line Stations Are Chosen Separately
I once visited a site where the buyer had sourced a mixer from one supplier and the egg-laying press from another. The mixer discharged into a wheelbarrow, and the wheelbarrow was tipped into the press hopper by hand. Every tip took roughly twenty seconds, which meant the press was idle for almost half of every cycle. The daily output was barely half of what the press could have produced with a matched belt feeder. [NEED_CITE: manual versus assisted feeding impact on daily block output]
The same logic applies downstream. If the curing area is uneven or too far from the laying path, blocks crack during transport or the operator spends more time walking than operating. These losses never show up in a machine spec sheet — they only appear when the line is running on a real site with real workers and real deadlines.
Why Specifying the Whole Line Here Changes the Outcome
Block machinery is our single focus, so the QMJ2-45 is never quoted as a standalone press. The mixer, feeding arrangement, and curing layout are specified as one matched system, which means the cycle times at every station are checked against each other before the quotation is issued. Configuration is set against the buyer’s actual mix design and local aggregate rather than a catalogue default, so the vibration force and cycle time are validated for the sand and cement the buyer can actually source. Mould design covers the formats the buyer’s market sells, including custom drawings when the standard 300 × 150 × 100 mm format does not match local demand. The semi-automatic starting point leaves room to add assisted feeding or pallet handling later, so a first-time entrepreneur can invest in stages. Installation support includes operator training on the full line, not just the press, because a trained operator who understands station timing will protect daily output better than any automation upgrade.
Documentation & Verification
- Line layout drawing showing mixer, QMJ2-45, and curing area with distances and station cycle times stated
- Capacity calculation sheet confirming 160 pcs/h based on 300 × 150 × 100 mm solid block
- Mould drawing and format list so buyers verify the block their market actually sells
- Voltage and frequency confirmation document signed before production begins
- Factory test record run on the buyer’s target block format before dispatch
- Operation and maintenance manual covering both press and supporting mixer
Installation, Commissioning & Support
- Level ground area of approximately 10 m × 5 m required for the QMJ2-45 and adjacent curing space
- Single-phase or three-phase power supply matching confirmed voltage and frequency, with dedicated 1.5 kW circuit
- Machine arrives assembled; only the hopper and handle bar require bolt-on attachment at site
- First-run commissioning includes mixer batch timing adjusted to match the 45-second press cycle
- Operator training covers dual vibration adjustment for local aggregate variations
- Wear parts list provided for mould liners and vibrator mounts with recommended replacement intervals
What to Share Before Requesting a Quotation
Send your target block format and the daily output you need on your construction site or first plant. Confirm the voltage and frequency available at the project location, and describe the sand and cement you plan to use so we can match the mixer and vibration settings. If you already own a mixer or generator, share its model and capacity so we can check whether it keeps pace with the press.
Frequently Asked Questions
Q: How is the QMJ2-45’s daily output calculated, and which block format is assumed?
A: The 1,280 pieces per 8-hour shift is based on a 300 × 150 × 100 mm solid block with 2 pieces per mould and a 45-second cycle. If you switch to a larger hollow block or a different format, the pieces per mould and cycle time change, so the daily output must be recalculated for your specific format before you commit to a production target.
Q: What supporting stations are needed to keep the QMJ2-45 from waiting?
A: At minimum, a mixer sized to deliver a full batch within the 45-second cycle, a flat curing area long enough to hold a full shift’s output, and a feeding arrangement — manual or assisted — that transfers concrete from the mixer to the press hopper without delaying the next cycle.
Q: Can the semi-automatic setup be upgraded with automatic feeding or stacking later?
A: The QMJ2-45 is an egg-laying machine that lays blocks directly on the ground, so automatic pallet stacking does not apply. However, assisted feeding from mixer to hopper can be added to reduce manual handling and protect cycle consistency as your daily volume grows.
Q: How should voltage, frequency, and control language be confirmed before shipment?
A: Provide your site’s exact voltage and frequency — for example 220 V / 50 Hz or 380 V / 60 Hz — before production begins. The control panel labels and any display language are then set at the factory so commissioning is not delayed by rewiring or relabelling after arrival.



