
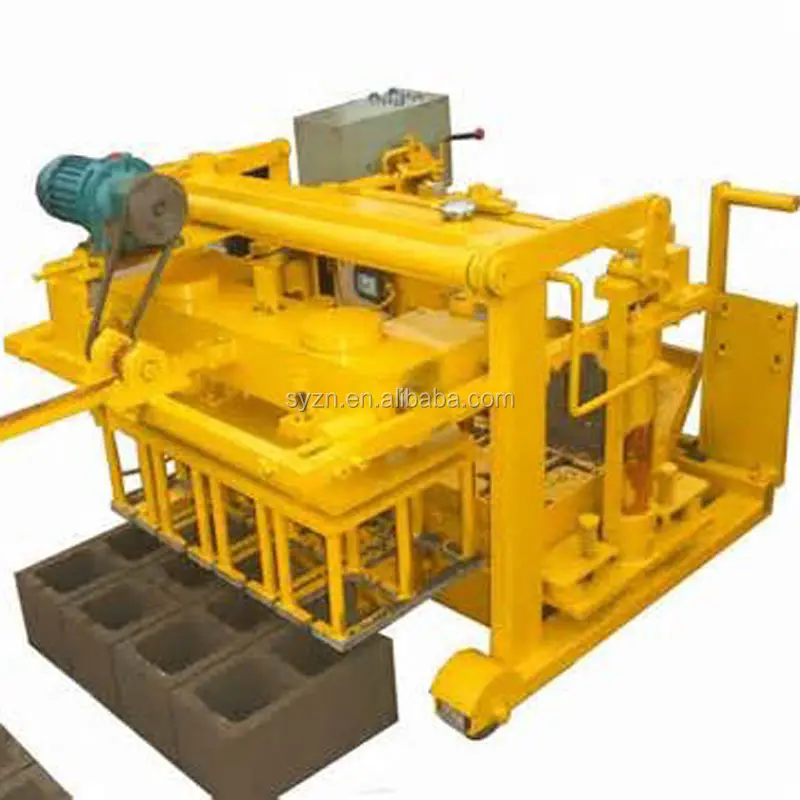
Integrated Line Thinking — the QMY4-30 mobile block machine is specified alongside its feeding, mixing and curing workflow so the press never waits on upstream material or downstream handling.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMY4-30 |
| Product Type | Mobile Egg Laying Concrete Block Making Machine |
| Hydraulic Method | Mould vibration |
| Demold Method | Hydraulic |
| Molding Cycle | 25–30s |
| Total Power | 5.95 kW |
| Pallet Requirement | Pallet-less (egg laying type) |
| Output (400×200×200 mm hollow block) | 480 pcs/hour, 3,840 pcs/8hr (4 pcs/mould) |
| Output (400×150×200 mm block) | 600 pcs/hour, 4,800 pcs/8hr (5 pcs/mould) |
| Output (400×100×200 mm block) | 840 pcs/hour, 6,720 pcs/8hr (7 pcs/mould) |
| Technology Reference | Italian advanced technology origin |
| Operating Environment | Mountainous, hilly, industrial mining, desert and coastal areas |
| Mobility | On-site production without fixed plant |
| Standards | ISO 9001:2000, CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Contractor on-site hollow block production | Cement, crushed stone, sand, and gravel mix for 400×200×200 mm blocks |
| Remote housing project solid block supply | Local aggregate with cement binder for 400×150×200 mm format |
| First-time block entrepreneur | Pallet-less egg laying operation in areas with limited infrastructure |
| Mining or desert construction camp | 400×100×200 mm blocks produced directly on uneven terrain |
| Coastal development projects | Salt-resistant aggregate mixes laid on prepared ground without curing racks |
What "Pallet-Free" Really Means for Your Block Line
Eliminating pallets removes an entire material flow — no pallet purchase, no pallet return conveyor, no curing rack system, no forklift shuttle between press and yard.
Many buyers compare mobile egg laying machines against static presses and miss that the real cost difference sits outside the press itself. Pallets represent a recurring capital item that must match the press cycle, survive outdoor curing, and fit the forklift tines already on site. When a pallet-based line arrives without the handling stations quoted, blocks pile up by hand within the first hour of production [NEED_CITE: common omissions in block line quotations for export markets]. A mobile block machine production line like the QMY4-30 sidesteps this entirely: the mould lowers onto prepared ground, vibration and hydraulic pressure form the block in place, and the machine rolls forward to repeat.
How Egg Laying Changes the Material Flow Around the Press
On a static block plant, the press sits at the center of a loop: pallet feeder, press, block sweeper, elevator, curing rack, lowerator, cuber, and pallet return. The mobile egg laying block machine turnkey concept collapses that loop into a straight path. Raw material arrives from the mixer, the press forms blocks directly on the ground, and the finished product cures in rows where it lands. This means the feeding and mixing station must keep pace with a 25–30 second cycle without the buffer that a pallet magazine normally provides.
The trade-off is space. Egg laying requires a flat, compacted curing yard sized for a full day’s output — roughly the area needed to lay out several thousand blocks in single-file rows. Site preparation shifts from building a curing chamber to grading and compacting an open yard.
Where the Line Bottlenecks First
Feeding the QMY4-30 is not as simple as dumping material into a hopper and walking away. The press cycles every 25–30 seconds, so the mixer must deliver a fresh batch within that window or the operator stands idle. In practice this means a pan mixer or small drum mixer positioned so that wheelbarrow or conveyor delivery keeps the hopper charged [NEED_CITE: continuous feed requirements for mobile block presses]. If the mixer is undersized, the effective daily output drops well below the per-hour figures calculated from a single mould cycle. I have seen sites where the mixer could only supply half the press appetite, cutting real output accordingly.
Mould Vibration, Hydraulic Demold, and What They Mean for Block Density
The QMY4-30 uses mould vibration rather than full hydraulic press force, which changes how mix design interacts with the machine. Vibration consolidates the concrete inside the mould cavity; the hydraulic system then lifts the mould away without disturbing the freshly formed block. If vibration frequency and duration are not matched to the local aggregate’s particle shape and moisture content, the block leaves the mould under-consolidated. I once spent two weeks on site adjusting vibration timing because the local sand carried high clay content, which absorbed water differently and left blocks friable until the parameters were corrected.
The 5.95 kW total power rating reflects this vibration-plus-demold method — it is a modest electrical demand that most temporary site generators can support, provided voltage and frequency match [NEED_CITE: generator sizing for mobile block making equipment]. The trade-off is that mould vibration relies more heavily on consistent mix quality than a high-tonnage hydraulic press would.
When the Wrong Supporting Equipment Stops the Line
Skipping the raw material feed configuration or choosing a mixer that cannot match the 25–30 second cycle turns a mobile advantage into a stationary bottleneck. Similarly, ignoring the ground preparation for egg laying — failing to compact the curing yard or neglecting drainage on a coastal site — leads to blocks settling unevenly during the first hours of cure, producing dimensional variation that no amount of press adjustment can fix [NEED_CITE: ground preparation standards for egg laying block production]. I have also seen buyers discover after arrival that their site voltage does not match the motor specification, delaying commissioning by weeks while transformers are sourced locally.
Why Buyers Place Repeat Orders Here
The QMY4-30 is specified as one matched station within the wider line, not quoted as a standalone press with the assumption that the buyer will figure out feeding, mixing and curing separately. Capacity figures are stated per block format — 400×200×200 mm, 400×150×200 mm, and 400×100×200 mm — so buyers know what to expect before the machine ships rather than discovering the gap after arrival. Mould options cover the formats the buyer’s local market actually sells, with custom drawings available when a project specifies a non-standard size. The automation level remains selectable: a buyer can begin with manual material handling and add conveyor feeding later without replacing the press. Installation support includes operator training on vibration and demold parameter adjustment, which matters especially when local aggregate differs from the test material used at the factory.
Documentation & Verification
- Line layout showing mixer placement relative to the QMY4-30 feed hopper
- Capacity calculation sheet stating assumed block format for each output figure
- Mould drawing and format list confirming available block sizes before production
- Voltage and control language confirmation sheet signed before build
- Factory test record using target mix design where sample material is provided
- Packing photographs and customs documentation support for container loading
Installation, Commissioning & Support
- Compacted, level curing yard sized for daily QMY4-30 output before machine arrival
- Voltage and frequency verified against the 5.95 kW motor rating before connection
- Mixer positioned for continuous feed matching the 25–30 second mould cycle
- Vibration frequency and demold timing calibrated on site with buyer’s actual aggregate
- Operator training covering mould change procedure and format switching
- Wear parts list with reorder references for mould liners and vibration components
What to Send with Your Inquiry
To configure the QMY4-30 and its supporting stations correctly, share the block formats your market requires, the daily output you need per format, and a sample or description of your local sand and aggregate. Include the voltage and frequency available at your project site, and whether you already have a mixer or need one matched to the press cycle. If you are working to a project deadline, state the required arrival date so stock availability and shipping lead time can be confirmed upfront.
Frequently Asked Questions
Q: How is output capacity calculated and which block format does it assume?
A: Each output figure is tied to a specific block size and mould cavity count. The QMY4-30 produces 480 pieces per hour for 400×200×200 mm hollow blocks with 4 cavities per mould, 600 per hour for 400×150×200 mm with 5 cavities, and 840 per hour for 400×100×200 mm with 7 cavities. Daily figures assume an 8-hour shift at continuous cycle.
Q: What raw material feeding and mixing setup keeps the press running?
A: The 25–30 second mould cycle demands a mixer that delivers a fresh batch within that window. A pan mixer or small drum mixer matched to the hopper volume, positioned for short wheelbarrow or conveyor transfer, prevents idle time between cycles and keeps daily output aligned with rated capacity.
Q: What voltage and electrical infrastructure does the project site need?
A: The QMY4-30 draws 5.95 kW total, which most site generators can supply. Voltage and frequency must be confirmed before the machine is built, because motor winding and control components are configured for the destination grid. Mismatched supply delays commissioning until a transformer is sourced locally.
Q: How does pallet-less egg laying affect curing and block handling?
A: Blocks cure in rows on the ground where they are formed, eliminating pallet purchase and curing rack infrastructure. The trade-off is a compacted, level yard large enough for a full day’s output. After initial set, blocks are stacked manually or with equipment for further curing and eventual transport to the construction area.
Q: What mould formats are available and can custom sizes be produced?
A: Standard moulds cover 400×200×200 mm hollow, 400×150×200 mm, and 400×100×200 mm solid formats. Custom moulds can be designed to buyer drawings when a project specifies a non-standard block size. Mould drawings and a format list are confirmed before production begins.


