
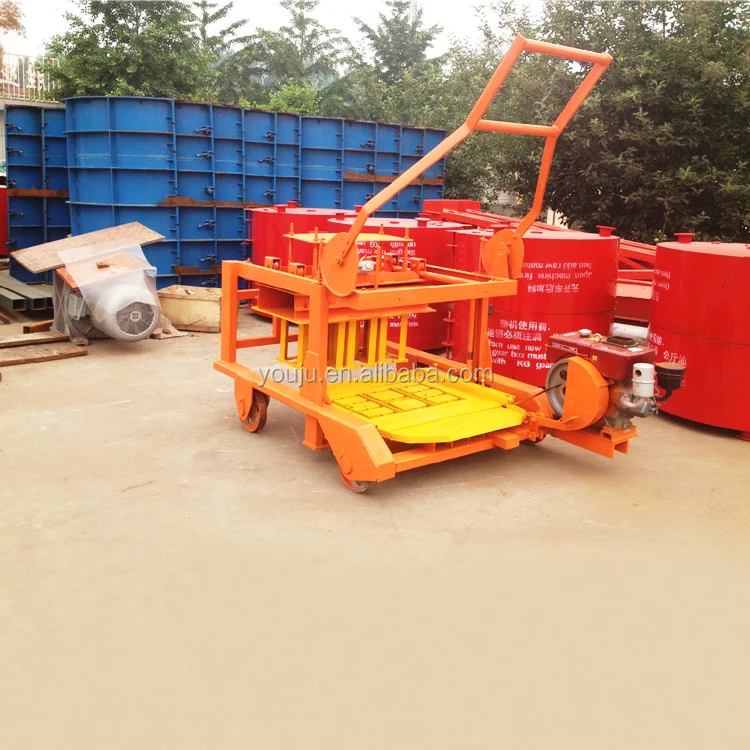
Matched Line Rhythm — we size the mixer, material feed and block handling around the QMR4-45’s 40–45s cycle so the press is never starved of material or left stacking by hand.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMR4-45 |
| Product Type | Mobile Egg Laying Block Making Machine |
| Overall Dimensions (L×W×H) | 2420 × 1320 × 1650 mm |
| Net Weight | 810 kg |
| Moulding Cycle | 40–45 s |
| Pallet Size | No pallet required |
| Rated Power | 6 kW |
| Diesel Engine Option | 6 kW or 6–8 HP |
| Voltage | 220 V / 380 V or site-specific |
| Output Capacity | 3000 pcs/day based on 400×200×200 mm hollow block, 4 pcs/mould |
| Output Capacity | 3500 pcs/day based on 400×150×200 mm hollow block, 5 pcs/mould |
| Output Capacity | 4500 pcs/day based on 400×120×200 mm hollow block, 6 pcs/mould |
| Mould Formats Included | 400×200×200 / 400×150×200 / 400×120×200 mm hollow block |
| Automation Level | Manual egg-laying operation |
| Power Source | Diesel engine or electric motor |
| Assembly State | Fully assembled at factory |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production at building sites | Cement, sand, crushed stone — no fixed plant required |
| Remote housing project block supply | Diesel-powered operation where grid electricity is unavailable |
| Small-scale contractor block making | Hollow formats from 400×200×200 mm down to 400×120×200 mm |
| Entrepreneur first-plant setup | No pallet investment, no curing rack infrastructure |
What the Mixer Must Deliver Before the Press Can Lay
A mobile block making machine production line only produces as fast as its slowest station feeds it.
I once watched a QMR4-45 sit idle for two full minutes every cycle because the site mixer discharged half a batch at a time. The machine itself was ready — the operator was ready — but the material simply was not there. That idle time does not show up in any brochure figure, yet it cuts real daily output roughly in half. When we quote a mobile block making machine production line around this egg-layer, the mixer capacity, conveyor feed rate and discharge sequence are calculated against the 40–45 s moulding cycle, not against a generic daily target. [NEED_CITE: matching mixer output to block press cycle time]
How the Egg-Laying Sequence Eliminates Pallet Infrastructure
The QMR4-45 places each set of blocks directly on the ground and moves forward one mould length before the next cycle begins. This removes pallet purchasing, pallet storage space, pallet handling labour and an entire curing-rack system from the project cost. For a contractor working on an unfinished site with no forklift and no covered curing area, the machine’s footprint plus the open ground behind it is the entire production zone.
Where Line Synchronization Determines Actual Output
Every station upstream of the press — aggregate batching, cement weighing, mixing, discharge — must complete its task within the 40–45 s window the QMR4-45 needs to vibrate, lift and advance. If the mixer takes 90 s per batch, the press waits through almost half of each cycle. We specify the supporting equipment with this timing in mind, so the mobile block making machine production line runs continuously rather than in a start-stop pattern that inflates labour cost per block. [NEED_CITE: production line synchronization standards for mobile block plants]
Reading the Specs That Actually Matter on Site
The 6 kW rated power must cover both vibration and hydraulic lift simultaneously; undersizing the diesel engine leads to weak compaction and blocks that crumble before curing. Mould formats span three hollow sizes on one frame, yet swapping a mould still takes manual effort — plan changeovers at shift breaks to protect continuous run time. The 810 kg net weight keeps the machine portable, but it also means the ground surface must be reasonably level; soft or freshly backfilled soil causes the blocks to tilt as they are laid, introducing dimensional variance the mason will notice.
What Happens When Line Stations Are Mismatched
A mixer that is too small forces the operator to run two batches before one mould can fill, doubling the effective cycle time without any change to the press itself. Conversely, an oversized mixer discharges more material than the hopper can accept, leaving wet concrete standing in the trough where it begins to set. Both scenarios are common on sites where each piece of equipment was bought separately, and both erase the daily output the buyer based their project schedule on. [NEED_CITE: consequences of unmatched batch sizing in small block lines]
Why Procurement Through a Line Supplier Changes the Outcome
Block machinery is the single focus here, so the QMR4-45, its moulds and the supporting mixer are specified as one matched system rather than assembled from separate vendors. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Mould design covers the hollow formats the local market moves, and custom drawings are available when a project calls for a non-standard size. Automation level is selectable, allowing a buyer to start with manual egg-laying and add feeder upgrades later. Installation support includes operator training so the crew understands cycle timing from day one. [NEED_CITE: integrated line specification versus separate equipment sourcing]
Documentation & Verification
- Line layout drawing showing mixer discharge matched to QMR4-45 cycle
- Capacity calculation per hollow block format with stated assumptions
- Diesel and electric power options with voltage confirmation sheet
- Mould drawing and format list for all quoted hollow sizes
- Factory test record before dispatch with cycle timing logged
Installation, Commissioning & Support
- Level, compacted ground required across the machine travel path
- 220 V or 380 V supply confirmed before electric motor dispatch
- Machine arrives fully assembled — no on-site mechanical build
- First-run cycle timing set against the installed mixer output
- Mould change and vibration adjustment covered in operator training
- Wear parts list for vibration springs and mould liners provided
Preparing a Line Inquiry
To size a mobile block making machine production line correctly, share the target block format, the daily volume your project schedule demands, and the raw materials you can source locally. Let us know whether grid power is reliable at the site or if a diesel configuration is preferred, and confirm the local voltage and frequency so the motor or engine match is right before packing.
Frequently Asked Questions
Q: How is daily output calculated, and which block format does the 3000 pcs/day figure assume?
A: The 3000 pcs/day figure is based on 400×200×200 mm hollow blocks with four pieces per mould and a 40–45 s cycle. Switching to a smaller format such as the 400×120×200 mm block raises the per-mould count to six and the stated daily figure to 4500 pcs. Real output depends on mixer feed rate and operator pace.
Q: What supporting equipment does the line include beyond the press?
A: We specify the pan mixer, aggregate batch hopper and manual or belt-fed material conveyor to match the QMR4-45 cycle. Pallet systems and curing racks are not needed because the machine lays blocks directly on the ground. The exact station list depends on the automation level the buyer selects.
Q: How do mixer capacity and feed rate match the QMR4-45 cycle time?
A: The mixer must discharge one full mould load of concrete within the 40–45 s window. We calculate the batch volume against the hopper capacity and select a pan mixer whose discharge gate opens fast enough to keep the press running without idle cycles.
Q: What site preparation is needed for an egg-laying machine with no pallets?
A: The ground must be compacted and reasonably level across the full travel path. No concrete floor, curing rack or covered yard is required. The machine’s 810 kg weight means very soft or freshly backfilled soil should be compacted first to prevent block tilting during laying.
Q: Can the diesel engine be swapped for an electric motor before dispatch?
A: Yes. The QMR4-45 is available with a 6 kW diesel engine or an electric motor rated for 220 V or 380 V. Confirm the site voltage and frequency during inquiry so the correct motor is fitted and the control panel labels match the destination standard.



