
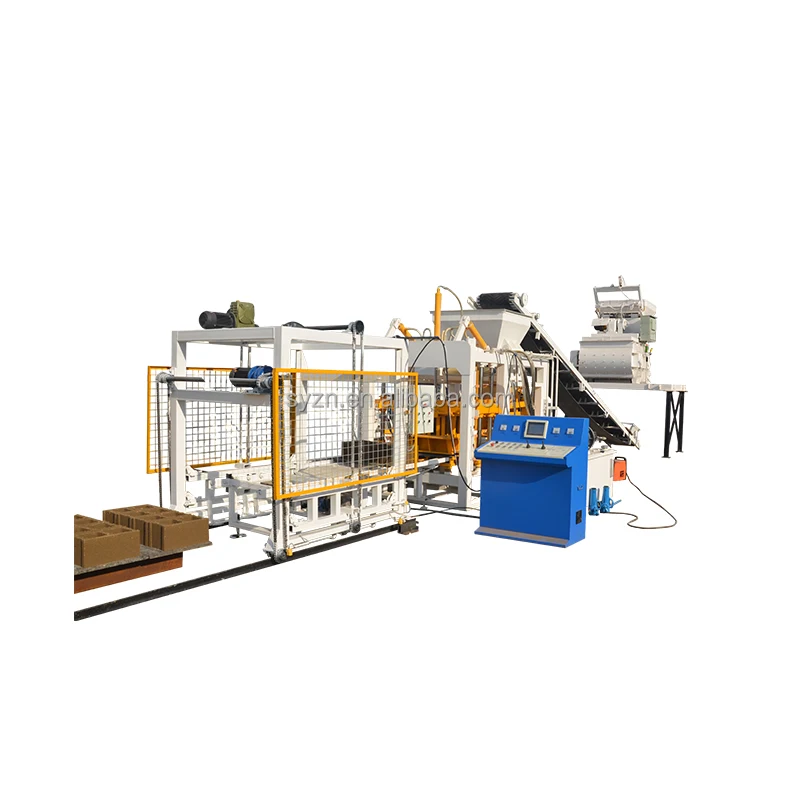
System-Synchronized Line Design — The QT4-15A quotation covers press, mixer, pallet feeder, conveyor and sweeper as a single matched flow, so the moulding cycle is never broken by an upstream or downstream station falling behind.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-15A |
| Product Type | Automatic Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 40–50 kN |
| Total Power | 18.45 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Net Weight | 3 T |
| Control System | PLC |
| Hydraulic Station | High-pressure hydraulic system included |
| Output Capacity — Hollow Block 400×200×200 mm | 4 pcs/mould, 408 pcs/hr, 3264 pcs/8hr |
| Output Capacity — Hollow Block 400×150×200 mm | 5 pcs/mould, 510 pcs/hr, 4080 pcs/8hr |
| Output Capacity — Solid Brick 240×115×53 mm | 18 pcs/mould, 2100 pcs/hr, 17000 pcs/8hr |
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Applied Products | Paver, solid block, hollow block, curbstone (via mould change) |
| Raw Materials | Crushed stone, sand, cement, dust, fly ash |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production plants | Crushed stone, sand, cement, fly ash mixes for 400×200×200 mm and 400×150×200 mm formats |
| Solid brick manufacturing | Cement and fine aggregate blends for 240×115×53 mm bricks |
| Paver and curbstone production | Denser mixes with higher cement content, switched via mould change on the same press |
| On-site construction block making | Self-contained line for housing and development projects producing blocks locally |
| Concrete product manufacturers expanding formats | Adding hollow block, paver or curbstone to an existing range using one press platform |
What "Pieces per Hour" Actually Means When the Line Stops Waiting
A block press only runs as fast as its slowest supporting station.
I once configured a QT4-15 class press for a plant in Southeast Asia where the buyer sourced the mixer and pallet return system separately. The press cycled fine on its own, but every hour it sat idle for fifteen minutes waiting for pallets to cycle back and fresh mix to arrive from an undersized mixer. The quoted output assumed continuous operation that the line could never sustain. The automatic block making machine production line approach with the QT4-15A avoids this by specifying the JQ350 mixer, pallet feeder, brick conveyor and sweeper together, with cycle times calculated against the 15–25 s moulding window so each station hands off to the next without the press losing rhythm [NEED_CITE: line synchronization principles in concrete block production].
How Station Synchronization Keeps the Press Running
The QT4-15A is configured around a 15–25 second moulding cycle. Within that window, the pallet feeder must deliver a fresh pallet, the mixer must supply enough material for the next mould charge, and the brick conveyor must clear the finished block before the next cycle begins. Each supporting station in this automatic block making machine production line is selected so its own cycle completes within the press cycle, not after it. When the pallet feeder, mixer and conveyor are matched to the press rather than purchased independently, the theoretical output per hour becomes achievable in actual shifts.
Where Material Flow Breaks Down in Unmatched Lines
A mixer that takes 90 seconds per batch but feeds a press cycling every 20 seconds creates a starvation point. Similarly, if pallets must be manually returned to the feeder after blocks are stripped at the curing area, the operator becomes the bottleneck. The QT4-15A line addresses these points by including the pallet feeder and brick conveyor as standard equipment, removing two of the most common flow interruptions [NEED_CITE: common bottlenecks in semi-automatic block plants]. The sweeper cleans the pallet surface before it re-enters the press, preventing residual concrete from affecting the next moulding cycle and reducing pallet rejection rates over time.
Reading the Specs That Determine Real Daily Output
The vibration force of 40–50 kN paired with the high-pressure hydraulic station determines how densely the concrete is compacted in the mould. Higher compaction means the block holds its shape immediately after demoulding, which matters for hollow blocks where wall thickness is thin and early strength must be sufficient for pallet transfer. The 4600 r/min vibration frequency works with this pressure to settle fine aggregate into voids, producing a denser block with less cement waste. The 850×550×25 mm pallet size must match the curing rack spacing and forklift tine width already in the buyer’s yard — specifying pallets without checking downstream handling equipment leads to double-handling that erodes the output the line was designed to deliver. The PLC control manages the sequence of hopper feed, vibration, hydraulic press and pallet advance, keeping cycle-to-cycle timing consistent across an eight-hour shift rather than relying on operator reflex.
The Cost of Treating Supporting Equipment as Optional
When pallet feeding and brick conveying are left out of the initial quotation to lower the purchase price, the buyer ends up paying for manual labor to fill those gaps every single shift. Blocks stacked by hand from the press outlet slow the cycle because the operator cannot clear finished pieces as fast as the press produces them [NEED_CITE: labor cost impact on block plant profitability]. Pallets dragged or carried back to the feed end accumulate surface damage faster, shortening their service life and increasing replacement frequency. These costs do not appear on the machine invoice but they appear on the plant operating statement within the first month of production.
Why Sourcing the Full Line from One Specification Matters
The QT4-15A press, JQ350 mixer, pallet feeder, brick conveyor and sweeper are specified against each other, meaning the motor ratings, belt speeds and pallet dimensions are cross-checked before the quotation is issued. Block machinery is the single focus here, so the configuration is not assembled from unrelated catalogue items. The capacity calculation states which block format each output figure assumes, rather than quoting a single number that only applies to the smallest brick. Mould design covers the formats the buyer’s market actually sells, including custom drawings when standard moulds do not match local block dimensions. Voltage, frequency and PLC display language are confirmed before production begins, so commissioning is not delayed by a control panel that arrives in the wrong language or a motor rated for a frequency the local grid does not supply [NEED_CITE: voltage and frequency standards by export market].
Documentation & Verification
- Line layout drawing showing station spacing and material flow path for the QT4-15A configuration
- Capacity calculation sheet stating output per format with the moulding cycle assumption noted
- Hydraulic and electrical schematic matching the as-built machine for maintenance reference
- Pallet specification confirming 850×550×25 mm dimensions and material grade
- Factory test record run on the buyer’s target block format before container loading
- Voltage, frequency and PLC language confirmation documented before production release
Installation, Commissioning & Support
- Foundation plan referencing the 7100×1600 mm footprint and 3 T net weight for slab design
- Power supply requirements based on the 18.45 kW total load with dedicated circuit recommendation
- Pallet feeder alignment to the press table verified during on-site commissioning
- PLC parameter setting for the buyer’s specific moulding cycle within the 15–25 s range
- Operator training covering mould change procedure across hollow block, solid brick and paver formats
- Wear parts list identifying hydraulic seals and vibration components with recommended replacement intervals
What to Prepare Before Requesting a Quotation
To size the QT4-15A line correctly, share the block formats your market sells most, the daily output target per format, and the raw materials available locally including aggregate grading. Confirm the voltage and frequency at the installation site, the PLC display language your operators need, and whether existing curing racks or forklifts constrain the pallet size. If you are replacing a press within an existing line, note which upstream and downstream equipment will remain so the new configuration can be matched to it.
Frequently Asked Questions
Q: How is the output capacity verified for each block format?
A: Each output figure states the exact block dimensions, pieces per mould, and the moulding cycle assumption. For example, 400×200×200 mm hollow blocks are rated at 408 pcs/hr based on 4 pcs per mould. No single blanket number is used across all formats, so you can calculate daily output for the specific block your plant will produce.
Q: Are pallet feeding and brick conveying included in the quotation?
A: Yes. The QT4-15A line includes the pallet feeder, brick conveyor and block sweeper as standard equipment within the quotation. These are not listed as optional extras or separate purchases, so the material flow from press to finished block is covered from the outset.
Q: How do the mixer and conveyor cycle times match the press?
A: The JQ350 mixer batch time and the brick conveyor speed are calculated against the 15–25 s moulding cycle of the QT4-15A. Each station is selected so it completes its task within the press cycle, preventing the press from idling while waiting for material or pallet clearance.
Q: What voltage and PLC language options are available?
A: Voltage, frequency and PLC display language are confirmed with the buyer before production begins. This ensures the motor ratings match the local grid and the control interface is readable by the operators who will run the line daily, avoiding commissioning delays.
Q: What is the typical timeline from order to container loading?
A: Lead time depends on the configuration and current production schedule. Once voltage, PLC language and mould selection are confirmed, the machine enters the production queue. Factory testing on the buyer’s target block format is completed before the unit is cleared for container loading.



