
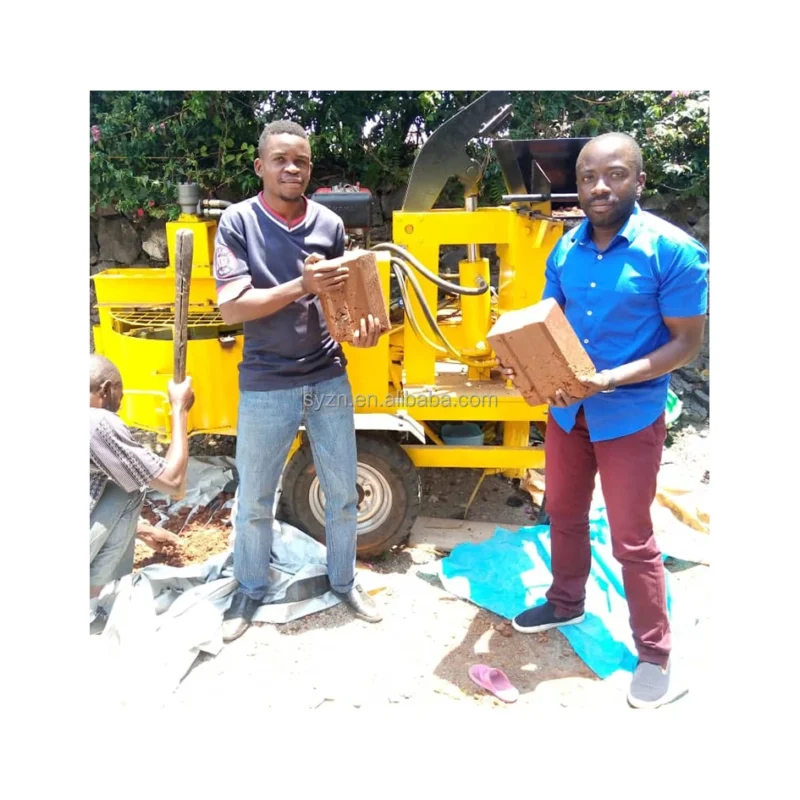
Matched Line Stations — The M7MI hydraulic interlocking block machine is integrated into a coordinated production setup where upstream mixing and downstream handling are sized to its 15–20 second molding cycle, preventing the press from standing idle while operators catch up.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Hydraulic Compressed Earth Interlocking Block Making Machine |
| Model | M7MI |
| Overall Dimensions (L×W×H) | 3200×1100×1500 mm |
| Net Weight | 1100 kg |
| Power Source | Diesel Engine |
| Rated Power | 7.5 kW |
| Hydraulic Pressure | 16 MPa |
| Molding Cycle | 15–20 s (basis not stated in source — depends on block format, material, and thickness) |
| Output Capacity | Up to 2200 pcs/day based on an 8-hour shift (basis not stated in source — confirm block format and material) |
| Production per Format (Example) | 300×150×100 mm interlocking block at a 20 s cycle, 1 pc/mould, approx. 200 pcs/h, approx. 1600 pcs/8 hr |
| Raw Materials | Clay, soil, concrete |
| Key Features | Mould change supported for different interlocking formats; mobile egg-laying assembly requiring no fixed plant foundation; manual operation |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site housing and infrastructure construction | Interlocking earth blocks stabilized with a small percentage of cement |
| Off-grid development projects with unreliable electricity | Diesel-powered production using locally sourced clay and soil |
| Expansion of existing block plant product ranges | Compressed cement-soil interlocking profiles for wall construction |
Why "Cycle Time" Means Nothing Without the Rest of the Line
A 20-second molding cycle only delivers real output if the mixer feeds fast enough and the wet blocks move off the curing floor without bottlenecking.
I have watched plant owners fixate on the press speed while the pan mixer upstream took 45 seconds per batch, leaving the Hydraulic Interlocking Block Making Machine production line sitting idle for a third of every shift. Others sized the mixer perfectly but had no plan for pallet handling, so freshly pressed blocks sat on the ground waiting for a wheelbarrow [NEED_CITE: block curing and handling logistics on mobile sites]. When you evaluate a turnkey setup, the press cycle must be synchronized with the raw material feeding, mixing station output, and the space required for curing, otherwise the headline capacity number remains theoretical.
Synchronizing the Mixer to the M7MI Press
When planning a complete block line, the mixing station is the most common failure point. The M7MI completes a cycle in roughly 15 to 20 seconds, which means the mixer must deliver a fresh, consistent batch of clay-soil-cement mix at that exact rhythm. If the mixer is undersized or relies on manual batching that varies from load to load, the Hydraulic Interlocking Block Making Machine production line will experience starved cycles, resulting in weak blocks that fail to interlock properly under load.
Managing Cured Output on a Mobile Site
A mobile egg-laying machine like the M7MI drops blocks directly onto the ground, eliminating the need for pallets but creating a different challenge: curing area management. The daily output requires a flat, level curing zone large enough to hold thousands of blocks without them being stepped on or driven over before the cement stabilizes [NEED_CITE: compressed earth block curing requirements]. Planning this footprint and the path for moving dried blocks to storage is part of the line design, not an afterthought.
What 16 MPa Means for Your Soil Mix
The hydraulic pressure rating of 16 MPa determines how densely the raw material is compacted into the mould. For compressed earth blocks, this pressure must be matched to the clay content and moisture level of your local soil. Too little pressure and the interlocking legs will be fragile; too much, and a highly clay-heavy mix might stick to the mould walls, slowing the cycle. The 7.5 kW diesel engine provides the power to reach this pressure consistently, which is critical when operating far from the electrical grid where voltage drops would otherwise compromise every block.
The Hidden Cost of an Unmatched Line
When the stations around the press are not specified together, the consequences are rarely obvious on day one. A mixer that cannot keep pace forces operators to run the press in bursts, wearing the hydraulic seals unevenly. A curing area that is too small leads to blocks being stacked while still green, causing the interlocking profiles to chip and deform. These issues look like machine failures, but they are actually line integration failures [NEED_CITE: common causes of block deformation in mobile production].
Sourcing the Line as a Single System
Specifying the M7MI alongside its raw material feeder, mixer, and site layout plan ensures the stations talk to each other. We configure the line against the buyer’s actual soil sample, not a catalog default, adjusting the mixer retention time to match local clay plasticity. Mould drawings are provided for the interlocking profiles the local market actually buys, and the daily capacity calculation states the exact block format assumed. The diesel engine configuration is confirmed for the site’s altitude and ambient temperature, so the 16 MPa pressure is achievable on arrival.
Documentation & Verification
- Line layout drawing showing station placement, curing area footprint, and material flow paths
- Capacity calculation sheet stating the exact block format and cycle time assumption
- Mould drawing and profile list for all available interlocking block formats
- Engine specification and hydraulic schematic confirming the 16 MPa system rating
- Factory test record run on a soil sample matching the buyer’s local material
Installation, Commissioning & Support
- Site leveling and compacted earth preparation to support the 1100 kg machine weight during operation
- Diesel fuel specification and filtration requirements confirmed for local supply quality
- On-site assembly of the mobile frame and hydraulic lines with pressure bleed and test cycle
- Mould change procedure training covering alignment and hydraulic clamp operation
- Initial production run supervised to match mixing ratios to the buyer’s specific soil sample
- Wear parts list provided with part numbers for hydraulic seals and mould liners
Starting the Conversation
To size a Hydraulic Interlocking Block Making Machine production line properly, we need to understand your project conditions. Please share a representative soil sample from your site, the specific interlocking block profile your market demands, and the daily volume you need to hit your project deadlines. We also need to know the altitude and typical ambient temperature, as these affect diesel engine performance and hydraulic efficiency.
Frequently Asked Questions
Q: How is the daily output of the M7MI calculated, and which block format is assumed?
A: The 2200 pieces per day figure is based on an 8-hour shift, but the exact output depends entirely on the block format. For example, a 300×150×100 mm interlocking block at a 20-second cycle yields approximately 1600 pieces in 8 hours. We provide a capacity calculation sheet that states the precise format, cycle time, and material assumption so the number reflects your actual production target.
Q: How do raw material feeding and mixing stations need to be sized to keep the M7MI running?
A: The mixer must deliver a fresh batch of clay, soil, and cement every 15 to 20 seconds to match the press cycle. This means selecting a pan mixer or ribbon blender with a batch volume and discharge speed that prevents the press from idling. We specify the mixer capacity and feed mechanism as part of the complete line layout.
Q: What curing arrangement is required downstream of a mobile egg-laying machine?
A: Since the M7MI drops blocks directly onto the ground, you need a flat, compacted curing area large enough to hold the daily output for several days until the cement stabilizes. We include the required footprint dimensions and material flow paths in the line layout so blocks are not moved or stacked while still green.
Q: How does the 16 MPa hydraulic pressure match different soil mix designs?
A: The pressure must be balanced against the clay content and moisture level of your local soil. High-clay mixes may require adjusted pressure or mould release agents to prevent sticking, while sandy mixes need maximum pressure for adequate density. We test your soil sample before finalizing the hydraulic setup to ensure consistent block strength.



