
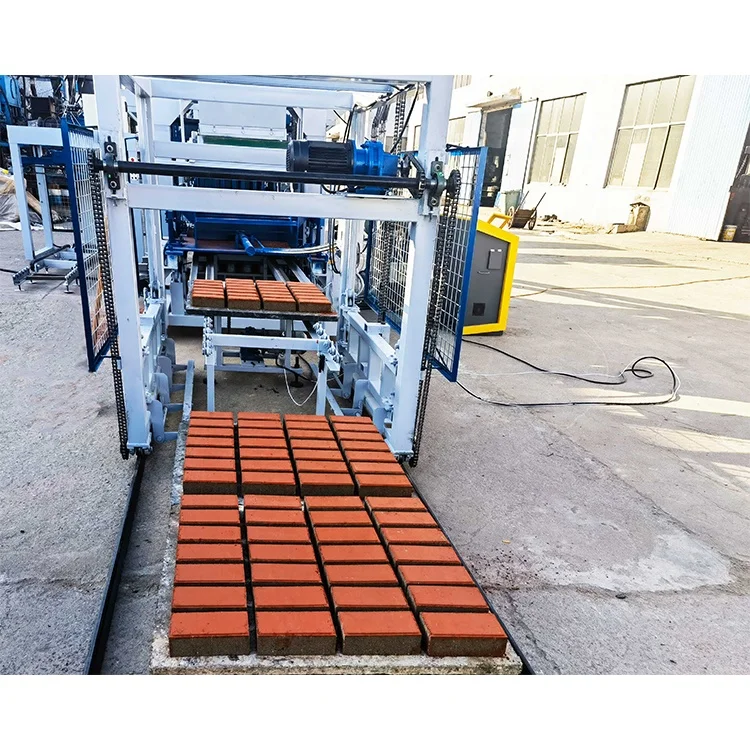
Matched Line Integration — The QT8-15 hydraulic block machine is specified alongside its feeding, mixing, pallet handling, and stacking stations so that cycle times align across every node, preventing the press from standing idle between strokes.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 8300×1860×3000mm |
| Rated Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency | 2800–4500 r/min |
| Vibration Force | 45 KN |
| Pallet Size | 950×900mm |
| Molding Cycle | 15–20s (basis not stated in source — confirm block format, material, and thickness) |
| Overall Power | 55.5 kW |
| Total Mass | 8 T |
| Demolding Method | Hydraulic |
| Applied Products | Hollow blocks, solid blocks, pavers, interlocking blocks, curbstone, colored pavers |
| Raw Materials | Crushed stone, sand, cement, fly ash, gravel, slag, dust |
| Factory Area | 300 m² (basis not stated in source — confirm whether minimum footprint or total production area including curing) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for residential and commercial walls | Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing for load-bearing structures | Gravel, sand, cement with high-density compaction |
| Paving block and colored paver runs for roads and walkways | Fine aggregate, cement, pigment additives |
| Interlocking brick production for landscaping and retaining walls | Sand, crushed stone, cement with precise moisture control |
| Curbstone forming for municipal and highway projects | Coarse aggregate, cement, slag blends |
Why the Supporting Equipment List Matters More Than the Press Alone
A block machine only produces as fast as its slowest upstream or downstream station allows.
When buyers evaluate a QT8-15 block machine production line, the conversation often stops at the press — its vibration force, cycle time, and pallet size. But in the field, the real constraint is rarely the press itself. It is the mixer that cannot discharge fast enough, the pallet return system that jams on warped boards, or the stacking station that falls two cycles behind and forces the operator to hand-stack wet blocks on the floor. I spent two weeks on a site in the Middle East where the aggregate had a high clay content, which threw off the entire batching rhythm; the mixer needed longer wet-mixing time, which in turn starved the press and desynchronized the stacker [NEED_CITE: raw material variability impact on block line synchronization]. The concrete block making line supporting equipment must be specified as a single coordinated system, not assembled from separate quotations.
Synchronizing Every Station to the Press Cycle
The QT8-15 block machine production line centers on a press with a 15–20 second molding cycle, but that number only holds if raw material arrives at the hopper on time and finished blocks clear the pallet before the next stroke begins. The raw material feeding system, mixer discharge rate, and pallet feeding mechanism must each be timed so the press never waits. When one station lags, the entire line throughput drops regardless of how fast the press can theoretically cycle.
Pallet Handling as the Hidden Bottleneck
Pallets travel through the press, into the curing area, and back to the feed station in a continuous loop. If the 950×900mm pallet size does not match the curing rack dimensions or the forklift capacity already on site, pallets pile up at the curing area entrance and the return conveyor starves. The pallet specification must be confirmed against the buyer’s existing infrastructure before the line is built, not after the first container arrives [NEED_CITE: pallet circulation requirements in concrete block plants].
Specifying the Line Around Local Aggregate and Mix Design
The vibration force of 45 KN and the rated hydraulic pressure of 21 MPa must be matched to the specific mix design the buyer will actually run. A mix high in fly ash behaves differently under vibration than one based on crushed stone and sand. When the concrete block making line supporting equipment — from the batching station to the mixer — is configured around a catalogue default rather than the buyer’s real material, block strength becomes inconsistent and demolding damage increases.
Reading the Numbers That Actually Matter
The 2800–4500 r/min adjustable vibration frequency allows the operator to tune compaction for different block formats — lower frequency for large hollow blocks where the concrete needs time to settle into the mould corners, higher frequency for thin pavers that require rapid densification. The 55.5 kW overall power draw reflects the combined load of the hydraulic pump, vibration motors, and conveyor drives; the electrical supply must provide a dedicated circuit at the confirmed voltage and frequency to avoid tripping during peak draw. The 8 T total mass indicates the structural steel in the frame and vibration platform, which directly affects how vibration energy transfers into the mould rather than dissipating into the foundation.
The Cost of Skipping Line-Level Configuration
When supporting stations are sourced separately or left out of the quotation entirely, the consequences show up within the first week of production. Pallets handled manually slow the return loop and the press sits idle between cycles. A mixer with insufficient capacity forces the press to run on partial batches, producing blocks with variable density. Stacking done by hand on the workshop floor means blocks cure in uneven conditions and breakage rates climb before they ever reach the customer [NEED_CITE: manual versus automated stacking impact on block breakage]. These are not press failures — they are line design failures that the buyer pays for every single shift.
What Sets This Line Configuration Apart
The QT8-15 is quoted as a coordinated system: the press, mould, pallet, and handling equipment are specified together so that cycle times match at every handoff point. The pallet size is chosen against the buyer’s curing area and forklift, not pulled from a standard list. The automation level is selectable — a buyer can start with semi-automatic pallet handling and add automatic stacking and cubing later as production volume grows. The line layout and capacity calculation state which block format each output figure assumes, so daily tonnage expectations are grounded in reality. Moulds are designed for the formats the buyer’s market actually sells, with custom drawings available when standard formats do not cover the requirement.
Documentation & Verification
- Line layout drawing with capacity calculation per block format assumed
- Machine specification sheet with hydraulic and electrical schematics
- Pallet specification matched to curing area and forklift capacity
- Voltage, frequency, and PLC display language confirmation before production
- Factory test record on buyer’s target block format before dispatch
- Wear parts and mould list with replacement part numbers
Installation, Commissioning & Support
- Foundation plan sized for the 8300×1860mm footprint and 8 T operating mass
- Dedicated power circuit confirmed for 55.5 kW total load at buyer’s voltage and frequency
- Machine shipped in dismantled state with reassembly sequence and bolt-torque specifications
- On-site commissioning with parameter tuning for buyer’s local aggregate and mix design
- Operator training covering mould change procedure and daily maintenance checkpoints
- Wear parts supply schedule aligned with hydraulic seal and vibration motor service intervals
Moving Forward With Your Line Inquiry
To configure the QT8-15 block machine production line around your actual production conditions, we need your target block formats and daily output requirement per format, the local aggregate types and typical mix proportions you will run, your available workshop area and curing space dimensions, and your site voltage and frequency. If you already have pallets, forklifts, or upstream batching equipment on site, share those specifications so the supporting equipment can be matched to what is already in place.
Frequently Asked Questions
Q: How is the line capacity calculated, and which block format does each output figure assume?
A: Capacity is calculated per block format, not as a single blanket number. The 15–20 second molding cycle varies depending on whether you are running hollow blocks, solid blocks, or pavers. Each output figure in the line layout states the specific block format, dimensions, and mix assumption behind it so you can match it to your actual product mix.
Q: Which supporting equipment stations are included, and where must cycle times match?
A: The quotation specifies which stations are included — raw material feeding, mixing, pallet feeding, stacking, curing rack handling, and cubing. Each station’s cycle time is matched to the press so that material arrives and finished blocks clear before the next stroke. Any station left out is clearly marked as buyer-supplied.
Q: How is the pallet size selected in relation to my existing curing area and forklift?
A: The 950×900mm pallet size is confirmed against your curing rack dimensions and the forklift capacity you already have on site. Choosing a pallet without this check leads to curing area congestion and pallet return delays that slow the entire line.
Q: What voltage, frequency, and PLC language will be confirmed before the machine ships?
A: Your site voltage, frequency, and preferred PLC display language are confirmed in writing before production begins. This prevents commissioning delays caused by mismatched electrical supply or an interface the operator cannot read.
Q: How does the raw material feeding and mixing station connect to the press?
A: The feeding and mixing station is timed so that a fresh batch reaches the press hopper before the current batch runs out. Mixer discharge rate, conveyor speed, and hopper level sensors are all set to keep the QT8-15 running continuously without waiting for material.



