
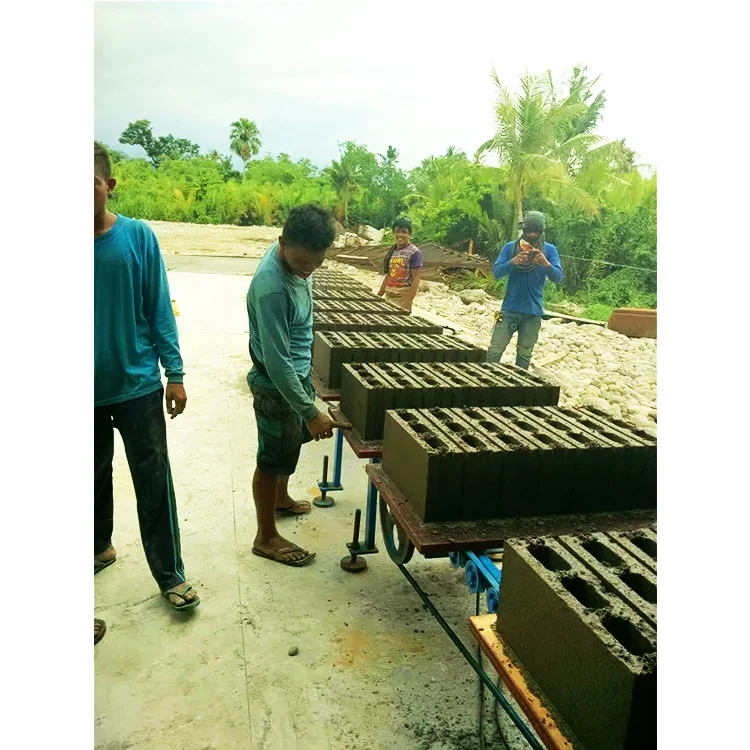
Matched Line Configuration — Every station from raw material feeding to stacking is timed so the Qt4-25a press never sits idle waiting for pallets or mix.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | Qt4-25a |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7100×1600×2610 mm |
| Net Weight | 5800 kg |
| Rated Power | 27.5 kW |
| Voltage & Frequency | 380V or configurable to buyer’s local standard |
| Control System | PLC with language options to confirm before order |
| Vibration Force | 60 kN |
| Pallet Size | 1020×850×40 mm |
| Mould Format Capability | Hollow block 400×200×200 mm, Hollow block 400×150×200 mm, Solid brick 225×112.5×53 mm |
| Output (Hollow 400×200×200 mm) | 960 pcs/hour, 7680 pcs/day (basis: 4 pcs/mould) |
| Output (Hollow 400×150×200 mm) | 1440 pcs/hour, 11520 pcs/day (basis: 6 pcs/mould) |
| Output (Solid 225×112.5×53 mm) | 3840 pcs/hour, 30720 pcs/day (basis: 16 pcs/mould) |
| Automation Level | Automatic |
| Color Options | Available according to buyer request |
| Warranty | 1 year |
| Standards | ISO 9001:2008, CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Fixed-plant hollow block production | Crushed stone, cement, sand and water mix for 400×200×200 mm and 400×150×200 mm hollow blocks |
| Solid brick manufacturing for masonry | Cement-based mix forming 225×112.5×53 mm solid bricks |
| On-site block line for housing projects | Local aggregate and cement producing structural and non-structural blocks |
| Building material distributor adding formats | Multiple mould changes across hollow and solid formats on one press |
What "7680 Blocks per Day" Leaves Out About Your Line
The headline capacity figure means nothing if the mixer cannot feed fast enough or the pallet return loop falls behind the press cycle.
I once watched a block plant in West Africa stall every forty minutes because the pallet feeder jammed on warped boards, and the operator spent the rest of the shift hand-stacking wet blocks onto the curing racks. The press itself ran fine — it was every station around it that created the bottleneck. When sizing an automatic concrete block making machine production line, the cycle time of the mixer discharge, the pallet indexing speed, and the stacking mechanism all have to match the press cadence or your real output drops well below the brochure number [NEED_CITE: common causes of block line downtime in tropical climates].
How the Stations Connect Around the Press
The Qt4-25a sits at the center of a sequence that begins with raw material batching and ends with green blocks on curing racks. The mixer must discharge a full batch into the hopper before the next mould cycle begins, and the pallet feeder must slide a fresh board under the mould box within seconds of the press lifting. If any station in this automatic concrete block making machine production line runs slower than the press, the controller holds the cycle and your hourly count drops.
Where Pallet Handling Decides Real Daily Output
Pallet size at 1020×850×40 mm dictates how many blocks ride on each board and how the boards stack on your curing racks. A pallet that does not match your existing forklift tine spacing means every board is moved twice. We confirm pallet material — bamboo, hardwood, or composite — against your local humidity and curing duration so warping does not turn a straight stack into a jam inside the return conveyor [NEED_CITE: pallet material selection for concrete block curing environments].
Reading the Specs That Shape Line Performance
The 60 kN vibration force works together with hydraulic pressure to compact the mix inside the mould box; if your local aggregate is fine and low in coarse fraction, the vibration transfers differently and block density can vary from one pallet to the next. The 27.5 kW total rated power covers the press motor, hydraulic pump, and conveyor drives, so your electrical supply must sustain that draw continuously across all three phases without voltage sag that would trip the PLC mid-cycle. Voltage is configurable from 380V to other industrial standards, but the exact frequency and plug configuration must be locked in before the control panel is wired. The PLC language and display prompts are set at the factory, so confirming the operator’s preferred language avoids commissioning delays once the line is bolted to the floor.
The Cost of Skipping Line-Level Verification
A buyer who treats the press as an island often discovers after arrival that the mixer output is too slow, the pallet return conveyor is missing, or the stacking station was never quoted. The result is an automatic line that runs in semi-automatic mode while workers hand-carry boards and hand-stack blocks — exactly the labour arrangement the investment was supposed to eliminate. We have seen projects lose entire curing cycles because the pallet quantity in the quotation did not cover the rack capacity, leaving wet blocks sitting on the press table until someone cleared a space [NEED_CITE: impact of incomplete line specification on block plant commissioning delays].
Why Sourcing the Full Line from One Supplier Matters
The Qt4-25a and every station around it are specified as a single system, so cycle times are calculated together rather than patched after delivery. Configuration starts with your actual mix design and local aggregate, not a catalogue default that assumes materials you cannot source. Mould formats are matched to the blocks your market actually buys, and custom mould drawings are available when standard sizes do not fit. Automation level is selectable — a buyer can begin with manual pallet handling and add automatic stacking later without replacing the press. Installation support includes on-site commissioning with operator training so the line runs at its verified capacity from the first full shift.
Documentation & Verification
- Line layout drawing showing mixer, feeder, press and stacker positions with cycle times per station
- Capacity calculation sheet stating the exact block format and mould cavity count assumed
- Pallet specification covering material, dimensions and quantity matched to curing rack layout
- Voltage, frequency and PLC display language confirmation signed before production begins
- Factory test record on your chosen block format before the line is dismantled for shipment
- Operation and maintenance manual with hydraulic and electrical schematics in the confirmed language
Installation, Commissioning & Support
- Foundation plan based on the 7100×1600 mm press footprint and dynamic load from 60 kN vibration
- Dedicated three-phase circuit sized for 27.5 kW continuous draw with voltage confirmed to local standard
- Machine shipped in dismantled modules with reassembly supervised on site during commissioning
- First-run parameter tuning of vibration duration and hydraulic pressure against your mix and aggregate
- Operator training covering PLC navigation, mould change sequence and daily greasing points
- Wear parts list identifying hydraulic seals, vibration springs and mould liner replacement intervals
What We Need to Size Your Line Correctly
Send us the block formats your market sells, the daily output you need for each format, and a sample of your local aggregate and sand. Include your site voltage and frequency, the language your operators read, and the curing area dimensions so we can match pallet quantity and rack handling. If you already own a mixer or forklift, share the specifications so the automatic concrete block making machine production line is built around what you have rather than replacing it.
Frequently Asked Questions
Q: How do I verify the daily output figure and which block format it assumes?
A: Every capacity figure we quote states the exact block format and mould cavity count behind it. For the Qt4-25a, 7680 pieces per day assumes 400×200×200 mm hollow blocks at 4 per mould. If your primary product is a different size, we recalculate and show the revised number before you commit.
Q: What supporting equipment is included in the line quotation, and what is left for me to source?
A: The quotation lists every station — mixer, raw material feeder, pallet feeder, press, and stacking method — with model numbers and cycle times. Items you must provide locally, such as compressed air supply or curing rack steel, are marked clearly so there are no surprises at arrival.
Q: How is the pallet size chosen to match my curing area and existing forklift?
A: The standard 1020×850×40 mm pallet is checked against your curing rack spacing and forklift tine width. If your existing racks are narrower or your forklift uses a different tine spread, we adjust the pallet dimension and confirm the change before the pallet order is placed.
Q: What voltage, frequency and PLC language options are confirmed before the machine is built?
A: We collect your site voltage, frequency, and the operator’s preferred PLC display language in writing before the control panel is assembled. This confirmation is attached to the production order so the electrical cabinet and HMI screens match your requirements when the line arrives.
Q: How do I ensure each station in the line has a matching cycle time so the press is not idle?
A: The line layout we provide lists the cycle time of every station — mixer discharge, pallet feed, press stroke, and stacking — in a single table. Any station slower than the press is flagged before order, and we propose a faster unit or a buffer conveyor to close the gap.



