
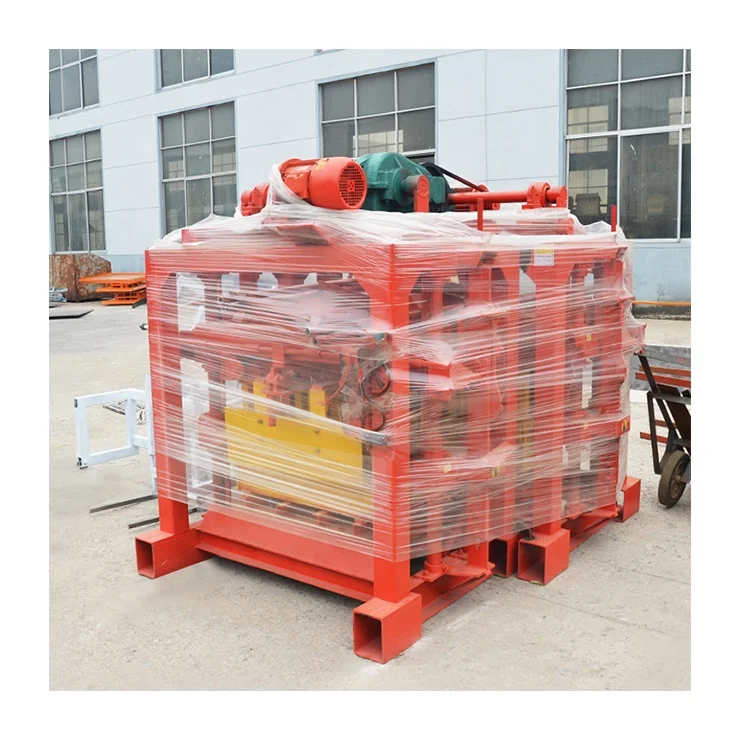
Semi-Automatic Block Making Machine Production Line Integration — the QTJ4-40 press is specified as one matched node within a complete block line, so raw material batching, pallet circulation, and curing handling are sized to its 40-second molding cycle rather than quoted as an isolated machine.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-40 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Rated Power | 9.5 kW |
| Molding Cycle | 40 s |
| Theoretical Productivity — 400×200×200 mm | 4 pcs/mould, 360 pcs/h, 2800 pcs/day |
| Theoretical Productivity — 400×150×200 mm | 5 pcs/mould, 450 pcs/h, 3600 pcs/day |
| Theoretical Productivity — 225×112.5×60 mm | 9 pcs/mould, 800 pcs/h, 6400 pcs/day |
| Vibration System | Bed mould vertical vibration + upper mould compression vibration |
| Control System | Semi-automatic, top die push-pull with automatic scraper |
| Pallet Size | 850 × 450 mm |
| Machine Weight | 1 T |
| Overall Dimensions | 1350 × 1460 × 1800 mm |
| Raw Materials | Concrete, sand, cement, fly ash, lime, gypsum |
| Voltage | According to buyer’s local voltage (basis to be confirmed) |
| Automation Level | Semi-automatic (manual pallet handling implied) |
| Standards | CE where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for small-to-medium block plants | Crushed stone, sand, cement, fly ash aggregates |
| Paver block manufacturing for walkways and yards | Concrete mixes with fine aggregate and pigment |
| Interlocking brick production for housing projects | Cement-stabilized soil, fly ash, lime blends |
| Solid brick runs for load-bearing masonry | Dense concrete mixes with graded sand |
| On-site contractor block production | Locally sourced aggregate and cement |
| First-plant entrepreneur setups | Multi-format output across standard block sizes |
What "2800 Pieces per Day" Leaves Out of the semi-automatic block making machine production line
The number only holds when every upstream and downstream station sustains the 40-second press cycle without interruption.
I once spent three weeks troubleshooting a line in a Gulf state where the host press ran perfectly, but the pallet return loop added twelve seconds every cycle because the curing racks were spaced for a different pallet dimension. The buyer had purchased a press, not a line, and daily output landed well below expectation. A semi-automatic block making machine production line only delivers its theoretical capacity when feeder discharge rate, mixer batch size, pallet magazine depth, and curing area turnover are each calculated against the same cycle tempo. [NEED_CITE: typical pallet circulation losses in semi-automatic block plants]
Matching Feeder and Mixer Throughput to the 40-Second Tempo
The QTJ4-40 cycles every 40 seconds, which means the mixer must discharge a fresh batch to the press hopper within that window or the press idles. For a semi-automatic block making machine production line, undersizing the mixer is the most common bottleneck. A pan mixer or twin-shaft mixer with a discharge volume aligned to the mould cavity fill requirement keeps material flowing without surge or starvation. The raw material feeder must also meter aggregate and cement at a rate that prevents the mixer from waiting between batches, especially when switching between fly ash-heavy and sand-heavy mixes.
Pallet Circulation and Curing Area Coordination
Each cycle consumes one 850 × 450 mm pallet, so across an 8-hour shift the curing loop must hold and return hundreds of pallets in continuous rotation. If the curing rack spacing does not match that pallet dimension, operators spend time adjusting or replacing pallets mid-shift. The semi-automatic block making machine production line must account for pallet quantity, rack geometry, and forklift turning radius so that cured blocks clear the rack before fresh ones arrive. [NEED_CITE: pallet-to-curing-rack compatibility standards in block production]
Reading the Specifications Against Real Production
The 9.5 kW rated power reflects the combined draw of the vibration motors and the hydraulic top-die push-pull mechanism. Dual vibration — vertical from the bed mould and compression from the upper mould — compacts the mix from both directions, which directly influences block density and early脱模 strength. The 1 T machine weight and 1350 × 1460 mm footprint determine the foundation slab thickness required beneath the press and the clearance needed between the mixer discharge chute and the press infeed. Pallet size at 850 × 450 mm is not interchangeable; it dictates the pallet feeder magazine capacity, the curing rack slot width, and whether the buyer’s existing forklift can handle loaded pallets without modification. The semi-automatic control with top-die push-pull and automatic scraper means an operator manually places and retrieves pallets, so labour planning must account for that station.
The Hidden Cost of Treating the Press as a Standalone Purchase
When pallet handling, stacking, and curing are left out of the quotation scope, the buyer discovers after installation that fresh blocks sit on the press table waiting for someone to carry them away. Output stacks by hand, cycle time stretches, and the 40-second rhythm the entire line was designed around breaks down at the exit station. I have seen contractors lose entire production days because the curing area was sized for a pallet count that ran out by mid-morning. These are not equipment failures — they are line-design omissions that turn a semi-automatic block making machine production line into a press with a manual bottleneck attached. [NEED_CITE: common line-design omissions in block plant installations]
Why Source the Full Line from One Specification Point
Block machinery as a single focus means the QTJ4-40 press, its mould, pallet, and handling equipment are specified as one matched system rather than assembled from separate suppliers whose cycle rates may not align. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default, so the vibration force and hydraulic pressure match what the material requires. Mould design covers the formats the buyer’s market actually sells, including custom drawings when a standard mould does not fit. The automation level is selectable — a buyer can start with the semi-automatic architecture and add pallet feeding or stacking later without replacing the press. Installation support includes line layout planning so that station spacing and material flow direction are resolved before the equipment ships.
Documentation & Verification
- Line layout drawing showing station positions and pallet circulation path around the QTJ4-40
- Capacity calculation document stating block format assumed for each output figure
- Pallet specification sheet confirming material, thickness, and curing rack compatibility
- Electrical schematic with voltage and frequency confirmed for all line stations
- Factory test record on the buyer’s target block format before dispatch
- Hydraulic and control system wiring diagram for the semi-automatic push-pull circuit
Installation, Commissioning & Support
- Foundation slab sized for the 1 T machine weight and 1350 × 1460 mm footprint
- Dedicated electrical circuit rated for the 9.5 kW total draw with confirmed local voltage
- Mixer-to-press infeed spacing set to match the 850 × 450 mm pallet feed path
- Vibration force and hydraulic pressure calibrated to the buyer’s submitted mix design
- Operator training on manual pallet handling rhythm at the 40-second cycle rate
- Wear parts list covering mould liners, scraper blades, and vibration motor brushes
What to Include in Your Inquiry
Share the block formats your market sells, the local aggregate and cement types available, and the daily output target so the semi-automatic block making machine production line can be configured around realistic cycle data rather than catalogue defaults. Include your site voltage and frequency, the curing area dimensions you can allocate, and whether you already hold pallets or forklifts of a specific size. State any existing upstream or downstream equipment that the new line must connect to.
Frequently Asked Questions
Q: How do I size the mixer and raw material feeder to sustain the QTJ4-40’s 40-second cycle without starving the press?
A: The mixer must discharge a full batch within the 40-second window, and the feeder must replenish the mixer before the next cycle begins. We calculate mixer capacity and feeder rate against your specific block format and mix density, then confirm the numbers in the line layout before production starts.
Q: What pallet material and quantity do I need to keep the curing loop running continuously across an 8-hour shift?
A: Pallet quantity depends on your curing time and the 850 × 450 mm dimension. We specify pallet material — bamboo, PVC, or steel — based on your climate and block weight, then calculate the total pallet count so the loop never runs dry mid-shift.
Q: Can I start with manual pallet handling and add automatic stacking or cubing later without replacing the press?
A: Yes. The QTJ4-40’s semi-automatic architecture with top-die push-pull leaves the pallet exit station open for future automation. Automatic stackers and cubing units can be added downstream as long as the pallet size and cycle tempo remain matched.
Q: How does the line layout change if I switch from 400×200×200 mm hollow blocks to 225×112.5×60 mm pavers?
A: Paver formats produce more pieces per mould but still cycle at 40 seconds, so pallet throughput and curing rack turnover must increase. We recalculate feeder rate, pallet count, and rack spacing for each format you plan to run before finalizing the layout.
Q: What voltage and control language must be confirmed before the full line ships?
A: Every motor and control panel across the line — not just the press — must match your site voltage and frequency. We also confirm the PLC or relay display language so operators can read diagnostics and cycle counters from day one without translation delays.



