
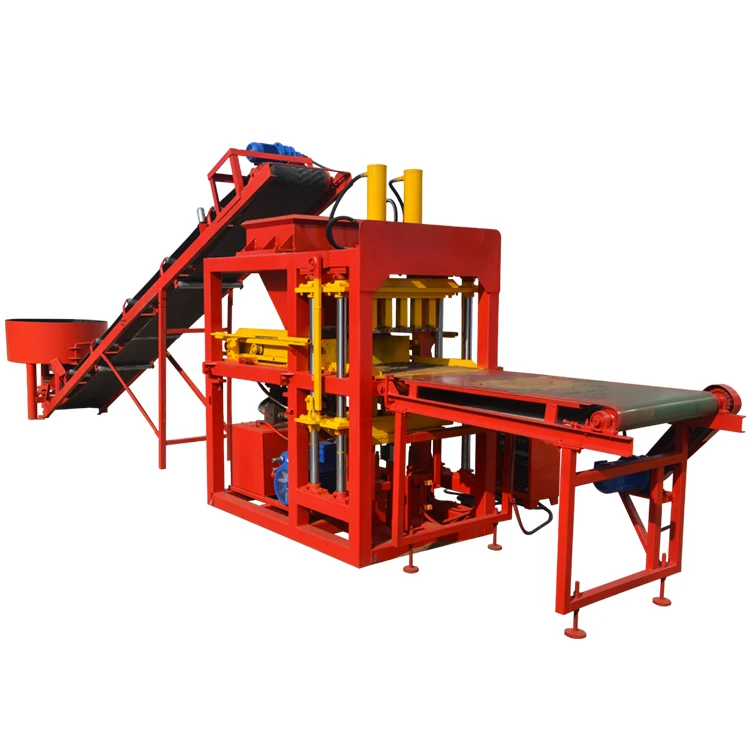
Line-Balanced Press Integration — every upstream feeder, mixer, and downstream stacker is sized against the LY4-10 cycle so the press never idles waiting for material or pallets.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY4-10 |
| Product Type | Automatic Clay Interlocking Block Making Machine |
| Rated Power | 11 kW |
| Control System | PLC control system with hydraulic system |
| Overall Dimensions | 2260 × 1500 × 2380 mm |
| Molding Cycle | 10–15 s (basis not stated in source — confirm block format / material / thickness) |
| Output per Cycle | 4 bricks (basis not stated in source — confirm block format) |
| Automation Level | Automatic material feeding, mould pressing, and mould lifting |
| Acceptable Raw Materials | Clay, soil, earth, mud, concrete, cement, fly ash, water |
| Mould Format | Interlocking bricks, multiple formats via mould change |
| Hydraulic Pressure | Not stated in source |
| Vibration Force | Not stated in source |
| Pallet Size | Not stated in source |
| Voltage & Frequency | Not stated in source |
| Net Weight | Not stated in source |
Application Suitability
| Application | Material or Output |
|---|---|
| Interlocking brick production for housing and commercial builds | Clay, soil, or cement-stabilised earth mixes |
| On-site block manufacturing for remote construction projects | Locally sourced mud, earth, and fly ash blends |
| Plant-based paver and interlocking block runs | Concrete and cement-aggregate mixes |
| Format changeovers within a single production shift | Multiple interlocking profiles via mould swap |
Why the Line Stops When One Station Is Misspecified
A press rated at a fast cycle is only as productive as the slowest station feeding or clearing it.
I once shipped a hydraulic block machine to a plant in West Africa without verifying their mixer discharge rate or stacker index speed. The press completed its cycle, then sat idle while the mixer caught up, and finished bricks queued faster than the stacker could index them. The buyer saw daily output fall well below expectation and blamed the press. The real fault was a line that had never been balanced as a single system [NEED_CITE: common causes of block line bottleneck in small-to-medium plants]. That experience now drives how every automatic clay interlocking block making machine production line we quote is mapped—station by station, cycle by cycle—before a single specification is locked in.
Mapping Every Station Around the LY4-10 Press
The LY4-10 operates on a PLC-controlled automatic cycle that covers material feeding, mould pressing, and mould lifting. To keep this automatic clay interlocking block making machine production line running without interruption, the raw material feeder must deliver a consistent batch volume within the press cycle window, and the mixer must discharge before the next feed call. When any upstream station lags, the PLC simply waits, converting a fast press into a slow line.
Pallet Flow and Stacking — The Downstream Half of the Equation
On the exit side, freshly pressed interlocking bricks ride on pallets that must be collected, stacked, and moved to the curing area before the next pallet is called. If the stacker index time exceeds the press cycle, wet bricks queue on the conveyor and risk surface damage. We therefore specify pallet dimensions, stacker lift capacity, and curing-rack spacing as one package so the downstream flow matches the 10–15 s moulding window [NEED_CITE: pallet handling standards for hydraulic block plants].
Reading the Numbers That Actually Matter
The 11 kW rated power defines the minimum dedicated circuit the buyer must provide; undersizing the supply causes voltage sag during the hydraulic pump start, leading to inconsistent pressing force. The PLC control system coordinates the hydraulic ram and mould lift in a single timed sequence, so any change in hydraulic fluid viscosity—common in tropical or cold climates—must be compensated during commissioning. Mould change capability lets the buyer switch between interlocking profiles on one press, but the time taken to swap, align, and test a new mould directly determines how many formats are practical within a single shift.
The Hidden Cost of Skipping Line Balance
Buyers who purchase the press alone and source mixers, conveyors, and stackers locally often discover that mismatched cycle times create micro-stoppages. Over a full shift these short pauses accumulate into significant lost output and extra labour spent manually moving pallets that the stacker could not clear in time [NEED_CITE: shift-level productivity loss from unbalanced block lines]. Rectifying the mismatch after installation usually means replacing at least one station, adding cost and downtime that a balanced quotation would have avoided.
Why Procure the Full Line from One Source
Block machinery is our single focus, so the LY4-10 press, its moulds, pallets, and handling equipment are specified as one matched system rather than assembled from separate suppliers. Configuration is set against your actual mix design, local aggregate, and target block format, not a catalogue default. Mould design covers the interlocking profiles your market sells, and custom drawings are available when standard formats do not fit. Automation level is selectable, allowing a buyer to start with the automatic feed and press cycle and add pallet stacking or cubing later. Installation and commissioning support includes operator training so the line runs at its intended rhythm from the first shift.
Documentation & Verification
- Line layout drawing showing every station and its cycle time relative to the LY4-10 press
- Machine specification sheet with hydraulic and electrical schematic confirming voltage and control language
- Mould drawing and format list for each interlocking profile included in the order
- Pallet specification matched to your curing area dimensions and existing forklift capacity
- Factory test record run on your nominated raw material mix before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 2260 × 1500 mm press footprint and dynamic load of the hydraulic ram
- Dedicated 11 kW circuit with correct voltage and frequency confirmed before wiring begins
- Press arrives partially assembled; hydraulic hoses and PLC cables connected on-site during commissioning
- First-run parameter setting covers hydraulic pressure, mould lift height, and feed volume for your mix
- Operator training includes mould change procedure and daily greasing points on the guide columns
- Wear parts list identifies hydraulic seals and mould liners with recommended replacement intervals
What to Share Before Requesting a Quotation
To size the automatic clay interlocking block making machine production line correctly, please confirm the interlocking brick dimensions and daily output target you need to hit. Tell us which raw materials—clay, soil, cement, fly ash—are available locally and in what proportions. Share your site voltage, frequency, and the language your operators read on a control screen. If you already own a mixer, forklift, or curing racks, send their specifications so the line layout accounts for existing equipment rather than duplicating it.
Frequently Asked Questions
Q: How do I verify realistic daily output when the cycle time is quoted without a stated block format?
A: Ask the supplier to provide a capacity table that lists cycle time and pieces per hour for each specific interlocking format you intend to produce. Without this, the quoted 10–15 s cycle may reflect a thin paver rather than the thicker interlocking brick you plan to sell, making daily output figures unreliable for your business plan.
Q: Which supporting stations must match the press cycle to avoid bottlenecks?
A: The raw material feeder, mixer discharge rate, pallet return conveyor, and stacker index speed all need to complete their tasks within or faster than the press moulding cycle. If any station is slower, the PLC pauses the press and daily output drops accordingly.
Q: How do I confirm voltage, frequency, and PLC display language before the line ships?
A: Provide your local utility specification and preferred HMI language during the inquiry stage. The supplier should return a written confirmation showing the exact motor rating, control voltage, and screen language that will be factory-set before the container is sealed.
Q: How does pallet size selection relate to my existing curing area and forklift?
A: Pallet length and width determine how many bricks fit on one curing rack tier and whether your current forklift can lift a loaded rack. Confirming these dimensions early prevents a situation where new pallets arrive but cannot be handled by the equipment already on your floor.



