
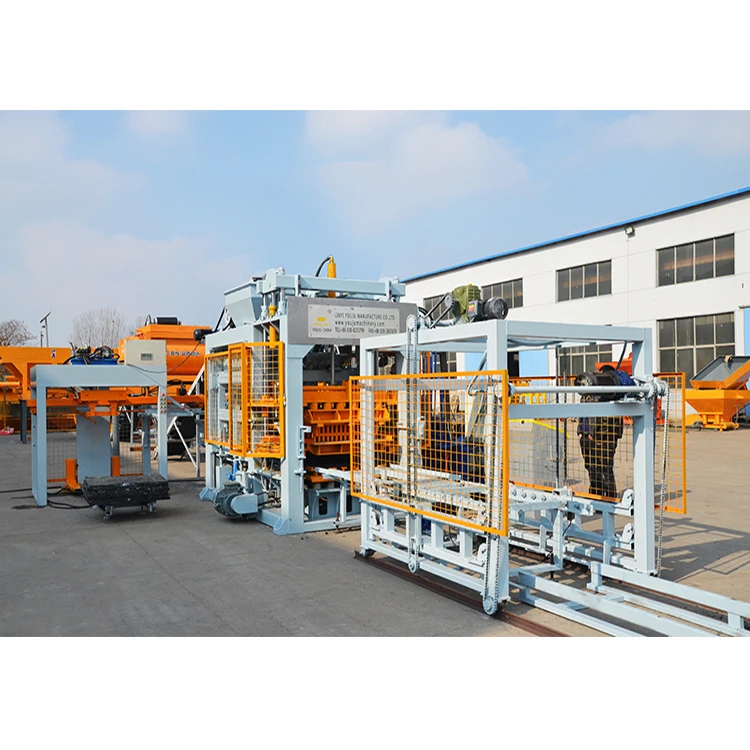
Matched System Integration — every station from the JS750 mixer through the pallet feeder and block conveyor is timed to the QT8-15 press cycle so the host machine runs without idle gaps.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT8-15 |
| Product Type | Fully Automatic Hydraulic Concrete Block Making Machine Production Line |
| Overall Dimensions (L×W×H) | 8300 × 1860 × 3000 mm |
| Molding Cycle | 15–20 s (basis not stated in source — confirm block format and material) |
| Exciting Power (Vibration Force) | 55 kN |
| Rated Power | 37.2 kW |
| Mixer Model | JS750 |
| Pallet Size | 1020 × 900 mm |
| Total Weight | 8 T |
| Applied Products | Paver, solid block, hollow block, curbstone (via mould change) |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Control System | PLC control system |
| Hydraulic Station | High-pressure hydraulic system included |
| Automation Level | Fully automatic |
| Output Capacity | 1920 pcs/hour (basis not stated in source — confirm block format and material) |
| Included Equipment | Block making machine, hydraulic station, PLC control unit, pallet feeder, block mould, material feeder, block conveyor, block sweeper, spare parts and tools |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for wall construction | Crushed stone, sand, cement, fly ash blends |
| Solid block manufacturing for load-bearing structures | Dense aggregate and cement mixes |
| Paving block output for roads and walkways | High-strength concrete with fine aggregate |
| Curbstone forming for infrastructure projects | Coarse aggregate and cement under high hydraulic pressure |
What "1920 Pieces per Hour" Leaves Out on a QT8-15 Block Making Machine Production Line
Capacity figures only matter when the block format behind them is named.
A number like 1920 pieces per hour sounds decisive on a quotation sheet, but it hides the assumption underneath. I have stood in block plants where the press was rated for a certain hourly output on a small solid block, yet the buyer’s market actually demanded hollow blocks that took twice the cycle time. The line spent half the day falling short of what the paperwork promised. Before any QT8-15 block making machine production line is ordered, the capacity calculation needs to state which format — hollow, solid, paver, or curbstone — was used to derive the number, along with the mix design and mould configuration. [NEED_CITE: how block format assumptions affect quoted capacity in machinery proposals]
Synchronizing Every Station Around the Press
The QT8-15 block making machine production line is built around a principle I learned the hard way on site: the press is only as fast as its slowest upstream or downstream station. The JS750 mixer, material feeder, pallet feeder, block conveyor, and sweeper are specified together so their individual cycle times align with the 15–20 second molding window. When a mixer batch finishes late, or a pallet arrives a few seconds behind schedule, the press sits idle and the quoted capacity becomes theoretical. Matching these intervals at the engineering stage — rather than adjusting them during commissioning — is what keeps the line running at its intended rhythm throughout a shift.
Pallet Handling as a Line Component, Not an Afterthought
Pallet size and movement dictate how much finished output actually leaves the press area each hour. The 1020 × 900 mm pallets on this line are fed automatically, which removes the bottleneck of an operator manually placing boards between cycles. I have seen plants where the press was fully automatic but pallets were still carried by hand, cutting real output noticeably below the rated figure. On the QT8-15 block making machine production line, the pallet feeder and block conveyor work as a continuous loop, returning spent pallets and delivering fresh ones without pausing the press. [NEED_CITE: impact of pallet circulation speed on block line throughput]
Reading the Specs That Actually Shape Daily Output
The 55 kN vibration force and the high-pressure hydraulic station work together to compact the concrete mix into a dense, consistent block. Vibration alone settles the aggregate, but hydraulic pressure locks it in place; if either value is mismatched to the buyer’s local aggregate gradation, block strength will vary from batch to batch. The JS750 mixer must produce a homogeneous blend at the rate the press consumes it — too slow and the press waits, too fast and the mix begins to set before forming. The PLC control system coordinates these variables across each cycle, holding timing and pressure within set tolerances. The 37.2 kW rated power reflects the combined demand of vibration, hydraulics, and conveyors running simultaneously, which must be matched to the site’s electrical supply before installation begins.
The Cost of Skipping Line-Level Configuration
Buying a press on its own and sourcing the mixer, pallet system, and conveyor separately often looks cheaper on paper. In practice, mismatched cycle times between stations cause the press to idle repeatedly, wearing hydraulic seals faster and consuming power without producing blocks. [NEED_CITE: consequences of unsynchronized station cycles in block plants] I have watched plants lose an entire shift’s output because a pallet feeder from a different supplier could not keep pace with the press, and the buyer had no single supplier accountable for the gap. Sourcing the QT8-15 block making machine production line as one integrated system means every station is warranted to work at the same tempo.
Why This Line Is Specified as a System
Block machinery is our single focus, so the QT8-15 is configured as a matched set — press, mould, pallet, mixer, and conveyor — rather than assembled from separate catalogues. Each proposal starts with the buyer’s actual block format, local aggregate, and daily output target, not a default template. Mould design covers the formats the buyer’s market sells, and custom drawings are available when standard options do not fit. The automation level is selectable, allowing a plant to begin with the included equipment and add downstream stacking later. Voltage, frequency, and PLC display language are confirmed before production so the line can be commissioned on arrival without electrical rework.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for output figures
- Machine specification sheet covering press, mixer, pallet feeder, and conveyor ratings
- Mould drawing and format list for paver, hollow, solid, and curbstone configurations
- Hydraulic and electrical schematic matching the confirmed voltage and frequency
- Factory test record on the buyer’s specified block format before dispatch
- Operation and maintenance manual with wear parts and mould replacement intervals
Installation, Commissioning & Support
- Foundation plan sized to the 8300 × 1860 mm footprint and 8 T operating weight
- Dedicated electrical circuit sized for the 37.2 kW rated power and confirmed voltage
- On-site assembly of press, mixer, pallet feeder, and conveyor with station alignment
- PLC parameter setup and cycle timing adjustment to the buyer’s block format
- Operator training covering mould change, hydraulic checks, and daily maintenance routines
- Wear parts list with reorder intervals for hydraulic seals and mould liners
What to Share Before Requesting a Quotation
To size the QT8-15 block making machine production line to your plant, we need the block formats your market buys, the target daily output per format, and the raw materials you source locally. Share your site’s voltage, frequency, and preferred PLC language so the control system is built to match. If you already have a curing area or forklift in place, send those dimensions so the 1020 × 900 mm pallet specification can be validated against your existing handling equipment.
Frequently Asked Questions
Q: How is the 1920 pcs/hour capacity calculated, and which block format does it assume?
A: That figure is derived from a specific block format, mould configuration, and mix design — details that must be stated alongside any capacity claim. We provide a written capacity calculation for each format you intend to produce, so you can compare hollow block, solid block, paver, and curbstone outputs individually before placing an order.
Q: How do the mixer, feeder, pallet feeder and conveyor cycle times synchronize with the press?
A: Each station on the QT8-15 block making machine production line is specified with a cycle time that falls within the 15–20 second press window. The JS750 mixer batch size, material feeder discharge rate, and pallet feeder return speed are all calculated against the press rhythm during the proposal stage, not adjusted empirically after arrival.
Q: What voltage, frequency and PLC language options are available for the destination market?
A: Voltage and frequency are confirmed during the proposal stage to match your site supply. The PLC display language is set before production so operators can read menus and alarms in their working language from the first day of commissioning, avoiding delays caused by untranslated control screens.
Q: Is automatic stacking and cubing available as a downstream upgrade to this line?
A: The standard QT8-15 line includes the block conveyor and sweeper as downstream equipment. Automatic stacking and cubing can be added as an extension once the core line is running, with the pallet return system and conveyor layout designed to accommodate the upgrade without repositioning the press.



