
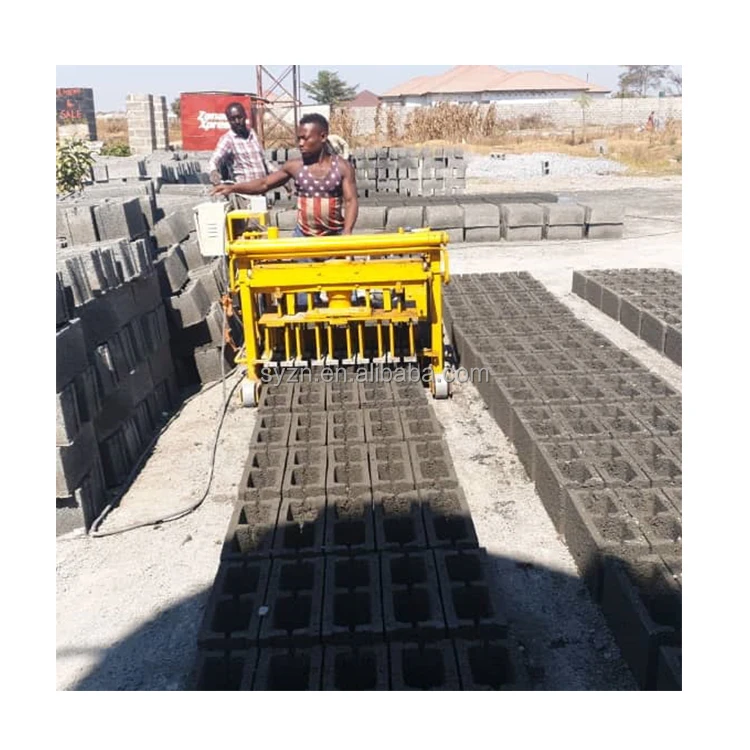
Matched System Integration — raw material feeding, mixing, and curing workflow are configured around the QMY4-30 mobile block machine so the press is never left waiting for the next batch.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMY4-30 |
| Product Type | Mobile Pallet-free Block Making Machine |
| Hydraulic Method | Mould vibration |
| Demold Method | Hydraulic |
| Molding Cycle | 25-30 seconds |
| Total Power | 5.95 kW |
| Pallet Requirement | Pallet-free (mobile egg-laying type) |
| Automation Level | Semi-automatic / Manual operation |
| Output Capacity (400×200×200mm hollow block) | 4 pcs/mould, 480 pcs/hour, 3840 pcs/8hr |
| Output Capacity (400×150×200mm hollow block) | 5 pcs/mould, 600 pcs/hour, 4800 pcs/8hr |
| Output Capacity (400×100×200mm hollow block) | 7 pcs/mould, 840 pcs/hour, 6720 pcs/8hr |
| Suitable Terrain | Mountainous, hilly, industrial mining, desert and coastal areas |
| Voltage & Frequency | Configurable to buyer’s local standard (basis to be confirmed) |
| Control System | PLC or relay logic (basis to be confirmed) |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production at building project locations | Crushed stone, sand, cement, water mixed to local aggregate profile |
| Remote infrastructure projects in difficult terrain | Concrete hollow blocks laid directly on prepared ground without pallets |
| Small-scale block manufacturing for first-time producers | 400×200×200mm, 400×150×200mm, and 400×100×200mm hollow block formats |
| Contractor-run block production at housing developments | Semi-automatic operation with manual material feeding and ground curing |
What "Pallet-Free" Really Means for Your Production Line
Eliminating pallets removes an entire material handling loop — but only if the curing area and upstream mixing are planned as part of the same mobile block machine production line.
When buyers see "pallet-free" they often assume the rest of the line takes care of itself. In practice, blocks laid directly on the ground need a flat, prepared curing surface that is large enough for the day’s output and accessible for watering and protection. The mixer must feed the hopper at a rate that matches the 25-30 second molding cycle, or the press sits idle while workers wait for the next batch. I have watched contractors arrive at a site with the machine and nothing else, only to spend the first week leveling ground by hand before a single block was produced. [NEED_CITE: ground preparation requirements for mobile egg-laying block machines]
How the Mobile Block Machine Production Line Connects Upstream
The QMY4-30 sits at the center of a workflow that starts with raw material batching and ends with ground-cured blocks ready for stacking. A pan mixer or drum mixer feeds mixed concrete into the machine hopper, and the feed rate must keep pace with the molding cycle. If the mixer batch size is too small, the press completes a cycle and waits. If it is too large, mixed material begins to set before it reaches the mould. Configuring the mixer capacity and feed method against the 5.95 kW total power draw and the 25-30 second cycle is what turns a standalone mobile block machine into a functioning mobile block machine production line.
Planning the Curing Zone Without Pallets
Without pallets to carry blocks from press to curing rack, the curing area must move with the machine or be large enough to accommodate a full shift of output in one location. For the 400×200×200mm hollow block format producing 3840 pieces in an eight-hour shift, the ground area required is substantial. The site layout must account for machine travel path, block spacing for air circulation, and water access for curing. [NEED_CITE: curing area calculation methods for pallet-free block production] Skipping this step means blocks are left too close together, stick to one another, or cure unevenly.
Reading the Specs That Actually Matter on Site
The mould vibration method paired with hydraulic demolding determines how densely the concrete is compacted and how cleanly the block releases from the mould. Vibration force and hydraulic pressure must be matched to the buyer’s specific mix design — a dry mix with coarse local aggregate needs different settings than a wetter mix with fine sand. The three stated output capacities are each tied to a specific block format, so a buyer planning to produce mainly 400×100×200mm blocks will see a different daily figure than one focused on the larger 400×200×200mm format. Total power at 5.95 kW is modest, which keeps generator sizing manageable on remote sites, but the voltage and frequency must still match the local supply or the generator set brought to the project. [NEED_CITE: voltage and frequency standards by export market]
The Cost of Skipping Line Integration
Treating the QMY4-30 as a standalone unit rather than the center of a connected mobile block machine production line leads to predictable problems. The mixer cannot keep up, the curing ground is too small, and blocks are moved by hand before they have gained enough green strength. Voltage mismatches are the most expensive oversight — I once spent three weeks waiting for a transformer to arrive at a project site because the supply frequency was not confirmed before the machine shipped. The machine sat under a tarp while the contractor paid idle crew wages and missed a project milestone. [NEED_CITE: commissioning delays caused by electrical specification mismatches]
Why Source the Full Line from One Supplier
Block machinery is our single focus, so the QMY4-30 is specified together with its mixer, material feed arrangement, and curing workflow as one matched system. Configuration is set against the buyer’s actual mix design and local aggregate rather than a catalogue default. Mould options cover the hollow block formats the buyer’s market actually sells, with custom drawings available. Automation level is selectable, allowing a buyer to start with manual operation and add automated feeding later. Installation support includes operator training on-site so the crew understands cycle timing and material flow from the first day.
Documentation & Verification
- Line layout and capacity calculation stating the hollow block format assumed for daily output
- Machine specification sheet with total power, cycle time, and mould vibration parameters
- Mould drawing and format list for 400×200×200mm, 400×150×200mm, and 400×100×200mm blocks
- Voltage and control system confirmation record before production begins
- Factory test record on the buyer’s selected block format before dispatch
- Operation and maintenance manual with wear parts list for hydraulic and mould components
Installation, Commissioning & Support
- Ground leveling and curing area preparation sized to 3840 or more blocks per shift based on selected format
- Electrical connection confirmed to local voltage and frequency before the QMY4-30 is energized on site
- Mixer and feed arrangement positioned to match the 25-30 second molding cycle without material starvation
- First-run parameter adjustment for mould vibration and hydraulic demolding against local aggregate mix
- Operator training on semi-automatic cycle sequence, mould change procedure, and daily greasing points
- Wear parts and mould inventory list provided with recommended reorder intervals for continuous production
What We Need to Configure Your Line
Tell us which hollow block format your market demands most, the daily output you are targeting, and the aggregate materials available near your project site. Share the local voltage and frequency so we can confirm the electrical package before production. If you already have a mixer or generator on site, send the specifications so we can check compatibility with the QMY4-30 and plan the mobile block machine production line around what you already own.
Frequently Asked Questions
Q: How is daily output calculated and which block format is each figure based on?
A: Each output figure is tied to a specific hollow block size. The 3840 pieces per eight-hour shift applies to 400×200×200mm blocks at four per mould. The 4800 figure assumes 400×150×200mm at five per mould, and 6720 assumes 400×100×200mm at seven per mould. Your actual daily output depends on which format you run and how consistently the mixer feeds the press.
Q: What raw material feeding and mixing setup keeps the QMY4-30 running without waiting?
A: The mixer batch size and discharge rate must match the 25-30 second molding cycle. A pan mixer with a batch capacity that delivers one full hopper load per cycle is typical. We size the mixer and feed conveyor against your selected block format and target output so the press does not sit idle between cycles.
Q: How do you plan curing area and workflow when there are no pallets?
A: The ground surface must be flat, level, and large enough for a full shift of blocks with spacing for air circulation. We calculate the required area based on your chosen block format and daily target, then lay out machine travel paths and water access points so curing is managed as part of the line.
Q: What voltage and frequency options are available for different target markets?
A: The QMY4-30 electrical package is configured to match your local supply before production. We confirm voltage, frequency, and plug type during the order process. I always verify this twice because a mismatch discovered after arrival delays commissioning by weeks while transformers or rewiring are arranged.
Q: How does the mobile machine integrate with upstream batching and downstream block handling?
A: Upstream, the mixer and feed system are positioned to deliver concrete at the pace of the molding cycle. Downstream, blocks are laid on prepared ground and remain in place for curing. The mobile block machine production line connects these stages so material flow is continuous and blocks are not moved before gaining adequate green strength.


