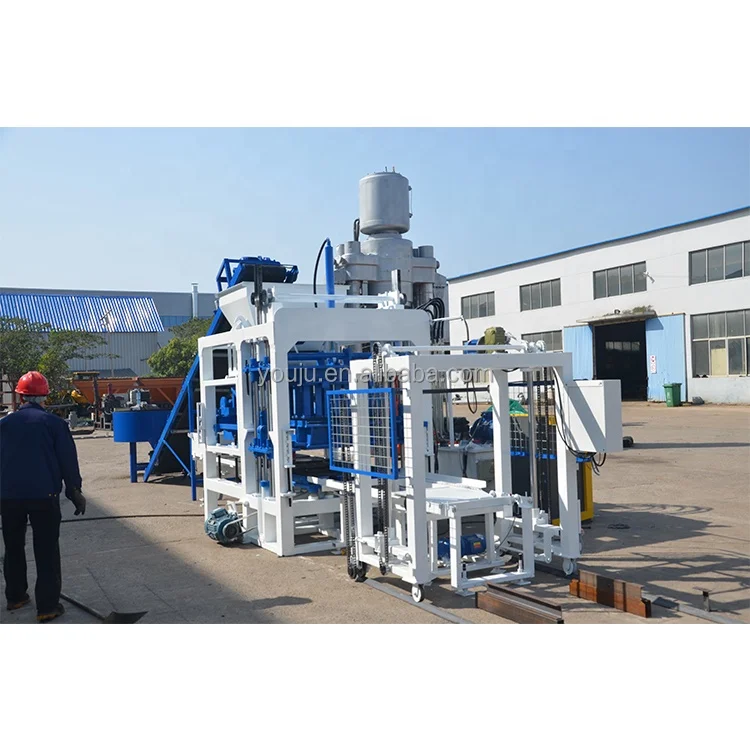
Integrated System Engineering — The QT4-18 line treats mixer, conveyor, host press, and stacking equipment as one synchronized unit rather than separate purchases, eliminating idle gaps where the press waits for material or pallets to arrive.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT4-18 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 2500 × 1750 × 2200 mm |
| Rated Pressure | 16 MPa |
| Vibration Form | Platform Vibration |
| Pallet Size | 950 × 550 mm |
| Molding Cycle | 18–25 s (basis to be confirmed) |
| Overall Power | 27.5 kW |
| Control System | PLC with frequency converter |
| Electrical Components | Schneider |
| Mold Lifting Mechanism | Double-sided sync gears |
| Material Feeding System | Distribution belt hopper |
| Concrete Mixer | JQ500 |
| Belt Conveyor | 8 m (6 m optional) |
| Support Equipment | Stacker, block gripper, trolley, concrete batching plant |
| Assembly State | Requires foundation preparation per layout drawing |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, and fly ash blends |
| Solid block manufacturing | Dense aggregate mixes for load-bearing walls |
| Paving block production | Fine aggregate with pigment for colored pavers |
| On-site contractor production | Locally sourced aggregate for housing projects |
| Medium-scale plant operations | Daily runs across multiple block formats with mould changes |
What "18–25 Seconds" Actually Means for Your Line
A molding cycle quoted without naming the block format is a number that cannot be translated into daily output.
Buyers often see a cycle time and multiply it across an eight-hour shift, only to discover the real throughput falls far short once the format, mix design, and pallet handling are factored in. A hollow block and a thin paving block do not share the same cycle, even on the same press. The QT4-18 is configured around your target block format, and the capacity calculation we provide states which format the 18–25 s range assumes so your production planning starts from an honest number [NEED_CITE: block format impact on cycle time in hydraulic press operations]. When the mixer, belt conveyor, and pallet loader are all sized to that confirmed cycle, the concrete block production line runs without the press sitting idle between strokes.
How Raw Material Feeding Keeps the Press Running
The JQ500 concrete mixer is matched to the QT4-18 throughput so that each batch arrives at the distribution belt hopper before the previous cycle completes. The 8 m belt conveyor transfers mixed material at a rate that aligns with the molding cycle, preventing the common bottleneck where the press finishes a pallet and waits for the next feed. If your site has space constraints, the 6 m conveyor option shortens the footprint without sacrificing feed rate. This synchronization is the first link in a concrete block production line that actually delivers the output the press is rated for.
Pallet Handling and Block Removal Without Manual Lifting
The pallet loader uses a hydro-cylinder to push a fresh pallet onto the vibrating platform while simultaneously ejecting the finished block onto the recipient conveyor. One motion accomplishes two actions, closing the gap that typically appears when pallet feeding and block removal are treated as separate steps. The block conveyor then transports products to the front idlers where the stacker picks them up for curing rack placement. The block gripper and trolley complete the loop, moving wet blocks to the curing area without manual lifting [NEED_CITE: ergonomic and safety standards for manual handling in concrete product plants]. This is where a block line and supporting equipment package differs from buying a press alone — the entire material flow is accounted for before installation day.
Reading the Specifications That Matter Beyond the Press
The 16 MPa rated pressure and platform vibration work together to compact the mix into the mould cavity. Higher pressure alone does not guarantee block strength; the vibration frequency must match the aggregate particle size in your local mix so that fines fill the voids between coarse particles. The 950 × 550 mm pallet size determines how many blocks fit on each curing rack and whether your existing forklift can handle a loaded rack without overloading the mast. The PLC with frequency converter controls both the vibration ramp and the hydraulic sequence, and its display language must match your operators before the line arrives on site — a detail that delays commissioning more often than any mechanical issue. Double-sided sync gears on the mould lifting mechanism keep the mould box level during extraction, reducing the uneven block heights that cause pallet jams downstream. Schneider electrical components are specified so that replacement contactors and relays are available through local distributors in most markets rather than requiring an air-freight order from the manufacturer [NEED_CITE: international availability of standard industrial electrical components].
The Cost of Skipping the Line-Level View
Purchasing a press without specifying the mixer capacity, conveyor length, and stacking method leads to a plant where the fastest machine is always waiting on the slowest station. Buyers who skip the pallet specification often discover that their curing racks accept a different size, forcing a full re-order of pallets before the first production run. Voltage and frequency left unconfirmed until after shipment can delay commissioning by weeks while a transformer or motor swap is arranged [NEED_CITE: common commissioning delays due to voltage mismatch in exported machinery]. These are not engineering problems — they are specification gaps that a complete block line and supporting equipment proposal is designed to close before any steel is cut.
Why Source the Complete Line Here
The QT4-18 is not quoted as a standalone press; mixer output, conveyor transfer rate, and stacking capacity are calculated together against your target block format. Mould design covers the formats your market actually sells, and custom drawings are available when your buyers need a dimension outside the standard range. Automation level is selectable, so you can begin with manual pallet recycling and add the stacker and trolley when volume justifies the investment. Installation support includes foundation drawings that show mixer, conveyor, and press placement so your contractor pours concrete once and gets it right. The spares list — hydraulic seals, vibration motor brushes, and mould wear plates — is built into the proposal before you ask, because a plant sitting idle while waiting for an air-freighted part is a cost no quotation should create.
Documentation & Verification
- Line layout drawing showing mixer, conveyor, press, and stacking zone dimensions for your site
- Capacity calculation sheet stating which block format the molding cycle assumes
- Pallet specification matched to your curing rack dimensions and forklift load rating
- Hydraulic and electrical schematic with component part numbers for local sourcing
- Voltage, frequency, and PLC display language confirmation form signed before production
- Factory test record on your specified block format before container loading
Installation, Commissioning & Support
- Foundation drawing with cement pouring requirements for the 27.5 kW total power load
- Electrical connection plan confirming voltage and dedicated circuit for the PLC and frequency converter
- Assembly sequence from mixer through stacker per the site-specific layout drawing
- First-run parameter setting for vibration force and hydraulic pressure matched to your mix design
- Operator training covering mould change procedure using the double-sided sync gear mechanism
- Spare wear parts list including mould liners, hydraulic seals, and conveyor belt sections
What We Need to Size Your Line
To configure a concrete block production line around your actual production conditions, we need your target block formats with dimensions, the daily volume you plan to run, and the raw materials available locally including aggregate type and grading. Your site voltage and frequency, preferred PLC display language, and existing forklift capacity help us match the pallet and control specification before the line enters production.
Frequently Asked Questions
Q: How is the line capacity calculated, and which block format does the 18–25 s molding cycle assume?
A: The molding cycle depends on the block format being produced — a 400 mm hollow block requires a different cycle than a thin paving block. Our capacity calculation sheet names the exact block format, dimensions, and mix design assumed so your daily output projection is based on a confirmed number, not a catalogue generalization.
Q: What is the total footprint required for the complete line from mixer through to stacking area?
A: The QT4-18 press occupies 2500 × 1750 mm, but the full line footprint includes the JQ500 mixer, the 8 m or 6 m belt conveyor, block conveyor run, stacker zone, and pallet return path. We provide a site-specific layout drawing with all station positions so your contractor can prepare the foundation before equipment arrives.
Q: How do the mixer batch time, conveyor transfer rate, and press cycle synchronize to prevent idle time?
A: The JQ500 mixer batch size and the belt conveyor feed rate are calculated against the QT4-18 molding cycle so that mixed material reaches the hopper before each press stroke completes. If any station runs faster or slower than the others, the press sits idle — the line is balanced as one system to prevent that.
Q: Is the pallet size 950 × 550 mm compatible with my existing curing racks and forklift?
A: Pallet dimensions must match your curing rack spacing and your forklift tine width and load capacity. We confirm these details during the proposal stage and adjust pallet specifications if your existing infrastructure requires a different size, avoiding a costly pallet re-order after delivery.
Q: What foundation preparation and cement pouring is required before installation?
A: Each station — mixer, conveyor supports, press, and stacker — has specific load points that require a level concrete pad of defined thickness. The foundation drawing included in your documentation package shows exact dimensions, anchor bolt positions, and curing requirements so your contractor can complete all civil work before the line ships.