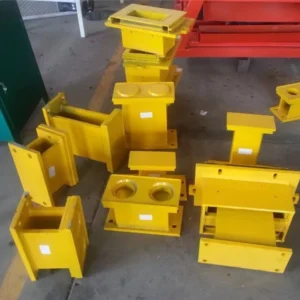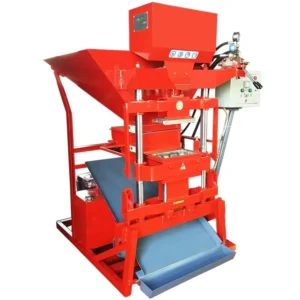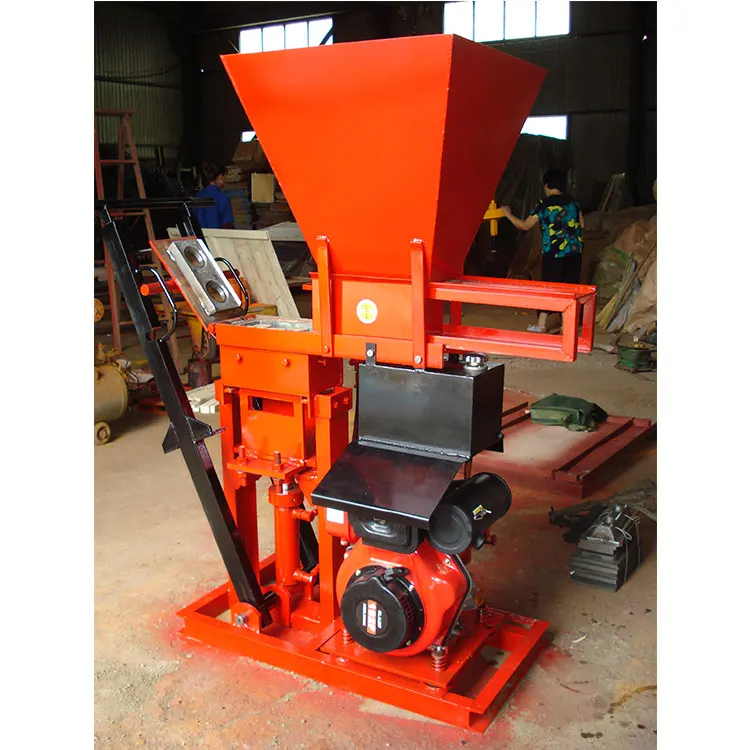
Line-Sized Equipment — Soil preparation, mixing, and curing stations matched to the 15–20 second press cycle so the Interlocking Brick Making Machine production line never waits on a bottleneck.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Interlocking Brick Making Machine |
| Dimension | 1200 × 800 × 1750 mm |
| Total Mass | 500 kg |
| Engine Option | Electric or Diesel |
| Molding Cycle | 15–20 s |
| Daily Capacity | 1,600 pcs per 8-hour shift (basis not stated in source — confirm block format, material, and thickness) |
| Brick Compressive Strength | >16 MPa |
| Basic Line Equipment | Soil crusher, soil screen, 6 m conveyor belt, JQ350 mixer |
| Compatible Raw Materials | Cement, sand, soil, fly ash, lime |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site housing project block production | Local soil blended with cement and lime |
| Environmental construction walls and partitions | Fly ash and sand interlocking bricks |
| First-plant entrepreneur setups | Crusher-screened soil with cement stabilisation |
| Contractor self-supply for rural infrastructure | Diesel-powered line using site-excavated earth |
Why the Mixer and Conveyor Decide Your Real Daily Output
A press cycling every 15–20 seconds is useless when upstream material arrives every 40 seconds.
I once stood in a workshop where an interlocking brick line was rated for solid throughput on paper, yet pallets of half-cured bricks were stacked on the floor because the mixer loop was slower than the press cycle. The Interlocking Brick Making Machine production line only delivers its stated output when soil crushing, screening, conveying, and mixing are timed to feed the press without gaps [NEED_CITE: line balancing principles in small-scale block plants]. A bottleneck at any upstream station turns a coordinated system into an expensive single machine with idle operators.
Matching the Upstream Loop to the Press Cycle
The JQ350 mixer must complete a batch within the window the press consumes the previous one. When the soil crusher and 6 m conveyor deliver material at a steady rate, the mixer never starves and the press never idles. Configuring the Interlocking Brick Making Machine production line around this sequence prevents the pile-up that quietly erodes daily throughput.
Curing and Handling Often Get Left Off the Drawing
Pallets, stacking, and curing space are sometimes excluded from quotations, leaving fresh bricks to be moved by hand [NEED_CITE: common omissions in small brick line quotations]. When curing racks and covering materials are planned alongside the press footprint, the line sustains its cycle through the entire shift rather than slowing once floor space fills with green bricks.
What the Specs Actually Mean on the Floor
The 15–20 second molding cycle sets the rhythm every other station must follow. Hydraulic pressure applied during this window compresses the soil-cement mix to densities that yield strengths exceeding 16 MPa after static curing. Choosing between the electric and diesel engine option depends on site grid reliability — a diesel-driven line keeps producing during load-shedding without waiting for a generator connection. The 1,200 × 800 × 1,750 mm press footprint and 500 kg mass keep the unit mobile enough for site relocation, yet the line still needs level ground for the conveyor and mixer to align correctly. Soil particle size from the crusher and screen directly affects mix consistency, which in turn determines whether the press produces uniform blocks or rejects.
The Hidden Cost of Sizing Only the Press
When buyers focus quotation discussions on the press alone, upstream and downstream mismatches surface after installation. A mixer that takes longer than the molding cycle forces operators to skip presses, cutting output without any mechanical fault. Undersized curing areas mean bricks are stacked before gaining enough green strength, leading to edge damage [NEED_CITE: green strength requirements for soil-cement interlocking bricks]. These issues show up as missed delivery dates rather than machine alarms.
Why Source the Full Line Together
Specifying soil preparation, mixing, pressing, and curing as one system means cycle times are checked against each other before the equipment ships. The basic line package — crusher, screen, conveyor, and JQ350 mixer — is matched to the press cycle rather than assembled from unrelated catalogue items. Pallet dimensions are chosen with the buyer’s existing curing racks in mind. Voltage and control language are confirmed before production so commissioning starts on day one. Mould options are discussed against the block formats the local market actually buys. Installation guidance covers the entire line footprint, not just the press foundation.
Documentation & Verification
- Line layout drawing showing station spacing and material flow direction for your site
- Capacity calculation stating the exact block format and material mix assumed
- Machine specification sheet with matched JQ350 mixer and 6 m conveyor ratings
- Voltage, frequency, and control language confirmation record before dispatch
- Factory test run video on your specified raw material blend
- Operation and maintenance manual covering press, mixer, and crusher servicing
Installation, Commissioning & Support
- Level foundation required across the full 6 m conveyor run and press footprint
- Dedicated circuit sized to the electric engine option or fuel storage for diesel
- Press arrives partially assembled; mixer and conveyor bolt on at site
- First-run parameter setting covers cycle timing between JQ350 mixer and press
- Operator training includes mould change and soil-cement mix ratio adjustment
- Wear parts list for crusher hammers, screen mesh, and press hydraulic seals
What to Share With Your Inquiry
Send the block format and dimensions your market demands, the soil or fly ash type available on site, and your local voltage and frequency. Note whether grid power is reliable or a diesel line is preferable. Including your curing area dimensions helps size pallet quantity and stacking layout.
Frequently Asked Questions
Q: What block format is the 1,600 pieces per day capacity based on?
A: The source does not state which interlocking brick size, material blend, or wall thickness that figure assumes. We calculate realistic daily output only after confirming your target block dimensions and raw material, then state the capacity per format so you can compare against your project schedule.
Q: How do the soil crusher and JQ350 mixer cycle times match the 15–20 second press?
A: The crusher and 6 m conveyor deliver screened soil to the JQ350 mixer at a rate calculated to complete each batch before the press finishes its current cycle. If your soil is heavier or more clay-rich, we adjust screen mesh size and mixer speed during commissioning to keep the loop balanced.
Q: What curing area and covering materials do I need for daily output?
A: Fresh interlocking bricks need covered curing space sized for at least several days of production stacked on pallets. We specify pallet count and rack layout based on your site area so bricks reach full strength without edge damage from premature handling.
Q: How do I match pallet size to my existing curing space and forklift?
A: Pallet dimensions are chosen to fit both the press platen and your forklift tine spacing. We confirm your curing rack width and aisle clearance before ordering so pallets slot straight into your existing layout without cutting or re-racking.
Q: Which engine type should I specify for my site conditions?
A: The electric engine suits sites with stable grid supply and three-phase power. The diesel option keeps production running where outages are frequent or no grid connection exists. We confirm voltage, frequency, and fuel availability before finalising the configuration.