
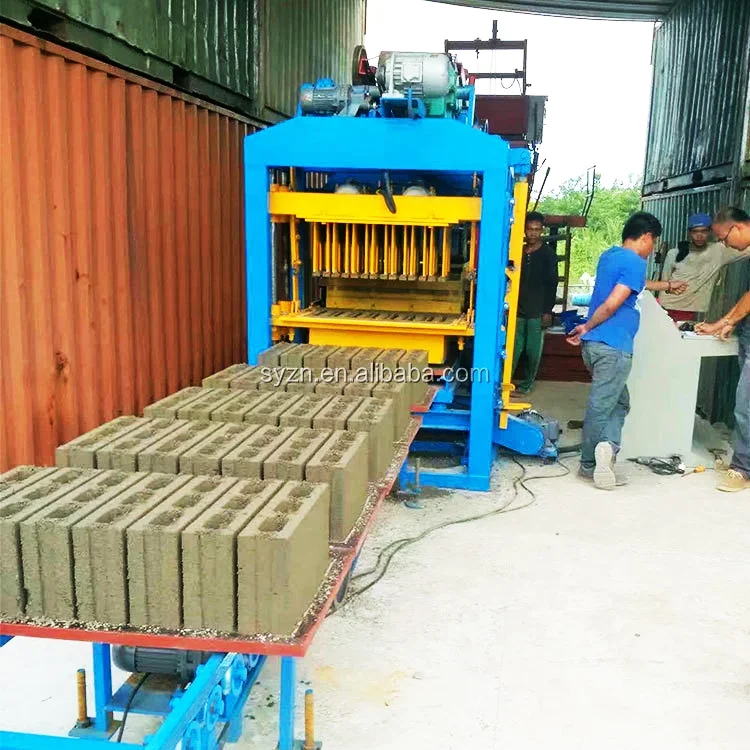
Coordinated Line Pacing — the QTJ4-25 block machine production line balances mixer feed rate, pallet circulation, and press cycle so no station waits on another.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Model | QTJ4-25 |
| Overall Dimensions (L×W×H) | 3060×1730×2580 mm |
| Total Mass | 4 T |
| Main Vibration Form | Platform Vibration |
| Vibration Force | 45.5 kN |
| Vibration Frequency | 4200 r/min |
| Rated Pressure | 16–21 MPa |
| Pallet Size | 850×550 mm |
| Molding Cycle | 25–30 s (basis not stated in source — confirm block format / material / thickness) |
| Overall Power | 14.9 kW |
| Demolding Method | Vibration |
| Factory Area Required | 200 m² |
| Stacking Method | Manual |
| Automation Level | Semi-Automatic |
| Warranty | 1 year (whole machine, excluding spare parts) |
| Loading | 1×40HQ container (for basic equipment) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Crushed stone, sand, cement, fly ash |
| Solid block manufacturing | Gravel, slag, cement blends |
| Paver and interlocking brick | Fine aggregate with colored pigment |
| Curbstone forming | High-density concrete mix with coarse aggregate |
| On-site project block production | Locally sourced sand, dust, and gravel |
Why "Cycles per Hour" Misses the Real Output Picture
A cycle time only becomes daily output once every upstream and downstream station matches its rhythm.
Buyers reviewing the QTJ4-25 block machine production line often see the 25–30 second molding cycle and calculate an hourly figure — then discover on site that the mixer empties faster than it refills, or that pallet return slows the press to a halt. [NEED_CITE: common causes of block line throughput loss in semi-automatic plants] The gap between quoted cycle time and actual shift output is almost always a line-balance problem, not a press problem. When the pallet feeding station cannot deliver a fresh board before the press finishes its vibration sequence, the operator stands idle and the theoretical output drops with every missed beat.
How Each Station Connects Around the Press
The QTJ4-25 block machine production line places the press at the center of a material loop that begins with raw material batching and ends with wet blocks leaving the curing rack. The mixer must deliver a fresh batch to the hopper within the same window the press takes to complete one vibration and demolding sequence. If the mixer is undersized, the press waits; if the conveyor is too narrow, material bridges in the hopper and the cycle stalls mid-press.
Pallet circulation is the second loop. With an 850×550 mm pallet, each board carries a set number of cavities depending on the mould in use. The return conveyor must move empty pallets back to the feed end before the press completes its next cycle. Manual pallet handling is specified for this configuration, which means the operator’s pace directly sets the line tempo.
Where the QTJ4-25 Block Machine Production Line Fits in Your Plant Layout
A factory area of 200 m² covers the press, mixer, and pallet return loop but leaves limited margin for curing racks and raw material stockpiles. [NEED_CITE: typical block plant floor space allocation for semi-automatic lines] Contractors setting up on a housing project site need to map pallet staging, wet-block curing lanes, and aggregate storage before the equipment arrives. The 4 T machine mass requires a level concrete pad with anchor points, and the 14.9 kW total power draw must be confirmed against the site transformer capacity before the container is dispatched.
Reading the Vibration and Pressure Numbers
The 45.5 kN vibration force at 4200 r/min works with the 16–21 MPa rated pressure to compact the mix inside the mould cavity. Platform vibration transmits energy through the pallet rather than the mould walls, which means the 850×550 mm pallet must be rigid enough to transfer that force without absorbing it. If the pallet material is too soft or warped, vibration energy dissipates before reaching the mix, and block density becomes inconsistent from one cycle to the next. The 25–30 second molding cycle is achievable only when aggregate gradation, cement ratio, and moisture content match the vibration profile — a coarser mix may need a longer cycle, while a fine sand blend may compact faster but risks cracking during demolding.
What Happens When Line Stations Are Mismatched
When the mixer capacity exceeds what the press can consume, wet mix sits in the hopper and begins to set, creating blockouts in the feed chute. [NEED_CITE: block machine hopper blockage causes in hot climates] On the downstream side, if curing rack space runs out before the shift ends, the operator has nowhere to place fresh blocks and the press must stop regardless of its mechanical readiness. These are not press failures — they are line-design oversights that show up only after installation, when the cost of adding a second mixer or extending the curing area has already multiplied.
Why Buyers Choose This Line Configuration
The machine, mould, pallet, and handling equipment are specified as a matched set rather than assembled from separate suppliers, so pallet dimensions and mould cavity counts align from day one. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default. Moulds are designed for the formats the buyer’s market actually sells, including custom drawings when standard cavity layouts do not fit. The semi-automatic level allows a buyer to start with manual pallet handling and add automation later as volume grows. Installation support includes operator training so the crew understands cycle-time dependencies before the first production run.
Documentation & Verification
- Line layout drawing showing mixer, press, and pallet return positions with dimensions
- Capacity calculation sheet stating block format assumed for each output figure
- Pallet specification confirming size, material, and required inventory count
- Hydraulic and electrical schematic with voltage and frequency marked
- Factory test record on buyer’s target block format before dispatch
- Operation and maintenance manual with mould change procedure
Installation, Commissioning & Support
- Level concrete pad with anchor bolts sized for the 4 T machine mass
- Dedicated power circuit matching confirmed voltage and frequency for the 14.9 kW load
- Pallet return conveyor alignment checked against 850×550 mm pallet travel path
- First-run parameter setting for vibration force and pressure matched to buyer’s mix
- Operator training on manual pallet handling rhythm and mould change sequence
- Wear parts list with reorder intervals for vibration springs and hydraulic seals
What to Prepare Before Requesting a Quote
Share the block formats your market sells along with daily volume targets so the line can be sized around those formats rather than a generic cycle figure. Confirm local voltage, frequency, and the control panel language your operators read. [NEED_CITE: electrical standard differences across export markets] Provide the dimensions of your existing curing area and forklift capacity so pallet size and rack layout can be matched before the quotation is finalized.
Frequently Asked Questions
Q: How is daily output calculated for the QTJ4-25 across different block formats?
A: Each block format uses a different number of cavities per pallet, so the same 25–30 second cycle produces different piece counts depending on whether the mould is set for hollow blocks, solid blocks, or pavers. The line quotation should include a capacity table that lists output per format, not a single cycles-per-hour figure. Upstream mixer and pallet feed rates must match whichever format produces the highest material demand.
Q: What pallet inventory does the full line require?
A: The 850×550 mm pallet size determines how many boards are needed to keep the press running while earlier blocks cure. Total pallet count depends on curing time and rack capacity. The line proposal should confirm pallet material, quantity, and whether existing racks accommodate these dimensions before the order is placed.
Q: How do I confirm electrical specifications before shipment?
A: Voltage, frequency, and control panel language must be locked in during the quotation stage. The electrical schematic in the documentation package shows the exact wiring configuration. Confirming these details before production avoids commissioning delays when the container arrives on site.
Q: What mixing capacity prevents the press from starving between cycles?
A: The mixer must deliver a fresh batch within the same window the press takes to complete one molding cycle. Mixer drum volume, conveyor belt width, and raw material feed rate all factor into this calculation. The line layout document should show the mixer-to-press material flow rate matched to the target block format.
Q: Which supporting equipment is included and which is the buyer’s scope?
A: The quotation covers the press, mould, pallets, and the handling equipment specified in the line layout. Items such as curing racks, yard forklifts, and raw material stockpile structures typically remain the buyer’s scope. The proposal document lists every included and excluded item to prevent gaps during installation.



