
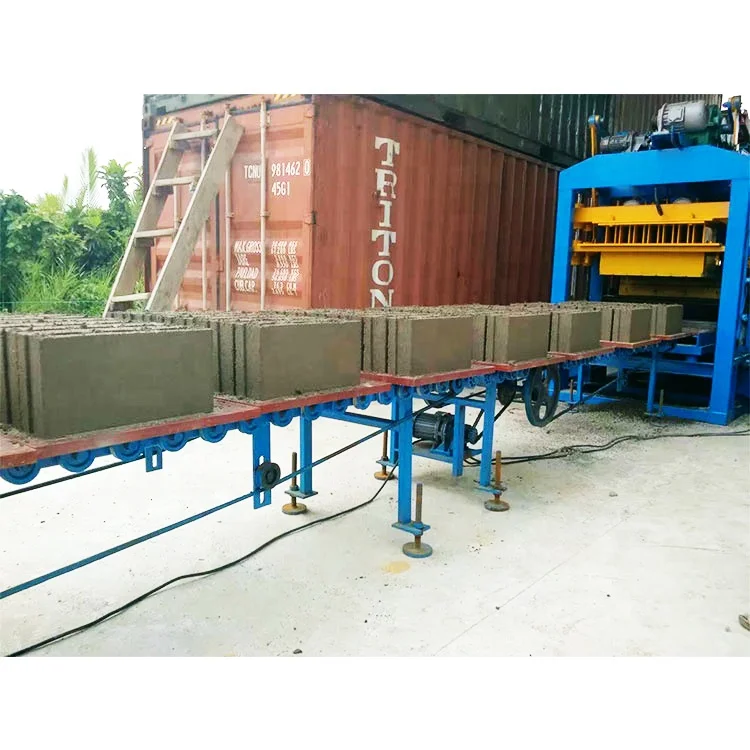
Matched System Integration — The QTJ4-25 is configured as a complete line where mixer discharge rate, pallet return speed, and press cycle are balanced so no station sits idle between forming and curing.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QTJ4-25 |
| Product Type | Semi-Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 6400×1500×2700 mm |
| Molding Cycle | 25 s (basis not stated in source — confirm block format / material / thickness) |
| Vibration Frequency | 2800–5100 r/min |
| Vibration Force (Exciting Power) | 60 kN |
| Total Power | 17.9 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×20 mm |
| Net Weight | 2500 kg |
| Applied Products | Concrete hollow blocks (8 inch, 6 inch), solid bricks |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Output Capacity (Hollow Block 390×190×190 mm) | 4 pcs/mould, 480 pcs/h, 3800 pcs/8hr |
| Output Capacity (Hollow Block 400×150×200 mm) | 5 pcs/mould, 600 pcs/h, 4800 pcs/8hr |
| Output Capacity (Solid Brick 240×115×53 mm) | 18 pcs/mould, 2100 pcs/h, 17000 pcs/8hr |
| Automation Level | Semi-automatic |
| Hydraulic System | Equipped (hydraulic station for stable pressure) |
| Vibration Type | Bed mould vertical vibration + upper mould compression vibration |
| Voltage & Frequency | Not stated in source — confirm before order |
| Control System / PLC | Not stated in source — confirm before order |
| Mould Change Time | Not stated in source — confirm with supplier |
| Stacking Method | Manual (stack by hand, move with trolley) |
Application Suitability
| Application | Material or Output |
|---|---|
| Small to medium block production plants | Hollow blocks and solid bricks from crushed stone, sand, cement, fly ash |
| On-site block production for construction contractors | 8 inch and 6 inch hollow blocks using locally available aggregates |
| Entrepreneurs setting up a first block plant | Solid bricks and interlock blocks with semi-automatic operation and manual stacking |
| Concrete product manufacturers adding formats | Pavers, kerbstones, and porous bricks through custom mould design |
What "25 Seconds Per Cycle" Actually Means for Your Daily Output
A cycle time only holds if the mixer can deliver fresh material and the pallet can clear the press before the next stroke begins.
When I walked onto a site where a similar semi-automatic press was running, the operator was spending half the shift waiting. The JQ350 mixer discharge was slower than the press demand, and pallets were piling up at the stacking end because no trolley route had been planned. The quoted block production line equipment capacity assumed a rhythm that the surrounding stations could not sustain. This is where block line supporting equipment decisions — pallet quantity, trolley path, mixer positioning — determine whether the line runs at its rated pace or loses hours to idle gaps [NEED_CITE: typical material flow bottlenecks in semi-automatic block plants].
How the Mixer and Press Cycle Must Align
The JQ350 mixer paired with this press is not a catalogue default — it is selected so that the batch discharge rate matches the hopper demand across a 25-second molding window. If the mixer is undersized, the press waits for material and the effective output drops well below the rated figure. Block production line equipment only performs when the upstream feed rate is verified against the press cycle and the specific block format being run.
Pallet Flow and the Hidden Stacking Bottleneck
Pallets measuring 850×550×20 mm leave the press loaded with wet blocks and must travel to the curing area, be stripped, and return before the next cycle completes. Without enough pallets in circulation or a clear trolley route, the press stops. Block line supporting equipment planning must account for pallet quantity relative to curing area size and the distance between the press and the stacking zone [NEED_CITE: pallet circulation ratios for semi-automatic block operations].
Reading the Specifications Beyond the Catalogue
The vibration system combines bed mould vertical vibration with upper mould compression vibration, which compacts the mix from both directions to produce consistent block density across the mould face. The 60 kN exciting power working within the 2800–5100 r/min frequency range is what determines wall thickness uniformity and compressive strength for hollow blocks. The hydraulic station adds stable forming pressure throughout each stroke, preventing density variation that would appear as weak corners or crumbling edges. A 17.9 kW total power draw across the press, mixer, and hydraulic station defines the electrical circuit requirement — this must be confirmed against site supply before the machine is built. The pallet size of 850×550×20 mm should be checked against the curing rack spacing and the trolley or forklift already on site, because a mismatch means either the pallets do not fit the racks or the handling equipment cannot carry them efficiently.
The Cost of Skipping Line Integration Checks
A buyer who confirms the press alone without specifying pallet quantity, trolley count, or mixer discharge timing will discover the gap on the first production day. Pallets run short by mid-shift, blocks stack unevenly because the curing area was never dimensioned to the pallet footprint, and the operator manually shuttles material between stations. The daily throughput then reflects the weakest link, not the press rating [NEED_CITE: consequences of incomplete block line specification at order stage].
Why Source the Full Line From One Supplier
Block machinery as a single focus means the press, mould, pallet, and handling are specified as one matched system — the JQ350 mixer is paired to this specific press cycle, not selected independently. Configuration is set against the buyer’s actual mix design and local aggregate, so the 60 kN vibration force is validated for the material being used rather than a catalogue default. Mould design covers the formats the buyer’s market sells, with custom drawings available for non-standard interlock or paver shapes. The automation level is selectable, allowing a buyer to start with semi-automatic operation and manual stacking, then add automatic pallet feeding later without replacing the press. Installation and commissioning include operator training on the specific block format and mould change procedure, so the line runs at pace from the first shift.
Documentation & Verification
- Line layout showing mixer, press, and pallet return positions with station distances
- Capacity calculation stating the block format assumed for each output figure
- Pallet specification matched to curing area dimensions and trolley type
- Hydraulic and electrical schematic with voltage and frequency confirmed per site
- Mould drawing and format list provided with quotation before production
Installation, Commissioning & Support
- Foundation pad sized to 6400×1500 mm footprint with level tolerance for vibration stability
- Dedicated electrical circuit rated for 17.9 kW total draw with voltage confirmed before shipment
- Machine arrives with hydraulic station pre-assembled; pallet feeder and trolley route laid out on site
- First production run supervised with mould change procedure and cycle timing verified per block format
- Operator training covers mix loading sequence, vibration frequency adjustment, and manual stacking workflow
- Wear parts list and mould maintenance schedule provided with initial spare pallets recommended
What to Include in Your First Enquiry
Provide the block format and daily output target so the line layout can be dimensioned around the QTJ4-25 cycle. Confirm your local raw material sources — aggregate type, sand grading, cement availability — so the mixer and vibration settings are matched to your mix. State your site voltage and frequency, curing area dimensions, and whether you need pallets and trolleys included in the block production line equipment scope.
Frequently Asked Questions
Q: How is daily output calculated, and which block format does each figure assume?
A: Each output figure in the specification table is tied to a specific block dimension — for example, 3800 pieces per 8-hour shift assumes the 390×190×190 mm hollow block at 4 pieces per mould. These figures also assume the mixer and pallet return can sustain the 25-second cycle without interruption. Confirm your target format so we calculate the realistic daily throughput for your line.
Q: Which stations are included in the block line supporting equipment quotation?
A: The standard line quotation covers the QTJ4-25 press, JQ350 mixer, pallet specification, and hydraulic station. Pallet quantity, trolley, curing racks, and stacking tools are added based on your curing area layout. Confirming these items at enquiry stage prevents gaps that would leave output stacked by hand on the first day.
Q: How do cycle times between the mixer, press, and pallet return need to match?
A: The JQ350 mixer must discharge a full batch before the press hopper runs empty, and the loaded pallet must clear the mould area before the next cycle starts. If the pallet return distance or trolley capacity creates a delay, the press idles and actual output falls below the rated cycle. Line layout planning addresses this before equipment is shipped.
Q: What pallet material and quantity is recommended for the curing area?
A: The 850×550×20 mm pallet must be ordered in sufficient quantity to cover the press output for one full curing cycle plus return time. Bamboo, PVC, or steel pallet options are available depending on block weight and local climate. The pallet material choice also affects how blocks release during stripping and how the surface finish appears.



