
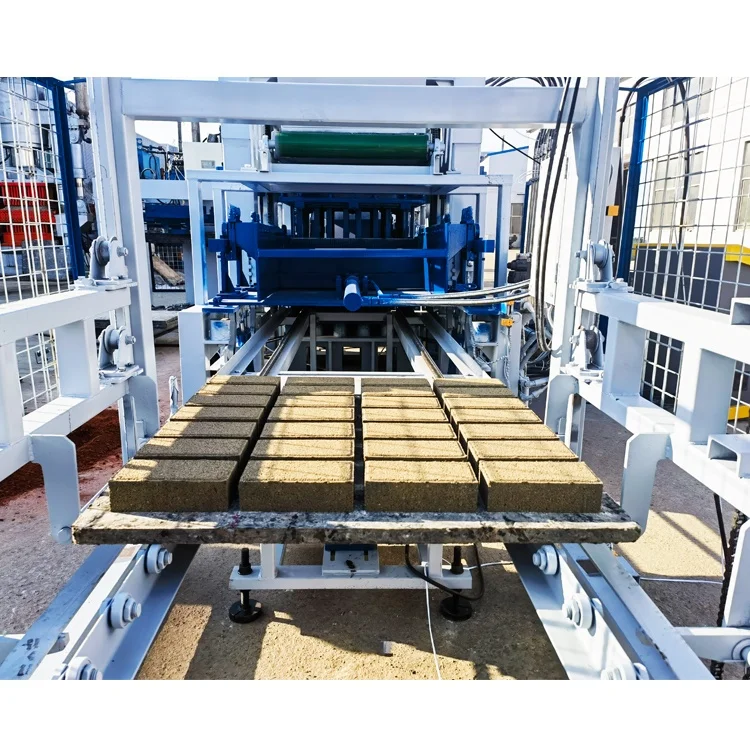
Matched line engineering — every station from mixer to cubing is sized to the QT612 press cycle so the bottleneck stays where you planned it.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT612 |
| Product Type | Hydraulic Block Making Machine |
| Overall Dimensions (L×W×H) | 7350 × 1780 × 2950 mm |
| Rated Pressure | 16 MPa |
| Main Vibration | Platform vibration |
| Vibration Frequency | 4600 r/min |
| Pallet Size | 880 × 700 mm |
| Molding Cycle | 15–20 s |
| Overall Power | 30.5 kW |
| Voltage & Frequency | Configurable to site supply (basis to be confirmed) |
| Control System | PLC or manual (basis to be confirmed) |
| Output — Hollow Block 400×200×200 mm | 6 pcs/mould, 1080 pcs/h, 8640 pcs/day |
| Output — Porous Brick 240×115×90 mm | 14 pcs/mould, 2800 pcs/h, 22400 pcs/day |
| Output — Standard Brick 240×115×53 mm | 30 pcs/mould, 6800 pcs/h, 54400 pcs/day |
| Raw Materials | Crushed stone, sand, cement, fly ash, slag, cinder, gangue, gravel, perlite, industrial wastes |
| Automation Level | Automatic |
| Standards | CE, SGS, ISO 9001 |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production plants | Crushed stone and cement mixes for 400×200×200 mm structural blocks |
| Porous and standard brick lines | Sand, fly ash and cement blends for 240×115×90 mm and 240×115×53 mm formats |
| Paving stone and kerbstone yards | Aggregate-rich face-mix designs for landscaping and municipal contracts |
| Interlocking and slope block projects | Site-specific industrial waste blends including slag and gangue |
| On-site construction supply | Multi-format runs for buildings, roads, squares and garden infrastructure |
What "1080 Pieces per Hour" Leaves Out on a QT612 Block Making Machine Production Line
Cycle rate on the press means nothing if the pallet return loop and stacker cannot keep up.
A quoted cycles-per-hour figure almost always assumes a single block format under ideal conditions. In the field I have watched lines stall because the mixer discharge cycle was longer than the press mould cycle, or because the pallet return conveyor could not feed fast enough during a switch from hollow blocks to pavers. The daily throughput then drops well below what the buyer budgeted for, and the conversation turns to warranty claims instead of production planning [NEED_CITE: block plant cycle time balancing principles].
How Station Cycle Times Are Balanced Around the Press
The QT612 block making machine production line starts with the press cycle of 15–20 seconds and works backward through every upstream and downstream station. The mixer batch size and discharge rate are set so that a full charge of material reaches the hopper before the press completes its current cycle. The pallet feeder must place a fresh pallet on the table within the same window, and the stacker must clear the finished product before the next cycle begins. When any one of these intervals drifts, the press sits idle and the quoted capacity becomes theoretical.
Where Pallet Handling Becomes the Real Constraint
Pallet size at 880 × 700 mm governs how many blocks sit on each board, how many boards fit in the curing rack, and whether the buyer’s existing forklift can load the racks without a second pass. I have seen lines where the pallet dimension was chosen from a catalogue rather than the curing area layout, forcing the plant to buy a different forklift before the first week of production ended [NEED_CITE: pallet and curing rack dimension matching in block plants]. Confirming pallet material and thickness against the buyer’s rack spacing avoids this surprise.
Reading the Numbers Behind 16 MPa and 4600 r/min
The rated hydraulic pressure of 16 MPa and platform vibration at 4600 r/min work together to compact the mix into a dense, consistent block. Pressure alone crushes the aggregate; vibration alone rearranges particles without full interlock. Both forces must match the buyer’s mix design — a sand-rich blend needs different vibration energy than a crushed-stone or fly-ash blend. The 30.5 kW overall power covers the press itself; total line draw depends on the mixer motor, conveyor drives and stacker hydraulics selected during layout, so the incoming supply capacity must be calculated for the whole system, not the press alone.
The Cost of Skipping Line-Level Engineering
Leaving pallet return, stacking and curing out of the quotation looks cheaper on paper but transfers labour cost and floor space problems to the buyer. Operators hand-stack output, pallets pile up between the press and the curing yard, and block strength varies because the curing timeline is uncontrolled. Over a production year these hidden costs show up as inconsistent block quality, overtime wages and replacement pallets bought in a hurry [NEED_CITE: hidden costs of incomplete block production lines].
Why Procure the Full Line Here
Block machinery is our single focus, so the QT612 press, moulds, pallets and handling equipment are specified as one matched system. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, including custom drawings when a project requires a non-standard kerbstone or interlocking profile. Automation level is selectable, allowing a plant to start semi-automatic and add stacking or cubing later. Installation support includes operator training on the specific line layout delivered to site.
Documentation & Verification
- Line layout drawing with capacity calculation stated per block format
- Machine specification sheet covering press, mixer, pallet feeder and stacker
- Mould drawing and format list matched to buyer’s product range
- Pallet specification confirmed against curing rack and forklift dimensions
- Voltage, frequency and PLC display language confirmation before production
- Factory test record showing cycle time on buyer’s chosen block format
Installation, Commissioning & Support
- Foundation plan sized to the 7350 × 1780 mm press footprint and vibration load
- Dedicated electrical circuit sized for 30.5 kW press plus full line auxiliary load
- Dismantling and container loading plan prepared before shipment
- On-site commissioning with cycle timing verified on buyer’s first block format
- Operator training covering mould change, pallet handling and PLC interface
- Wear parts and mould list supplied with first replacement lead times stated
Preparing Your Line Inquiry
Send us the block formats you sell today and the ones you plan to add, along with your target daily output per format. Include the raw materials available locally and a sample mix design if you have one. Confirm the site voltage, frequency and the language you need on the PLC display so the QT612 block making machine production line arrives ready to commission without delay.
Frequently Asked Questions
Q: How is daily output calculated for the QT612 line, and which block format does each figure assume?
A: Output figures are stated per format: 8640 pieces per day assumes 400×200×200 mm hollow blocks at 6 per mould, while 22400 per day assumes 240×115×90 mm porous bricks at 14 per mould. Each number is based on the stated moulding cycle of 15–20 seconds and assumes the full line — mixer, pallet feeder, stacker — keeps pace with the press.
Q: Which supporting stations are included in the line quotation, and where are they optional?
A: The standard quotation covers the press, pallet feeder, raw material mixer and conveyor. Automatic stacking, curing rack handling and cubing are configurable based on the buyer’s automation level and budget. Every optional station is listed separately so the buyer sees exactly where manual labour is replaced by equipment.
Q: How is pallet size and material selected to match my existing curing area and forklift?
A: The 880 × 700 mm pallet is a starting point. We confirm rack shelf spacing and forklift tine width with the buyer before production so the pallets fit without modification. Material and thickness are chosen to withstand the vibration cycle and the weight of wet blocks through the curing period.
Q: What voltage, frequency and PLC language options are available, and when must they be confirmed?
A: Voltage and frequency are configurable to the buyer’s site supply. PLC display language is agreed during the configuration stage. Both must be confirmed in writing before production begins so the electrical cabinet and control software are ready for immediate commissioning on arrival.
Q: How is the line cycle time balanced across stations so the press is not left waiting?
A: The 15–20 second moulding cycle sets the pace. Mixer batch size, conveyor speed, pallet feeder stroke and stacker lift rate are all calculated to complete their action within that window. The line layout drawing shows the timing for each station so the buyer can verify the balance before equipment is built.



