
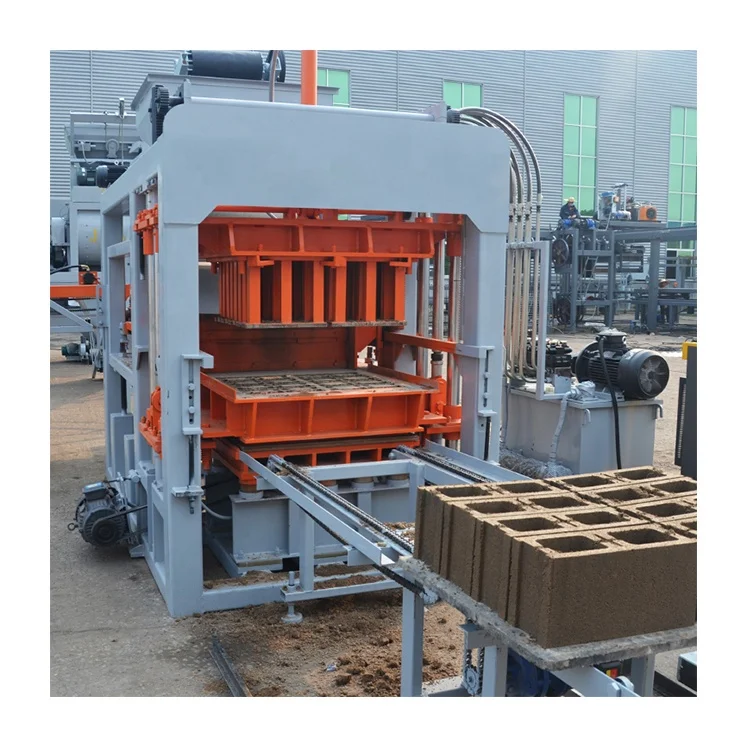
Matched Line Configuration — The QT6-15 block production line equipment is specified so the mixer output, pallet feed rate and conveyor speed all align with the 15-25 second press cycle, preventing upstream or downstream bottlenecks.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Fully Automatic Hydraulic Vibration Block Making Machine |
| Overall Dimensions (L×W×H) | 7400×1900×2660 mm |
| Molding Cycle | 15-25 s |
| Vibration Frequency | 4600 r/min |
| Exciting Power (Vibration Force) | 40-50 kN |
| Rated Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850×550×25 mm |
| Total Weight | 7 T |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Control System | PLC control system |
| Hydraulic Station | Included (high pressure, stable operation) |
| Included Auxiliary Equipment | Hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Output Capacity (Hollow block 400×200×200 mm) | 1200-1680 pcs/hr (basis: 15-20 s cycle) |
| Output Capacity (Hollow block 400×150×200 mm) | 1800-2400 pcs/hr (basis: 15-20 s cycle) |
| Output Capacity (Solid brick 240×115×53 mm) | 3240 pcs/hr (basis: 15-20 s cycle) |
| Daily Output (8 hr, Hollow block 400×200×200 mm) | 9600-13440 pcs/8 hr |
| Daily Output (8 hr, Solid brick 240×115×53 mm) | 16200-19440 pcs/8 hr |
| Voltage & Frequency | Configurable (confirm with buyer’s local supply) |
| PLC Display Language | Configurable (confirm before commissioning) |
Application Suitability
| Application | Material or Output |
|---|---|
| Commercial block plant | Hollow blocks (400×200×200 mm and 400×150×200 mm) from crushed stone, sand and cement |
| Municipal paving supply | Interlocking pavers and curbstones from aggregate and fly ash mixes |
| Housing project on-site production | Solid bricks (240×115×53 mm) for local masonry demand |
| Concrete product manufacturer | Format switching between hollow block, solid brick and paver on a single line |
Why the Mixer and Pallet Feeder Decide Your Real Daily Output
A press rated at 15-25 seconds per cycle only achieves that tempo when every surrounding station keeps pace.
Quotations that list only the main machine often leave the buyer to source the mixer, pallet feeder and conveyor separately. When those components arrive with mismatched cycle times, the press sits idle waiting for the next pallet or for mixed material to drop. I have seen turnkey block making line installations where the mixer discharged slower than the press could consume, cutting actual daily output in half during the first weeks of operation [NEED_CITE: synchronization of mixer discharge and press cycle in concrete block lines]. The QT6-15 block production line equipment addresses this by pairing the JQ350 mixer, pallet feeder, brick conveyor and block sweeper as one sequenced system under the PLC, so no station starves or overflows the next.
How Stations Connect Around the Press
The press cycle sets the heartbeat of the line. Every upstream and downstream station must complete its task within that 15-25 second window. The pallet feeder pushes a fresh pallet into position while the press is still closing the mould; the brick conveyor accepts the finished layer the moment the press head lifts. If any station lags, the PLC holds the press in a safe idle state rather than risking a jam.
Sequencing Logic That Prevents Bottlenecks
The PLC control system monitors pallet position, mould clamp status and conveyor readiness before authorising each press stroke. This interlock logic means the turnkey block making line does not rely on operator timing. Even during a shift change or a brief material refill pause, the sequence resumes without manual reset, keeping the block production line equipment running at its verified cycle rate.
Reading the Specs That Actually Matter
Vibration force and hydraulic pressure work together to compact the mix. The QT6-15 delivers 40-50 kN of exciting power at 4600 r/min, which is matched to the mould cavity volume for hollow blocks and solid bricks. The 850×550×25 mm pallet size determines how many blocks are pressed per cycle and must align with the curing rack dimensions and the forklift capacity already on site. Rated power of 31.25 kW covers the press, hydraulic station and conveyor motors together, so the electrical supply must be sized for the full line, not just the main machine.
What Happens When Line Stations Are Mismatched
When the pallet feeder runs slower than the press cycle, the press waits. When the conveyor cannot clear finished blocks fast enough, the sweeper jams against the next layer. These micro-stoppages accumulate across an eight-hour shift. I have watched plants lose significant portions of their rated daily output because nobody calculated the conveyor belt speed against the press discharge rate before the equipment was shipped [NEED_CITE: impact of conveyor speed mismatch on block plant daily throughput].
Why Procure the Full Line From One Source
Block machinery is our single focus, so the QT6-15 is never shipped as a standalone press. The mixer, pallet feeder, conveyor and sweeper are specified as one matched set, with cycle times verified together at the factory. Configuration is set against the buyer’s actual mix design and local aggregate rather than a catalogue default. Voltage, frequency and PLC display language are confirmed before production, preventing commissioning delays on arrival. Line layout drawings show every station footprint so foundation work is completed before the container arrives.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for each output figure
- Machine specification sheet covering press, hydraulic station, pallet feeder and conveyor
- Hydraulic and electrical schematic for local maintenance planning
- Voltage, frequency and PLC display language confirmation record before production
- Factory test record showing cycle times verified with all stations connected
Installation, Commissioning & Support
- Foundation plan drawn around the 7400×1900×2660 mm press footprint and pallet feeder reach
- Dedicated electrical circuit sized for the 31.25 kW total line load at the confirmed voltage
- On-site assembly of pallet feeder, conveyor and sweeper aligned to the press discharge height
- PLC parameter tuning to match the buyer’s mix design and target block format
- Operator training covering mould change sequence, daily greasing points and PLC alarm response
- Wear parts list covering hydraulic seals, vibration springs and pallet feeder guide rollers
What to Share With Your Inquiry
To size the turnkey block making line correctly, provide the target block formats, expected daily volume, and the raw materials available locally including aggregate gradation. Confirm the site voltage, frequency and preferred PLC display language. If an existing curing area or forklift is already in place, share those dimensions so the 850×550 mm pallet specification can be cross-checked before the order is finalised.
Frequently Asked Questions
Q: How is the output capacity verified, and which block format is each figure based on?
A: Every capacity figure on the QT6-15 data sheet states the block format and cycle time it assumes. The 1200-1680 pieces per hour figure, for example, is based on a 400×200×200 mm hollow block at a 15-20 second cycle. Daily output is then calculated over an eight-hour shift with the same format assumption carried through.
Q: How do upstream and downstream stations match the press cycle time?
A: The JQ350 mixer discharge rate, pallet feeder stroke speed and brick conveyor belt velocity are each calculated against the 15-25 second press window. The PLC interlocks all stations so the press only fires when every upstream and downstream position is confirmed ready.
Q: What voltage, frequency and PLC language are configured for the target market?
A: These are confirmed with the buyer before production begins. The electrical cabinet is built to the site supply specification, and the PLC display is loaded with the operator’s preferred language so commissioning proceeds without translation delays on arrival.
Q: Which raw materials and mix designs has this line been configured for?
A: The QT6-15 handles crushed stone, sand, cement, dust and fly ash mixes. Before the line is built, the buyer’s local aggregate sample and target block strength are reviewed so vibration force and hydraulic pressure settings are matched to the actual material rather than a generic default.
Q: What installation, commissioning and operator training support is included?
A: The block production line equipment is shipped with a foundation drawing, assembly sequence and PLC parameter file. On-site support covers station alignment, cycle verification with the buyer’s mix, and operator training on mould change, daily maintenance and PLC alarm response [NEED_CITE: standard commissioning scope for automatic block production lines].



