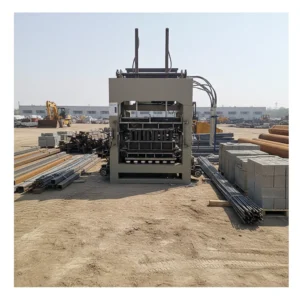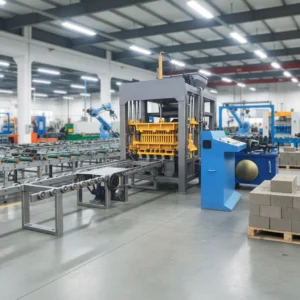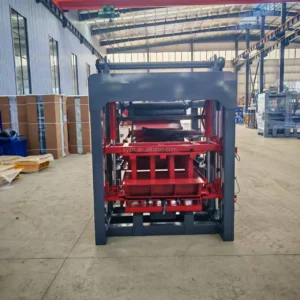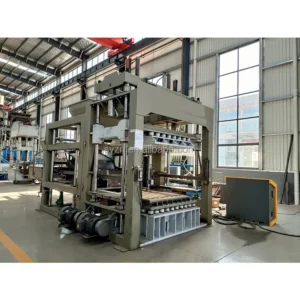
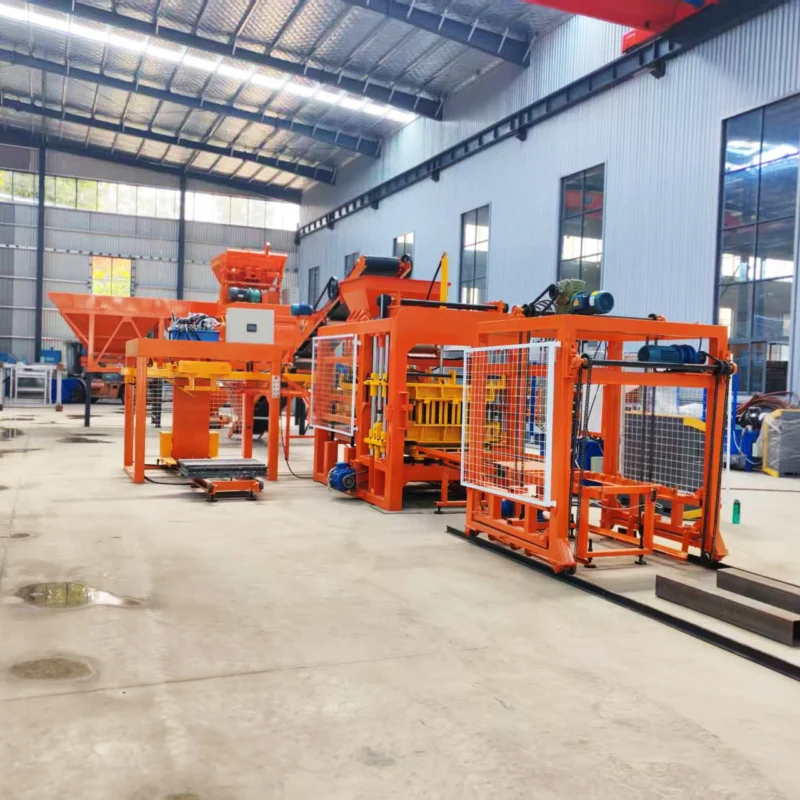
Matched System Engineering — the QT6-15 block making machinery, mixer, pallet feeder, and stacker are specified together so cycle times align across every station.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Full Automatic Hydraulic Block Making Machine |
| Model | QT6-15 |
| Overall Dimension | 820017002950mm |
| Total Mass | 7T |
| Overall Power | 37KW |
| Vibration Frequency | 0-60HZ |
| Vibration Form | Platform Vibration |
| Vibration Force | 45KN |
| Moulding Mode | Load automatically, vibration moulding |
| Molding Cycle | 15-20s |
| Demolding Method | Hydraulic |
| Pallet Size | 880*850mm |
| Control System | PLC (Programmable Controller) with touch screen |
| Hydraulic System | Independent integrated type hydraulic station |
| Output Capacity (Hollow block 400x200x200mm) | 1080-1440 pcs/hour (basis: 6 pcs/mould, 15-20s cycle) |
| Output Capacity (Hollow block 400x150x200mm) | 1440-1920 pcs/hour (basis: 8 pcs/mould, 15-20s cycle) |
| Output Capacity (Solid brick 240x115x53mm) | 5760-7680 pcs/hour (basis: 32 pcs/mould, 15-20s cycle) |
| Output Capacity (Rectangular brick 200x100x60mm) | 2160-2880 pcs/hour (basis: 21 pcs/mould, 20-25s cycle) |
| Output Capacity (Zigzag brick 225×112.5x60mm) | 2160-2880 pcs/hour (basis: 15 pcs/mould, 20-25s cycle) |
| Block Compressive Strength | More than 15 MPa |
| Factory Area | 1200m2 |
| Raw Material Adaptability | Waste ash, slag, cement, various aggregates |
| Certification | CE declaration where applicable |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production | Cement, crushed stone, sand, and waste ash blends |
| Solid brick production | Fly ash, slag, and fine aggregate mixes |
| Paving brick production | Coarse aggregate with cement binder for high-density pavers |
| Interlocking brick production | Graded aggregates with controlled moisture content |
| Building material plant setup | Full product range from structural blocks to decorative pavers |
What "Rated Output per Hour" Leaves Out When Stations Fall Out of Sync
A block press only produces when every upstream and downstream station keeps pace with its cycle.
I once worked on a line where the host machine was a QT6-15 capable of a 15-20 second molding cycle, but the pan mixer feeding it needed nearly two minutes per batch. The press sat idle almost half the shift, and daily output dropped to a fraction of the nameplate figure. The buyer had compared host machine prices across three suppliers without ever asking how fast the mixer could deliver concrete to the hopper [NEED_CITE: common causes of block plant underperformance in emerging markets]. An automatic block making machine production line only reaches its stated capacity when raw material feeding, mixing, pallet circulation, and stacking are all timed to the press rhythm.
Stations That Must Keep Time With the Press
The QT6-15 completes a molding cycle in 15-20 seconds, which means the mixer must deliver a fresh batch to the hopper within that window, the pallet feeder must index a new board into position, and the stacker must clear cured product from the exit conveyor. If any one of these stations runs slower, the press waits. In a matched automatic block making machine production line, each station’s cycle is calculated against the target block format and the specific pallet size of 880*850mm so that no single bottleneck drags the entire line down.
Where Line Configuration Decides Real Daily Output
A buyer planning a complete block production setup needs to see capacity stated per format, not just per press cycle. The QT6-15 produces 6 hollow blocks of 400x200x200mm per mould at 1080-1440 pieces per hour on a 15-20 second cycle, but switch to a solid brick mould holding 32 pieces and the raw material demand changes entirely. The mixer, belt conveyor, and cement silo must all be re-checked for that higher throughput. This is why a line layout and capacity calculation should state the assumed block format for every output figure [NEED_CITE: block plant capacity calculation methodology per format].
How Platform Vibration and Hydraulic Pressure Work Together on the Pallet
The QT6-15 uses platform vibration with an adjustable frequency range of 0-60HZ and a vibration force rated at 45KN, combined with an independent integrated hydraulic station for demolding. Platform vibration transmits energy through the pallet board into the concrete mass, compacting aggregate from the bottom upward. Hydraulic pressure then locks the compacted material into shape before the mould lifts. If the pallet material is too soft, vibration energy dissipates into the board rather than the concrete, producing blocks with lower compressive strength. The 880*850mm pallet size must therefore be paired with boards stiff enough to transfer the full 45KN force into the mix while still fitting the buyer’s existing curing racks and forklift tines.
Reading the Specs That Matter Beyond the Host Machine
Overall power of 37KW covers the press motor, vibration system, and hydraulic pump together. When the full automatic block making machine production line adds a mixer, pallet return conveyor, and stacker, the total connected load rises substantially. The independent hydraulic station sits apart from the main frame, which keeps hydraulic oil away from vibration-induced contamination and extends seal life. The PLC touch screen controls not only the press cycle but can also integrate signals from the pallet feeder and stacker, so a single operator monitors the entire line from one interface rather than walking between stations.
The Cost of Treating Supporting Equipment as an Afterthought
When pallet handling and stacking are left out of the quotation, blocks come off the press and pile up at the end of the conveyor. Workers then carry them by hand to the curing area, which introduces breakage, slows the press operator who must wait for cleared space, and turns a theoretically automatic line into a manual operation at its most labour-intensive point. Pallet size chosen without checking the buyer’s forklift capacity or curing rack dimensions means boards either do not fit the racks or require a new forklift purchase before the first block is produced [NEED_CITE: hidden costs of incomplete block line quotations]. These mismatches surface on commissioning day, when delays and rework cost far more than specifying the right supporting equipment upfront would have.
Why Sourcing the Full Line From One Configuration Point Matters
Block machinery as a single focus means the QT6-15 host machine, moulds, 880*850mm pallets, and handling equipment are specified as one matched system. Configuration is set against the buyer’s actual mix design and local aggregate, not a catalogue default, so the vibration frequency and hydraulic pressure are adjusted for the materials the buyer can actually source. Mould design covers the formats the buyer’s market sells, with custom drawings available for non-standard sizes. Automation level is selectable, so a buyer can start with semi-automatic pallet handling and add full automatic stacking later without replacing the press. Installation support includes operator training on the PLC interface, and wear parts lists cover both the press and the supporting stations.
Documentation & Verification
- Line layout with capacity calculation per block format and per station cycle time
- Machine specification sheet with hydraulic and electrical schematics for the 37KW system
- Pallet specification confirming 880*850mm size and board material stiffness rating
- Voltage, frequency, and PLC touch screen language confirmation before production
- Factory test record on the buyer’s target block format and mix design
- Mould drawing and format list with changeover procedure
Installation, Commissioning & Support
- Foundation plan matching the 8200*1700mm footprint and 1200m2 factory area requirement
- Dedicated power circuit sized for 37KW press plus upstream mixer and downstream stacker load
- Machine dismantled for container loading and reassembled on site with alignment checks
- PLC touch screen commissioned with the buyer’s confirmed language and voltage settings
- Operator training on mould change, pallet feeder adjustment, and fault diagnosis system
- Wear parts list covering hydraulic seals, vibration springs, and pallet boards
What to Prepare Before Requesting a Line Quotation
To receive a configuration that actually reaches its stated capacity, provide the target block formats and daily output goal, the local raw materials available with their grading and moisture range, the existing curing area dimensions and forklift specifications, and the site voltage and frequency. If you already operate a mixer or conveyor, share the make and capacity so the automatic block making machine production line can be configured around your existing equipment rather than duplicating it.
Frequently Asked Questions
Q: What supporting equipment is included beyond the QT6-15 press itself?
A: A complete line configuration covers the raw material batching and mixing station, belt conveyor to the press hopper, pallet feeder for the 880*850mm boards, exit conveyor, and stacking system. Each station is sized so its cycle time matches the 15-20 second press cycle, preventing idle time at any point.
Q: How do I verify that mixing and stacking keep pace with the press?
A: Request a line layout that lists cycle time per station against your target block format. The mixer batch size and discharge rate must deliver concrete within the molding cycle, and the stacker must clear cured boards before the next pallet arrives. Any mismatch shows up as idle seconds that accumulate across a shift.
Q: What pallet size and material should I specify for my curing setup?
A: The QT6-15 uses 880*850mm pallets. Board material and stiffness must transfer the 45KN vibration force into the concrete without absorbing energy. Confirm that this size fits your existing curing racks and forklift tines before ordering, or specify new racks matched to this dimension.
Q: Can I begin with semi-automatic handling and add automation later?
A: The QT6-15 platform supports selectable automation levels. You can start with manual pallet handling and add an automatic pallet feeder and stacker later. The PLC control system accommodates the upgrade path, so the press itself does not need replacement when supporting stations are automated.