
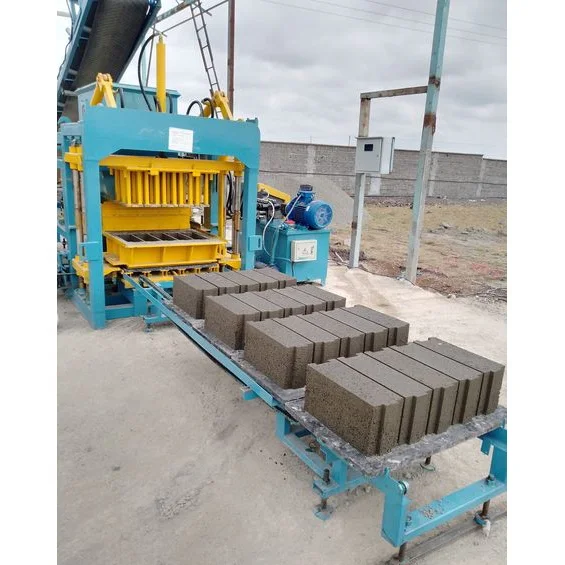
Matched Line Balance — press, pallet feeder, conveyor and PLC tuned to the same 15–25 s moulding cycle so the QT4-15A never idles waiting for the next station.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Hydraulic Block Making Machine |
| Model | QT4-15A |
| Overall Dimensions (L×W×H) | 7100 × 1600 × 2610 mm |
| Molding Cycle | 15–25 s (basis not stated in source — confirm block format and material) |
| Vibration Frequency | 4600 r/min |
| Vibration Force | 40–50 kN |
| Total Power | 18.45 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 550 × 25 mm |
| Net Weight | 3 T |
| Control System | PLC control system |
| Hydraulic Station | Included (high pressure, stable operation) |
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Free Accessories | Manual hydraulic trolley, spare parts and tools |
| Output Capacity | Hollow block 400×200×200 mm: 408 pcs/h, 3264 pcs/8 hr |
| Output Capacity | Hollow block 400×150×200 mm: 510 pcs/h, 4080 pcs/8 hr |
| Output Capacity | Solid brick 240×115×53 mm: 2100 pcs/h, 17000 pcs/8 hr |
| Automation Level | Semi-automatic (with pallet feeder and conveyor) |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site housing project block production | Hollow blocks from crushed stone, sand and cement at project-defined daily volumes |
| Paver and curbstone supply for municipal works | Pavers and curbstones from fly ash and sand with format changes on the same press |
| First block plant for a regional distributor | Solid bricks and hollow blocks from locally sourced aggregate blends |
| Format expansion for an existing concrete product manufacturer | Additional block sizes using the same QT4-15A press with mould swaps |
Why the "Per-Hour" Figure Rarely Survives the First Shift
A press quoted alone tells you what the mould can do, not what the line will deliver.
In my years running block lines across the Middle East, the most common argument on a new plant floor is about output that never materialised. The hydraulic block making machine production line might be rated at several hundred pieces per hour on paper, but when the pallet feeder lags or the mixer cannot keep up with the press cycle, the actual tally drops sharply. Buyers sign off on a number tied to a specific block format and then discover their daily mix and pallet handling were never part of the calculation [NEED_CITE: typical output shortfalls when supporting equipment is undersized].
Stations That Keep the Same Beat
The QT4-15A is supplied with a pallet feeder and brick conveyor specified alongside the press, not added as an afterthought. When every station shares the same 15–25 s moulding cycle target, pallets arrive before the press finishes its stroke, and finished blocks clear the table before the next cycle begins. This is what separates a hydraulic block making machine production line that runs from one that stutters.
Where the Mixer Fits in the Chain
The JQ350 mixer ships as part of the configuration, sized to feed the press without forcing the operator to slow the cycle. A mixer that empties too slowly turns the QT4-15A into a waiting machine. Matching mixer discharge rate to press demand is a line-level decision, not a press-level one, and it is resolved before the equipment leaves the factory [NEED_CITE: mixer-to-press throughput matching principles].
Reading the Numbers Behind the Output
Vibration force of 40–50 kN at 4600 r/min works together with the hydraulic station to compact the mix into a dense block. Higher vibration alone will not compensate for weak hydraulic pressure, and pressure alone will not consolidate a dry mix without sufficient vibration. The QT4-15A pairs both so that hollow blocks, solid bricks, pavers and curbstones each reach the density the market expects. Pallet size of 850 × 550 × 25 mm must match the curing rack spacing and the forklift already on site; a mismatch here means rearranging the entire curing yard after arrival. The PLC control system manages cycle timing and can be confirmed for voltage, frequency and display language before production, avoiding commissioning delays that I have seen stall projects for weeks.
What Happens When Pallet Handling Is Left to Chance
When a quotation covers only the press, someone ends up moving pallets by hand and stacking blocks on the floor. The semi-automatic configuration of the QT4-15A removes that bottleneck by including the pallet feeder and conveyor, but if the buyer’s curing area was never measured against the 850 × 550 mm pallet, the forklift cannot turn between racks and output piles up at the end of the conveyor. That backlog then forces the operator to stop the press — exactly the idle time the line was designed to eliminate [NEED_CITE: curing yard layout impact on block plant throughput].
Why Buyers Source the Whole Line from One Supplier
Block machinery is the single focus here, so the press, mould, pallet and handling equipment are specified as one matched system rather than assembled from separate vendors. Configuration is set against the buyer’s actual mix design and target block format, not a catalogue default. Moulds are designed for the formats the buyer’s market actually sells, including custom drawings when a standard mould does not fit. The automation level starts at semi-automatic with the pallet feeder and conveyor, leaving room to add stacking or cubing later. Installation, commissioning and operator training are included so the first production run is not left to guesswork.
Documentation & Verification
- Line layout showing pallet feeder, conveyor and press positions with cycle time alignment notes
- Capacity calculation sheet stating the block format and mix assumed for each output figure
- Hydraulic and electrical schematic for the QT4-15A so site electricians can prepare connections
- Pallet specification confirming 850 × 550 × 25 mm dimensions and material grade
- Factory test record run on the buyer’s requested block format before dispatch
- Voltage, frequency and PLC display language confirmation document signed before production
Installation, Commissioning & Support
- Foundation pad sized to the 7100 × 1600 mm footprint with anchor bolt template provided
- Dedicated circuit rated for the 18.45 kW total power draw with voltage confirmed before shipment
- Pallet feeder and brick conveyor assembled and aligned to the QT4-15A press on site
- PLC control system parameters set to the buyer’s block format during commissioning
- Operator training covering mould change procedure, daily greasing points and hydraulic checks
- Wear parts list with mould and hydraulic seal reorder codes for the first year of operation
Before You Send the Inquiry
Tell us the block formats you sell today and the ones you plan to add, along with your target daily output for each. Share the aggregate and sand sources available locally so the mix can be matched before the mould is built. Confirm the voltage and frequency at your site, the PLC language your operators read, and whether your existing forklift and curing racks fit an 850 × 550 mm pallet.
Frequently Asked Questions
Q: How is the output capacity calculated, and which block format does each figure assume?
A: Each capacity figure on the QT4-15A is tied to a specific block size. The 408 pcs/h rate applies to 400×200×200 mm hollow blocks, the 510 pcs/h rate to 400×150×200 mm hollow blocks, and the 2100 pcs/h rate to 240×115×53 mm solid bricks, all based on an 8-hour shift. A different format or mix will shift these numbers, so the line layout document always states the assumed format.
Q: What supporting equipment is included so the line runs without manual pallet handling?
A: The QT4-15A hydraulic block making machine production line ships with a pallet feeder that loads pallets into the press automatically and a brick conveyor that carries finished blocks away. A block sweeper cleans pallets before they re-enter the feeder. Together these stations remove the need for an operator to move pallets by hand between cycles.
Q: How do pallet size and material affect curing area layout and forklift compatibility?
A: The 850 × 550 × 25 mm pallet defines the rack spacing in the curing yard and the fork dimensions of the lift truck. If racks are built for a different pallet, the yard must be rebuilt after arrival. Confirming pallet size against the existing curing area and forklift before production avoids that cost.
Q: What voltage, frequency and PLC language options are confirmed before shipment?
A: Voltage, frequency and the PLC display language are confirmed in writing before the QT4-15A enters production. This step ensures the electrical cabinet matches the buyer’s site supply and the operator interface reads in a language the crew understands, preventing commissioning delays.
Q: How are cycle times balanced across the press, pallet feeder and conveyor?
A: Every station on the QT4-15A line is set to the same 15–25 s moulding cycle target. The pallet feeder releases a pallet just before the press finishes its stroke, and the brick conveyor clears the finished block before the next cycle begins. This balance keeps the press running continuously rather than waiting on upstream or downstream stations.



