
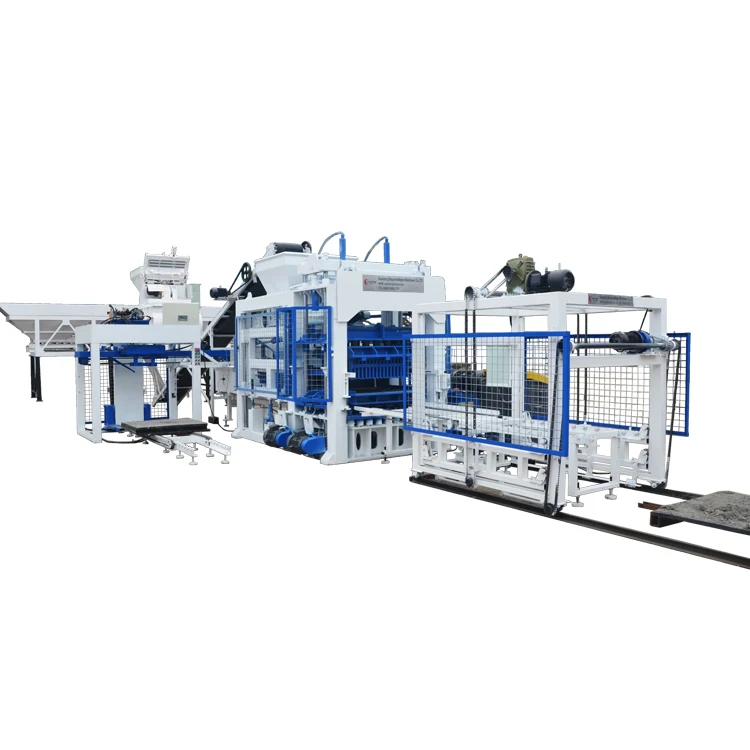
Matched System Configuration — The QT10-15 block making machine line coordinates press, pallet feed, conveyor and hydraulic station as one verified unit, eliminating the upstream and downstream bottlenecks that typically cut actual output on standalone machines.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT10-15 |
| Product Type | Hydraulic Concrete Block Making Machine |
| Control System | PLC control cabinet |
| Hydraulic System | Independent integrated hydraulic station |
| Vibration Mode | Vertical station mode resonance, automatic FM-AM |
| Component List | Pallet feed machine, block making machine, storage hopper, conveyor, hydraulic unit, PLC control cabinet |
| Output Capacity (Hollow Block) | 1,800–2,400 pcs/hour (basis: 400×200×200mm, 10 pcs/mould, 15–20s cycle) |
| Output Capacity (Solid Brick) | 8,928–11,160 pcs/hour (basis: 240×115×53mm, 62 pcs/mould, 15–20s cycle) |
| Output Capacity (Paving Block) | 5,184–6,480 pcs/hour (basis: 200×100×60mm, 27 pcs/mould, 20–25s cycle) |
| Cycle Time (Hollow Block) | 15–20s |
| Cycle Time (Paving Block) | 20–25s |
| Mould Change | Quick replacement supported |
| Daily Output (Hollow Block) | 14,400–19,200 pcs (basis: 8-hour shift, 400×200×200mm) |
| Daily Output (Solid Brick) | 71,424–89,280 pcs (basis: 8-hour shift, 240×115×53mm) |
| Automation Level | Automatic |
| Warranty | 1 year (excluding spare parts) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow Block Production | Crushed stone, cement, sand aggregate for 400×200×200mm structural blocks |
| Solid Brick Production | Dense concrete mix for 240×115×53mm standard building bricks |
| Paving Block Production | High-strength mix designs for 200×100×60mm interlocking pavers |
| Interlocking Brick Production | Specialized mould formats for dry-stack wall systems |
What "Automatic Line" Leaves Out of the Quotation
A press is only as productive as the slowest station feeding or clearing it.
Many quotations list the block making machine supporting equipment as optional or exclude it entirely, leaving the buyer to source pallets, mixers and conveyors locally. I have walked onto sites where a high-capacity press sat idle because the locally sourced pallet feeder could not match the press cycle, dropping actual daily output well below the quoted figure. The concrete block production line must be calculated as a single system where every station’s cycle time aligns [NEED_CITE: block line cycle synchronization principles]. When the pallet feed, material hopper and hydraulic unit are specified together and tested at the factory, the press runs continuously rather than waiting for upstream delays.
Line Synchronization Removes the Bottleneck
The QT10-15 operates as a complete production cell where the PLC control cabinet coordinates the pallet feed machine, storage hopper, conveyor and press cycle. This concrete block production line ensures that a fresh pallet arrives and the material hopper charges the mould box within the press cycle window, preventing the idle time that plagues lines assembled from separate suppliers. Each station’s timing is verified against the others during factory testing.
Hydraulic Isolation Sustains Output Over Long Shifts
The independent integrated hydraulic station sits apart from the main press frame, shielding hydraulic valves and pumps from the intense vibration and dust generated during block compaction. On a block making machine supporting equipment setup, hydraulic reliability directly determines whether the line maintains pressure through a full shift. Isolating the station extends component life and reduces the unplanned stops that erode daily output [NEED_CITE: hydraulic system protection in vibrating machinery].
Vibration Tuning Adapts to Mould Format
Vertical station mode resonance with automatic FM-AM adjustment means the vibration profile shifts when the operator changes moulds, matching the frequency and amplitude to the new block format. A hollow block mould requires a different vibration pattern than a dense paving block mould. Manual tuning introduces inconsistency; automatic adjustment keeps block density uniform across format changes on this concrete block production line.
Reading the Specs That Determine Real Output
Hydraulic pressure and vibration force work together to compact the mix into the mould. Insufficient pressure leaves blocks weak at the core; excessive vibration without matched pressure causes surface cracking. The cycle time of 15–20 seconds for hollow blocks and 20–25 seconds for paving blocks reflects the dwell time needed for proper compaction at this pressure class. Pallet size, while to be confirmed before order, must match both the mould footprint and the curing rack dimensions the buyer already has on site. The PLC control cabinet manages all station sequencing, and confirming the display language before production avoids commissioning delays once the line arrives. Quick mould replacement enables format switches within a single shift, giving the plant flexibility to produce hollow blocks in the morning and paving blocks in the afternoon without losing a full day to changeover.
The Hidden Cost of Mismatched Stations
When a buyer purchases the press alone and adds a locally sourced mixer or conveyor, the cycle times rarely align. The press completes a cycle and waits. Over an eight-hour shift, those idle seconds accumulate into thousands of lost blocks. I have seen lines where the pallet return speed could not keep up, forcing the operator to manually feed pallets and negating the automation the buyer paid for. Voltage mismatches discovered after arrival can stall commissioning for weeks while transformers are sourced locally [NEED_CITE: industrial voltage compatibility issues in export machinery]. These costs never appear on the original quotation but show up in the first month of production.
Why Source the Line as One Package
Block machinery is our single focus, so the QT10-15 arrives with machine, mould, pallet and handling specified as a matched system rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design, local aggregate and target block format, not a catalogue default. Mould design covers the formats the buyer’s market sells, with custom drawings available. The automation level is selectable, allowing a buyer to start with the standard pallet feed and conveyor, then add automatic stacking later. Installation support includes operator training so the line reaches its verified cycle time from the first week.
Documentation & Verification
- Line layout with capacity calculation stating block format assumed for each output figure
- Machine specification sheet covering hydraulic pressure, vibration force and pallet dimensions
- Mould drawing and format list confirming all block types the line can produce
- Voltage and PLC control language confirmation document signed before production
- Factory test record showing cycle time verified against target block format
Installation, Commissioning & Support
- Foundation plan specifying load points and curing pit layout for the QT10-15 footprint
- Dedicated power circuit sized to the confirmed rated power and local voltage
- Factory-dismantled station modules with reassembly sequence for on-site erection
- PLC parameter setting and cycle timing adjustment during first-week commissioning
- Operator training covering mould change procedure and daily maintenance checkpoints
- Wear parts list identifying hydraulic seals and vibration components for first reorder
Before You Request a Quote
To size this concrete block production line accurately, share your target block format and daily output requirement, the raw materials available locally including aggregate type and gradation, and your site’s voltage and frequency. Let us know whether you already have pallets, curing racks or a mixer on site so the quotation covers only what you need. If you plan to expand formats later, mention the full range so the mould plate and pallet dimensions accommodate future additions.
Frequently Asked Questions
Q: How do I verify that pallet feed, conveyor and press cycle times are matched?
A: Request the line layout document showing each station’s cycle time against the press cycle for your specific block format. The factory test record should confirm these timings were verified together, not tested as standalone machines. Any station slower than the press creates idle time that cuts actual output.
Q: What stations are included in the quotation, and which do I need to source separately?
A: The QT10-15 line includes the press, pallet feed machine, storage hopper, conveyor and hydraulic unit. Mixers, curing racks, stacking systems and forklifts are typically sourced by the buyer. Clarify your existing equipment before quotation so the line interfaces correctly with what you already have.
Q: How is the hydraulic station protected from vibration and dust?
A: The independent integrated hydraulic station is mounted separately from the main press frame, reducing exposure to compaction vibration and concrete dust. This isolation protects valves and pump seals over sustained production runs, maintaining pressure consistency and reducing unplanned maintenance stops.
Q: Can the line be upgraded to fully automatic stacking later?
A: Yes. The automation level is selectable, and the PLC control cabinet can integrate an automatic stacker added after initial installation. Plan the floor space and pallet return path for the future stacker during initial layout so the upgrade does not require repositioning the press or conveyor.
Q: When must voltage, frequency and PLC language be confirmed?
A: These must be confirmed before production begins. The PLC display language and electrical components are set during assembly, and changing them after arrival delays commissioning. Provide your site voltage and frequency, plus preferred operating language, at the quotation stage to avoid post-delivery modifications.



