
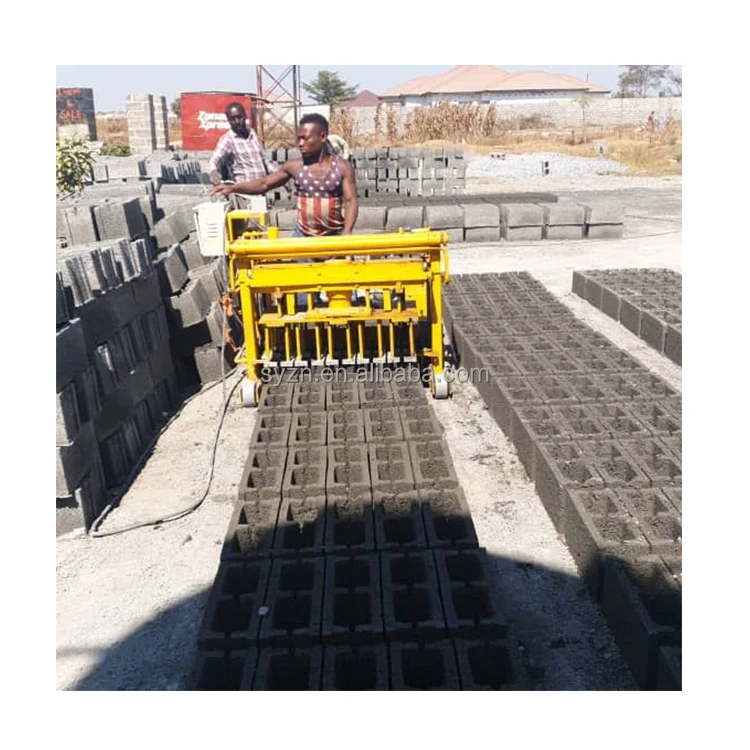
Line Balance Engineering — every station from mixer to curing area is sized against the 30-second molding cycle so the QMY4-30 press is never left waiting for material or space.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QMY4-30 |
| Product Type | Diesel Engine Mobile Block Making Machine |
| Overall Dimensions (L×W×H) | 1300 × 1500 × 1000 mm |
| Net Weight | 950–1000 kg |
| Vibration Method | Mold Vibration |
| Exciting Power | 28.6 kN |
| Excitation Frequency | 4500 r/min |
| Total Power | 5.95 kW |
| Molding Cycle | 30 seconds |
| Output Capacity | 3000 pcs/day (8 hours) (basis to be confirmed — block format unspecified) |
| Power Source Option | Diesel Engine |
| Voltage Option | 220V / 380V |
| Control System | Manual / Semi-automatic (handle-operated) |
| Assembly State | Mobile / Egg-laying |
| Stacking Method | Manual (egg-laying on ground, no pallet required) |
| Raw Material Compatibility | Concrete, sand, cement, fly ash, lime, gypsum, stone dust, construction waste, slag, mine tailings, river sand, coal gangue |
| Mould Format | Customizable to buyer drawings |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production at housing projects | Crushed stone, cement, sand |
| Remote-area brick making without grid power | Fly ash, lime, gypsum, slag |
| Small-scale startup block plant | River sand, cement, stone dust |
| Mining industrial zone block production | Mine tailings, coal gangue, cement |
| Coastal or desert construction site production | Local aggregate with cement binder |
Why the "3000 Pieces per Day" Figure Needs a Second Look
The cycle time is fixed; the block format is what changes the math.
Every mobile block machine quotation carries a headline output number. Buyers then arrive at the site, start producing, and discover the daily count falls short. The gap is almost always the block format assumed in that headline — a 400×200×200 mm hollow block takes the same cycle but occupies more material feed and curing area than a smaller solid brick. With the QMY4-30 mobile block making machine production line, the 30-second cycle is a constant. What varies is how many pieces each cycle yields for your chosen format, and how fast your mixer can replenish between presses [NEED_CITE: capacity calculation methodology for egg-laying block machines].
Planning the supporting stations around this machine starts with confirming the exact block dimension you intend to sell. Only then can mixer batch size, material feed rate, and curing ground area be sized correctly.
How Stations Connect Around an Egg-Laying Press
A Mobile Block Making Machine production line is only as fast as its slowest station. The QMY4-30 completes a press every 30 seconds. That means your mixer must deliver a fresh batch within that window, and the operator must move the machine to the next position before the next cycle begins. If the mixer is undersized, the press sits idle. If the curing ground is too small, finished blocks bottleneck the entire operation.
Each station — batching, mixing, mobile pressing, ground curing — must be planned as a linked sequence rather than independent purchases. The diesel engine option removes grid dependency, but the vibration motor and control circuit still require stable voltage [NEED_CITE: diesel-electric integration in mobile block presses]. Matching these stations prevents the common frustration of a press that could produce more but is starved by upstream or downstream constraints.
Curing Area Logistics That Match Daily Output
Egg-laying machines cure blocks directly on the ground, eliminating pallet costs but demanding significant flat area. The curing zone must accommodate one full day of output plus the curing duration before blocks can be moved. For a machine producing in the range of thousands of pieces per shift, this area grows quickly — especially with hollow blocks that require wider spacing to prevent contact damage during the initial set.
Ground condition matters as much as area. Soft or uneven ground causes blocks to settle unevenly, creating dimensional inconsistency across the batch. A compacted gravel base or a concrete apron is typically necessary, and this preparation should be included in the project scope before the machine arrives on site.
Vibration, Power, and Material Density Trade-Offs
The 28.6 kN exciting force and 4500 r/min excitation frequency work together to compact the mix inside the mold. Higher vibration frequency improves surface finish but requires a cohesive mix that does not segregate under rapid oscillation. The 5.95 kW total power must cover both the vibration motor and the diesel-driven hydraulic circuit simultaneously.
Mold vibration means the compaction energy is applied directly at the mold walls rather than through a separate table. This is effective for egg-laying operation because the ground itself becomes the forming base. The mix design — particularly water-cement ratio and fine aggregate proportion — must be adjusted to suit this vibration method [NEED_CITE: vibration method comparison for mobile block machines]. A mix optimized for table vibration may produce weak or cracked blocks when used in a mold-vibration system.
The Hidden Cost of Treating the Press as a Standalone Purchase
Buyers who purchase only the mobile press and source the mixer, material handling, and curing logistics separately often find cycle times that do not align. A mixer that delivers batches every 60 seconds forces the 30-second press to wait through every other cycle. Inadequate curing space means blocks are moved before reaching sufficient green strength, resulting in chipped corners and rejected pieces [NEED_CITE: block curing timeline and green strength thresholds].
These mismatches are not visible in a quotation that lists the press alone. They appear weeks after startup, when the operator is spending more time managing bottlenecks than producing. Specifying the line as a connected system — with each station’s capacity stated against the same block format — eliminates this class of problem before equipment is shipped.
What Makes This Supplier’s Line Approach Different
Block machinery is the sole focus of this manufacturing operation, which means the press, mold, and supporting equipment are specified as a matched system rather than assembled from unrelated suppliers. The mold is designed for the block format your market actually sells, including custom drawings when standard formats do not match local demand.
Configuration is set against your actual mix design and local aggregate, not a catalogue default. The automation level is selectable, allowing a buyer to begin with semi-automatic operation and plan upgrades as production volume justifies further investment. Installation support includes operator training so the team understands not just the press but how each station in the line interacts with the others.
Documentation & Verification
- Line layout showing mixer, press path, and curing area scaled to your block format
- Capacity calculation stating the block dimension assumed for the daily output figure
- Mold drawing and format list confirming cavity count per cycle
- Voltage and control language confirmation before production begins
- Factory test record on your specified raw material mix before dispatch
Installation, Commissioning & Support
- Ground preparation guidance for egg-laying operation across the required curing area
- Diesel engine and vibration motor circuit checked against your site voltage at 220V or 380V
- Machine positioned and first-cycle test run using your local aggregate mix
- Handle-operated control sequence training for each production step
- Mold change procedure demonstrated on your ordered format set
- Wear parts list provided with recommended first replacement intervals
What We Need to Quote Your Complete Line
Provide the block format dimensions you intend to produce, along with the daily output target for that specific format. Share the raw materials available locally and any existing mix design data. Confirm the voltage and frequency standard at your site, and whether diesel power is required for off-grid operation. If you have existing equipment such as mixers or loaders, include the model and capacity so the line can be balanced around them.
Frequently Asked Questions
Q: How is the 3000 pcs/day output verified, and which block format is it based on?
A: The output figure requires confirmation of block dimensions, as the same 30-second cycle produces different piece counts depending on mold cavity layout. A capacity calculation is prepared for each buyer, stating the exact block format and cavity count assumed. This prevents the common gap between quoted capacity and actual daily production.
Q: What supporting equipment is needed around the mobile press to form a complete line?
A: A mixer matched to the 30-second cycle, a material batching station for consistent feed, and sufficient cured ground area to hold one full shift of output. Each station’s throughput must align with the press speed so no station becomes a bottleneck during continuous operation.
Q: How does diesel engine power integrate with the vibration motor and control system?
A: The diesel engine drives the hydraulic and mechanical systems while supplying the electrical circuit for the vibration motor and control panel. Voltage stability is essential for consistent vibration frequency, so the generator or engine alternator must be sized to handle the 5.95 kW total load without fluctuation.
Q: What site area and ground conditions are required for egg-laying production?
A: The curing area must accommodate daily output with adequate spacing between blocks. Ground should be compacted and level — a gravel base or concrete apron is recommended. Soft or uneven ground causes blocks to settle during initial curing, leading to dimensional inconsistency across the batch.



