
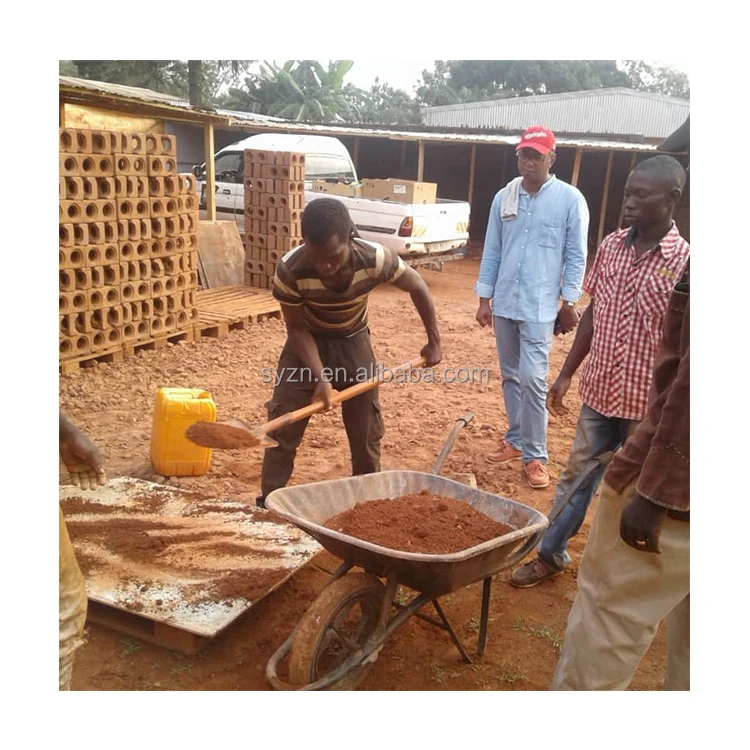
Complete Line Rhythm — Matching the 10-second press cycle to upstream feeding and downstream pallet handling so the machine never sits idle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | LY2-10 |
| Product Type | Clay Interlocking Block Making Machine |
| Machine Power | 7.5 kW |
| Molding Cycle | 10 seconds |
| Output Capacity | 6000 pcs/8hours (basis not stated in source — confirm block format / material / thickness) |
| Mould Format Options | 300×150×100mm, 250×125×75mm, 230×220×115mm (1 pc/mould) |
| Raw Material Compatibility | Clay, soil, earth, mud, concrete, cement, fly ash |
| Overall Dimensions (L×W×H) | 1300×1800×2400 mm |
| Automation Level | Semi-automatic |
Application Suitability
| Application | Material or Output |
|---|---|
| Small-scale interlocking brick plants | Clay, soil, and cement mixes for local building supply |
| Sidewalk and pathway paving projects | Interlocking formats using local earth or fly ash blends |
| On-site contractor production | Mud and concrete blocks for housing developments |
| Home business block manufacturing | Semi-automatic operation for limited-footprint workshops |
What a 10-Second Cycle Actually Demands From the Rest of the Line
The press is only as fast as the slowest station feeding it or clearing its output.
A clay block machine production line running a 10-second moulding cycle sounds straightforward on paper. But when the mixer batch cannot discharge fast enough, or the pallet feeding station jams on warped boards, the press spends half the shift waiting. I have stood on sites where the operator was manually shoveling material into the hopper because the upstream screw feeder was sized for a slower machine entirely [NEED_CITE: line synchronization principles for block making equipment]. The bottleneck simply moved from the press to the material feed, and daily output dropped well below what the cycle time suggested.
Sizing the Mixer and Feed System to the Press
The LY2-10 cycles every 10 seconds across its listed interlocking formats, which means the upstream mixer must deliver a consistent batch at intervals that match this rhythm. For clay and soil mixes, the moisture content and plasticity vary throughout the day, so the feeding system must handle material that ranges from free-flowing to sticky. A pan mixer paired with a belt conveyor typically provides the steady discharge rate needed, whereas a batch mixer that dumps its entire load at once can overwhelm the hopper. The clay block machine production line only reaches its intended rhythm when each station is timed against the press, not against its own maximum capacity.
Pallet Handling and the Downstream Bottleneck
Once the block is pressed, it sits on a pallet that must be moved to the curing area before the next cycle begins. With a 10-second cycle, a pallet leaves the press station every few seconds during active production. If the pallet return system is manual or undersized, pallets pile up at the discharge end, and the operator must stop the press to clear the backlog. Matching the pallet size to both the mould footprint and the buyer’s existing forklift and curing rack dimensions prevents this. The semi-automatic configuration of the LY2-10 means pallet handling is partly operator-dependent, making the layout of the curing area and the distance to the stacking point critical variables [NEED_CITE: pallet circulation requirements for semi-automatic block lines].
Reading the Specifications Against Your Actual Mix
The 7.5 kW motor drives both vibration and hydraulic pressure, but the effective forming force depends entirely on the mix design being used. A dry concrete mix with coarse aggregate requires different vibration amplitude and pressure settings than a wet clay blend. The three listed mould formats — 300×150×100mm, 250×125×75mm, and 230×220×115mm — each present a different filling depth and compaction challenge. A thinner 75mm format may cycle cleanly at 10 seconds, while the 115mm format might need a longer vibration dwell to achieve adequate density. These adjustments happen at the control panel, but only if the buyer has communicated the local aggregate characteristics before the machine is configured. The overall dimensions of 1300×1800×2400mm also define the physical envelope within which pallet feed and block discharge must operate, influencing how closely supporting equipment can be positioned.
When Line Stations Are Specified in Isolation
Purchasing the press from one supplier and the mixer, pallet system, and stacking equipment from others often leads to mismatched cycle times. The press waits for material, or the conveyor runs empty between batches. On interlocking formats where block geometry requires careful pallet placement, a misaligned pallet feeder causes the mould to close on an offset board, damaging both the mould and the pallet. These issues do not appear in any single supplier’s quotation because each station works perfectly on its own [NEED_CITE: equipment integration challenges in multi-supplier block plants].
Why Sourcing the Line Together Matters
Specifying the press, moulds, pallets, and handling equipment as one system means every station is configured against the same cycle time and block format. The raw material feed is matched to the buyer’s local clay or cement mix rather than a generic default. Pallet size and material are chosen with the buyer’s curing area and forklift in mind. Mould design covers the interlocking formats the buyer’s market actually demands. The automation level is selectable, allowing a semi-automatic start with a defined path to add automatic stacking later. Installation includes operator training on the complete line, not just the press in isolation.
Documentation & Verification
- Line layout drawing showing station spacing and pallet flow path for the LY2-10 footprint
- Capacity calculation sheet stating which interlocking format the output figure assumes
- Mould drawing and format list covering all three listed block dimensions
- Pallet specification matched to mould size and buyer’s curing rack configuration
- Factory test record run on the buyer’s specified raw material blend before dispatch
- Voltage and control language confirmation document signed off before shipment
Installation, Commissioning & Support
- Foundation plan accounting for the 1300×1800×2400mm footprint and vibration isolation requirements
- Electrical connection schedule for the 7.5kW motor with dedicated circuit and correct voltage configuration
- Assembly sequence for semi-automatic stations including pallet feed alignment to the mould
- First-run commissioning with vibration and pressure settings adjusted to the buyer’s local mix
- Operator training covering mould change procedure across all three interlocking formats
- Wear parts list identifying mould liners and hydraulic seals with recommended replacement intervals
What to Share Before Requesting a Quotation
Provide the specific interlocking block format and dimensions your market requires, along with the local raw material available — whether that is clay, soil, cement, or fly ash. Share the daily output target and the floor space allocated for the complete line including curing racks. Confirm the site voltage, frequency, and preferred control panel language so the electrical and control configuration is locked before production begins.
Frequently Asked Questions
Q: How is the 6000 pieces per 8-hour figure calculated and which block format does it assume?
A: That capacity figure is provided without a stated basis in the source data. Actual output depends on which of the three mould formats is running, the mix material used, and whether the upstream and downstream stations can sustain the 10-second cycle without interruption. A line layout document specifying the assumed format should be requested before confirming expected daily volumes.
Q: What raw material feeding and mixing equipment does the LY2-10 need upstream for clay versus cement mixes?
A: Clay and soil mixes typically require a pan mixer with controlled moisture addition and a belt feeder that handles sticky material. Cement and fly ash blends work better with a batch mixer and screw feeder for dry powders. The feeding configuration must match the material characteristics and sustain a discharge rate aligned with the 10-second press cycle.
Q: How should pallet size and material be chosen to match the press cycle and the curing setup?
A: Pallets must match the mould footprint across all three formats while fitting the buyer’s existing curing racks and forklift dimensions. Material choice — steel, bamboo, or composite — affects weight, durability, and how the operator handles them during semi-automatic operation. Confirming pallet specs before the line ships avoids costly mismatches on arrival.
Q: What voltage, frequency, and control language options need confirming before the line ships?
A: The electrical configuration must match the site supply to avoid commissioning delays. Control panel language should be set to the operator’s working language. These details are confirmed in a signed document before production, ensuring the machine powers on correctly and the interface is readable from day one at the installation site.



