
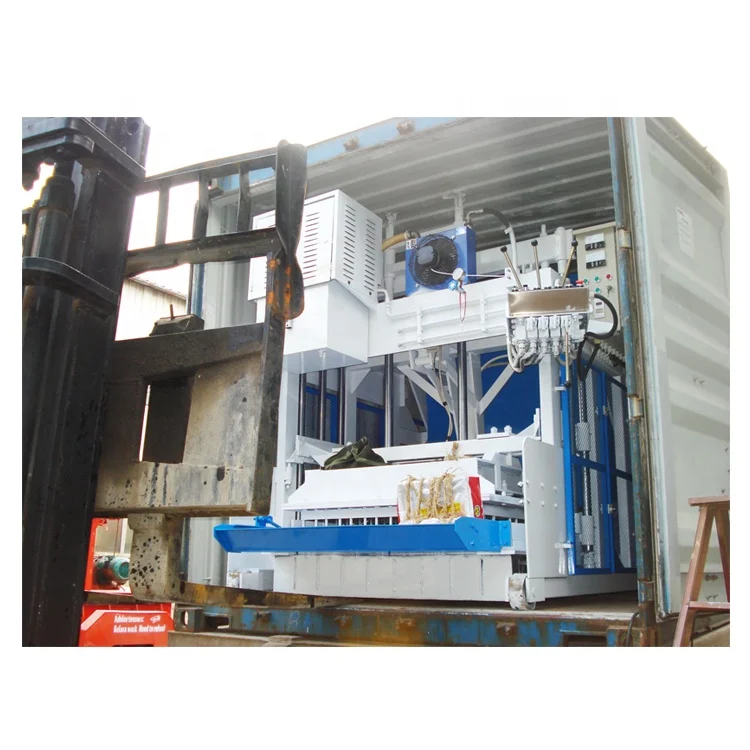
Line-First Configuration — The QMY10-15 mobile block machine is specified here not as a standalone press but as the central station in a matched on-site production line where mixer output, material feed rate, and curing area layout are calculated against the actual block format you intend to produce.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Mobile Concrete Block Making Machine |
| Model | QMY10-15 |
| Mould Capacity | 10 pcs/mould |
| Molding Cycle | 10s–15s (basis not stated in source — confirm block format, material, and thickness) |
| Output Capacity | 11,000 pcs/day over 8 hours (basis not stated in source — confirm block format) |
| Vibration System | Dual vibration motors |
| Hydraulic System | Upper and lower demoulding control with heat dissipator |
| Movement | Electric walking, hydraulic steering |
| Pallet Requirement | None (egg-laying type) |
| Total Power | 16 kW |
| Basic Equipment Included | QMY10-15 host machine, JS7500 concrete mixer, dump truck |
| Optional Equipment | PL1200 batching machine, cement silo, screw conveyor, loader |
Application Suitability
| Application | Material or Output |
|---|---|
| On-site hollow block production at housing project sites | Crushed stone, sand, cement, and water mixed to local aggregate gradation |
| Solid block manufacturing for boundary walls and foundations | Dense aggregate mix with higher cement content for structural load |
| Low-investment first block plant for entrepreneurs | Locally sourced river sand and gravel with standard Portland cement |
| Remote construction site block supply | Mixed aggregate available within short hauling distance of the curing area |
What "11,000 Blocks per Day" Actually Means on a Mobile Block Machine Production Line
The daily output figure is only valid when every upstream station — batching, mixing, and material transport — delivers fresh concrete to the press faster than the molding cycle consumes it.
Many buyers receive a single capacity number without any reference to block format, wall thickness, or curing constraints. A hollow block with thin walls completes its cycle faster than a dense solid block of the same footprint, yet both may be quoted under the same headline figure. On a mobile block machine production line, the press moves across the curing area laying blocks directly on the ground, which means the walking speed, steering precision, and operator rhythm also influence how many cycles fit into an eight-hour shift. When the mixer falls behind or the dump truck is delayed returning from the batching point, the press sits idle and the gap between quoted and actual output widens noticeably [NEED_CITE: common causes of output shortfall in mobile egg-laying block operations].
Matching Mixer Output to the Press Cycle
The JS7500 concrete mixer included in the basic package must produce a batch volume that aligns with the QMY10-15 mould capacity and cycle time. If the mixer takes longer to deliver a homogeneous batch than the press needs to complete one moulding cycle, the operator is forced into a stop-start rhythm that introduces cold joints in the material feed. Adding the optional PL1200 batching machine improves proportioning consistency, which is critical when local aggregate moisture content fluctuates between morning and afternoon batches. The turnkey mobile block making equipment concept only works when material supply is treated as part of the cycle, not as a separate concern.
Curing Area Layout and the Pallet-Free Advantage
Because the QMY10-15 lays blocks directly on the ground in an egg-laying pattern, the curing area does not need pallet inventory, curing racks, or a forklift fleet to move stacked output. However, the ground itself must be level, compacted, and large enough to accommodate eight hours of production spread across multiple rows. Electric walking and hydraulic steering allow the press to traverse between rows without external hauling equipment, but the turning radius and row spacing must be planned before the first block is laid. A site that is too narrow forces the operator into tight maneuvers that extend each cycle beyond the rated molding time [NEED_CITE: site preparation standards for mobile egg-laying block machines].
How Dual Vibration and Hydraulic Pressure Interact
The dual vibration motor system densifies the concrete mix from the bottom of the mould upward, while the hydraulic system controls the upper and lower demoulding strokes to release the formed block without cracking. If vibration force is too high relative to the hydraulic clamping pressure, the mix segregates and coarse aggregate settles at the bottom of the block. If hydraulic pressure dominates, the block releases before vibration has fully compacted the core, resulting in lower compressive strength. The heat dissipator fitted to the hydraulic circuit prevents oil temperature from rising during extended shifts, which keeps demoulding pressure consistent from the first block of the day to the last.
The Hidden Cost of Undersized Supporting Equipment
When the dump truck cycle time is longer than the press consumption rate, the mixer runs empty and the operator waits. Over a full shift, these gaps accumulate into a meaningful shortfall against the quoted daily capacity. Similarly, if the optional cement silo and screw conveyor are added without recalculating the batching accuracy against the local cement grade, the mix design drifts and block strength becomes inconsistent across batches. Buyers who treat the press as the only variable in the line often discover that the real bottleneck was upstream all along [NEED_CITE: production line bottleneck analysis for concrete block plants].
Why Buyers Source This Line Here
Block machinery is the sole product focus at Shandong Shiyue Intelligent Machinery Co., Ltd., so the QMY10-15 is specified together with its mixer, batching unit, and handling accessories as one matched system rather than assembled from separate suppliers. Configuration is set against the buyer’s actual mix design and local aggregate, not pulled from a catalogue default. Mould options cover the formats the buyer’s market demands, including custom drawings when standard moulds do not match local block dimensions. The automation level is selectable — a buyer can start with the basic equipment package and add the PL1200 batching machine or cement silo as production volume justifies the investment. Factory testing is conducted on the buyer’s confirmed block format before dispatch.
Documentation & Verification
- Line layout and capacity calculation stating the block format assumed for daily output
- Machine specification sheet with voltage, frequency, and control language confirmed pre-dispatch
- Mould drawing and format list so the buyer verifies which block types the line will produce
- Hydraulic and electrical schematic for local maintenance reference
- Factory test record on the buyer’s confirmed block format before shipment
- Packing photographs and customs documentation support for import clearance
Installation, Commissioning & Support
- Ground compaction and leveling verified against the 16 kW total power and electric walking path
- Voltage and frequency confirmed to match local supply before the JS7500 mixer motor is wired
- Hydraulic steering calibrated on-site to match curing area row spacing and turning radius
- Dual vibration motor settings adjusted to the buyer’s local aggregate during first production run
- Heat dissipator inspection added to the daily maintenance checklist for extended shift operation
- Mould and hydraulic wear parts list provided with reorder lead times noted
Planning Your Line Configuration
Before requesting a quotation, confirm the block format and wall thickness your market requires, the daily volume you need to sustain, and whether your site can accommodate the curing area footprint for eight hours of continuous egg-laying output. Specify your local voltage, frequency, and preferred control display language so that the electrical package matches your site conditions on arrival. If you already own a loader or concrete transport equipment, indicate the model and capacity so the optional equipment list avoids duplication.
Frequently Asked Questions
Q: How is the 11,000 pieces per day capacity calculated for the QMY10-15?
A: The figure is based on eight hours of continuous operation, but the block format, wall thickness, and material mix assumed in that calculation must be confirmed for your specific project. A thin-walled hollow block cycles faster than a dense solid block of the same footprint. Request a capacity breakdown that states the exact format used as the basis so your expected output is realistic.
Q: What supporting equipment must match the press cycle time?
A: The JS7500 mixer batch volume and discharge rate, the dump truck round-trip time between batching point and press, and the optional PL1200 batching machine proportioning speed must all deliver fresh concrete faster than the QMY10-15 consumes it. When any upstream station is slower, the press idles and daily output drops below expectation.
Q: Can the line start with the basic package and expand later?
A: Yes. The basic equipment package includes the QMY10-15 host, JS7500 mixer, and dump truck. The PL1200 batching machine, cement silo, and screw conveyor can be added when production volume justifies more consistent batching and reduced manual material handling. Line layout should reserve space for future additions.
Q: What voltage and control language are confirmed before shipment?
A: Voltage, frequency, and PLC display language are confirmed during the order stage, not assumed. This ensures the 16 kW electrical system, vibration motors, and hydraulic controls match your local grid and operator language on arrival, avoiding commissioning delays.
Q: How does pallet-free operation affect site preparation?
A: Egg-laying operation eliminates pallet inventory and curing racks, but the curing area ground must be level, compacted, and large enough for eight hours of output spread in rows. The electric walking and hydraulic steering system needs sufficient turning radius between rows to maintain cycle time without tight maneuvers that slow production.



