
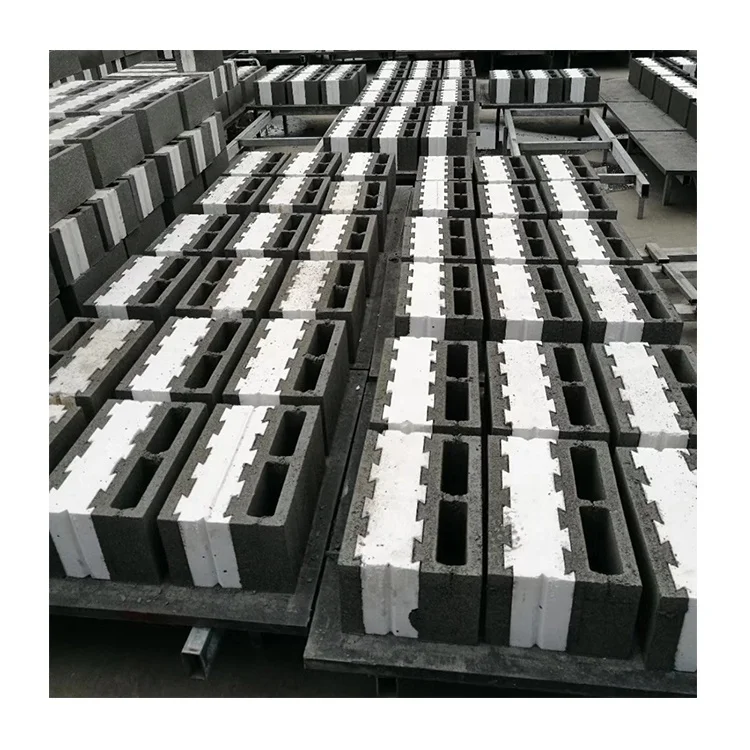
Automatic Concrete Block Making Machine QT6-15 | Complete Line
Matched line pacing — the press, pallet feeder, mixer and conveyor are timed so stations never wait on each other across the QT6-15 production cycle.
Technical Specifications
| Parameter | Value |
|---|---|
| Model | QT6-15 |
| Product Type | Automatic Concrete Block Making Machine |
| Overall Dimensions (L×W×H) | 7400 × 1900 × 2660 mm |
| Molding Cycle | 15–25 s |
| Vibration Frequency | 4600 r/min |
| Exciting Power | 40–50 kN |
| Total Power | 31.25 kW |
| Mixer Model | JQ350 |
| Pallet Size | 850 × 550 × 25 mm |
| Total Weight | 7 T |
| Control System | PLC control system |
| Hydraulic Station | Included |
| Included Equipment | Block making machine, hydraulic station, PLC control system, pallet feeder, brick conveyor, block sweeper |
| Output (400×200×200 mm hollow block) | 1200–1680 pcs/hr (basis stated) |
| Output (400×150×200 mm hollow block) | 1800–2400 pcs/hr (basis stated) |
| Output (240×115×53 mm solid brick) | 3240 pcs/hr (basis stated) |
| Daily Output (8 hr, 400×200×200 mm hollow) | 9600–13440 pcs (basis stated) |
| Daily Output (8 hr, 400×150×200 mm hollow) | 14400–19200 pcs (basis stated) |
| Daily Output (8 hr, 240×115×53 mm solid) | 16200–19440 pcs (basis stated) |
| Applied Products | Paver, solid block, hollow block, curbstone |
| Raw Materials | Crushed stones, sand, cement, dust, fly ash |
| Standards | CE |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow block production for building walls | Crushed stone, sand, cement and fly ash mixes in 400×200×200 mm and 400×150×200 mm formats |
| Solid brick manufacturing for masonry | Standard 240×115×53 mm bricks from local aggregate and cement blends |
| Paver and curbstone production for infrastructure | Interlocking and kerb formats using high-density vibration compaction |
| On-site or fixed-plant block manufacturing | Line configured for locally sourced aggregates including dust and fly ash |
Why the "Pieces per Hour" Figure Fails Without Line Context
A press rated at a given cycle time only reaches that output when every upstream and downstream station keeps pace.
Sellers often quote the Automatic Concrete Block Making Machine production line capacity based on the press alone, ignoring the mixer batch time, pallet feeder interval and conveyor clearing speed. I have watched a QT-class machine sit idle for seconds between cycles because the pallet feeder could not return fast enough, quietly shaving thousands of blocks off the daily count. When the mixer discharges slower than the press consumes, operators start short-dosing the hopper and block weight drifts upward across the shift [NEED_CITE: synchronization standards for concrete block line stations]. The stated capacity is real — but only when the entire line is timed as one system.
Station Timing Across the QT6-15 Line
The 15–25 second molding cycle sets the heartbeat. The pallet feeder must deliver a fresh 850×550×25 mm pallet within that window, the JQ350 mixer must discharge a full batch before the hopper runs low, and the brick conveyor must clear the pressed block before the next cycle begins. The PLC control system coordinates these intervals so no station starves the press.
What Happens When One Station Lags
If the conveyor clears slowly, the sweeper cannot prepare the next pallet in time. The PLC then holds the press, and that 15-second cycle stretches to 20 or more without any alarm sounding — the operator just sees fewer blocks at shift end. I spent three days on a site in West Africa re-tuning feeder and conveyor timers after the line arrived with default settings that did not match the buyer’s pallet weight and curing rack distance [NEED_CITE: typical on-site line synchronization adjustments]. That is why the automatic concrete block making machine production line scope here lists every included station, not just the press.
Reading the Specs Against Your Block Format
Vibration frequency at 4600 r/min paired with 40–50 kN exciting power determines how tightly the mix compacts inside the mould cavity. Higher frequency with lower force suits fine-sand paver mixes; lower frequency with higher force compacts coarse crushed-stone hollow blocks. The hydraulic station provides the clamp pressure that holds the mould rigid during vibration, preventing wall thinning on hollow cores. Pallet size 850×550×25 mm defines the maximum mould footprint and must match the curing rack slot width and the forklift tine spacing already in use at the plant. Total connected load of 31.25 kW across the press, feeder, conveyor and sweeper determines the transformer and dedicated circuit sizing before the line arrives [NEED_CITE: voltage and frequency standards by export market].
The Cost of Skipping Line Integration
Buyers who price the press alone often discover the pallet feeder and conveyor must be sourced separately, arriving weeks later with mismatched voltage and incompatible pallet dimensions. The line then runs in manual mode — operators hand-carry pallets and stack wet blocks on the floor — defeating the purpose of buying automatic equipment. I have seen this gap turn a quoted daily output into half that number until the missing stations finally arrived and were wired into the PLC [NEED_CITE: risks of partial-line concrete block equipment procurement].
Why Procure the Full Line Here
Block machinery is the single focus, so the QT6-15 press, mould, pallet and handling equipment are specified as one matched system rather than assembled from separate suppliers. The configuration is set against your actual mix design, local aggregate and target block format instead of a catalogue default. Mould design covers the formats your market sells, including custom drawings when standard cavities do not fit. Automation level is selectable, meaning a buyer can start with the included pallet feeder and conveyor, then add automatic stacking later. Installation support includes operator training so the crew understands how each station’s timer affects the next.
Documentation & Verification
- Line layout showing pallet feeder, press and conveyor positions with station boundaries marked
- Capacity calculation sheet stating the block format assumed for each output figure
- Pallet specification confirming 850×550×25 mm size, material grade and forklift compatibility
- Hydraulic and electrical schematic showing interlock wiring between PLC and each station
- Voltage, frequency and PLC display language confirmation signed off before production
- Factory test record on your target block format before dispatch
Installation, Commissioning & Support
- Foundation plan sized to the 7400×1900 mm footprint with vibration isolation pads for the 7 T frame
- Dedicated 31.25 kW circuit with voltage and frequency matched to local grid before shipment
- Line arrives in sections for container loading; reassembly supervised on site by technician
- PLC timer parameters tuned to your pallet weight and conveyor length during first-week commissioning
- Operator training covers mould change procedure and daily pallet feeder belt inspection
- Wear parts list for hydraulic seals, vibration springs and sweeper brushes with reorder codes
Before You Send an Inquiry
Share the block formats your market sells along with the daily volume you need per format. Confirm local aggregate types — crushed stone grading, sand source, fly ash availability — so the mixer and mould can be matched to what you can actually buy. State your site voltage, frequency and preferred PLC display language to avoid rewiring after arrival. If you already have curing racks or forklifts, send their dimensions so the 850×550 mm pallet fits your existing handling.
Frequently Asked Questions
Q: How are cycle times matched across pallet feeder, press and conveyor so the press is not starved?
A: The PLC control system sets individual timer values for each station based on the pallet weight, conveyor length and mixer discharge rate. During commissioning these timers are fine-tuned on site so the feeder returns a pallet before the press completes its 15–25 second molding cycle.
Q: Which block format does the stated pcs/hr figure assume?
A: Each output figure is tied to a specific block size — for example 1200–1680 pcs/hr is based on a 400×200×200 mm hollow block. If your primary product is a different format, the realistic hourly output will differ and a revised capacity calculation is provided with the quotation.
Q: Is pallet handling and stacking included in the line scope?
A: The QT6-15 scope includes the pallet feeder, brick conveyor and block sweeper. Automatic stacking and curing rack handling are available as add-on stations. If not selected, blocks leave the conveyor and must be moved to the curing area manually.
Q: How is the line configured against my local aggregate rather than a catalogue default?
A: Before production, the mix design is reviewed against your locally available crushed stone, sand and fly ash. The mixer batch size, vibration frequency and hydraulic pressure are then adjusted so block density meets your market strength requirement without forcing a material change.
Q: What voltage, frequency and PLC language will be confirmed before shipment?
A: Your site voltage, frequency and preferred PLC display language are confirmed in writing before production begins. This ensures the electrical cabinet and control interface match local standards and the operator can read the screen on day one.



