
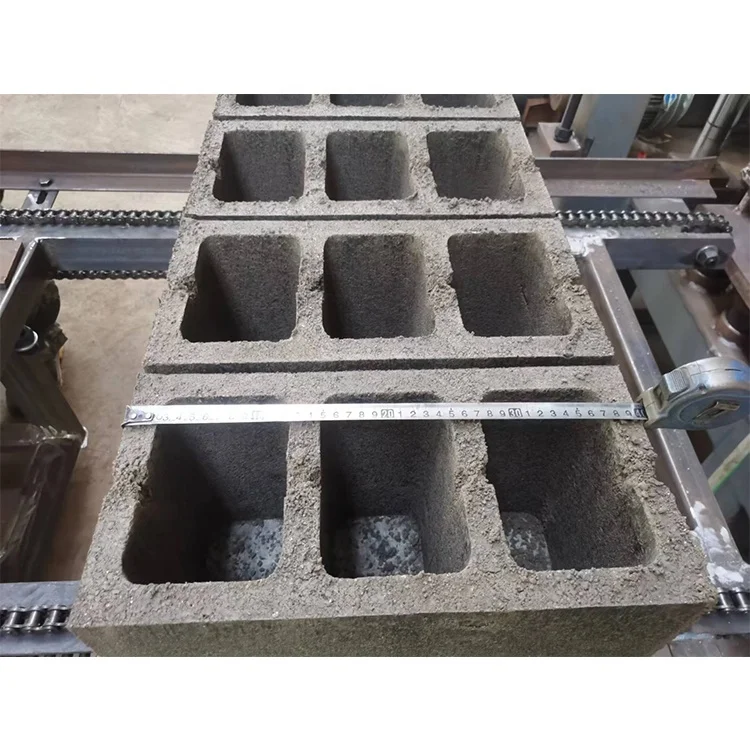
Matched System Engineering — the QT4-16 block production line supporting equipment is specified so every station from batching to stacking keeps pace with the press cycle, preventing the idle time that silently cuts real daily output.
Technical Specifications
| Parameter | Value |
|---|---|
| Product Type | Stationary Concrete Block Making Machine |
| Model | QT4-16 |
| Overall Dimensions (L×W×H) | 7400 × 1950 × 2800 mm |
| Total Mass | 5 T |
| Rated Hydraulic Pressure | 21 MPa |
| Main Vibration Form | Platform Vibration |
| Vibration Frequency Range | 2800–4500 r/min |
| Vibration Force | 40 kN |
| Pallet Size | 900 × 550 mm |
| Demolding Method | Hydraulic |
| Control System | PLC with man-machine interface, malfunction diagnosis, remote monitoring |
| Machine Frame Material | Manganese steel (China national standard) |
| Oil Hydraulic System | Built to international standard |
| Recommended Factory Area | 600 m² |
| Molding Cycle | 15–20 s (basis not stated in source) |
Application Suitability
| Application | Material or Output |
|---|---|
| Hollow and solid block manufacturing | Crushed stone, sand, cement, fly ash, gravel, slag |
| Paving block and interlocking brick production | Aggregates blended with cement and pigment |
| Curbstone and colored paver forming | Dense aggregate mixes requiring high hydraulic pressure |
| On-site stationary plant operations | Locally sourced raw materials including dust and fly ash |
Why the Press Is Never the Actual Bottleneck
A stationary block machine only delivers its rated output when every upstream and downstream station matches its cycle. The QT4-16 block production line supporting equipment is configured as a synchronized system so the press is never left waiting for pallets, raw mix, or stacking clearance.
I have walked onto sites where a perfectly capable press sat idle for minutes each cycle because the mixer discharged too slowly or the pallet return conveyor jammed under wet concrete splash. The result is always the same: daily throughput falls to a fraction of the quoted figure, and the buyer blames the machine. When the batching station, pallet feeder, stacker, and curing rack handler are engineered around the same cycle target, those gaps close. [NEED_CITE: typical causes of idle time in stationary block plants]
How Each Station Connects to the QT4-16 Cycle
The platform vibration cycle on the QT4-16 completes a molding stroke in a matter of seconds, which means the raw material feed must discharge a measured batch into the hopper before the next cycle begins. If the mixer is undersized or the belt conveyor runs at a fixed speed that does not match the press rhythm, the hopper starves and the PLC flags a feed fault. Sizing the mixer volume and conveyor speed to the actual block format being run is the first step in QT4-16 block production line supporting equipment configuration.
Downstream, the 900 × 550 mm pallet exits the press carrying a freshly molded block. The wet block must be transferred to a curing rack without jolting, stacked in layers that allow air circulation, and eventually cubed for dispatch. Each of these movements is a station that either runs in time with the press or forces the entire line to slow down.
Matching Pallet Circulation to Your Curing Area
The pallet is the single item that travels through every station — press, stacker, curing rack, and return conveyor. Choosing a pallet material and thickness without checking what your existing forklift can lift, or whether your curing racks accept a 900 × 550 mm footprint, creates a mismatch that shows up on day one of production. We confirm pallet specifications against your current infrastructure before the line is built. [NEED_CITE: pallet handling compatibility standards in block manufacturing]
What the Numbers on the Spec Sheet Actually Mean
The 21 MPa rated hydraulic pressure works together with 40 kN of platform vibration force to compact the mix into the mould cavity. Higher pressure alone produces a dense block but risks sticking; vibration alone gives a clean release but lower strength. The QT4-16 pairs both so that hollow blocks with thin walls achieve structural density without cracking during demolding. The 2800–4500 r/min vibration frequency range allows the operator to dial in the setting that suits the aggregate gradation — coarser crushed stone generally needs higher frequency, while fly-ash-heavy mixes respond better at the lower end.
The manganese steel frame absorbs the repeated shock of vibration cycles without fatigue cracking, which matters on a machine running continuous shifts. The PLC control with malfunction diagnosis monitors hydraulic pressure, vibration motor current, and pallet position sensors, flagging anomalies before they escalate into a line stoppage.
The Cost of Leaving Supporting Stations Off the Quotation
Buyers who receive a quotation for the press alone often discover that pallet feeding, stacking, and curing rack handling were never included. Finished blocks pile up at the press exit, workers move them by hand, and the press waits while the exit area is cleared. This pattern repeats every shift, and the real output never approaches what the machine is mechanically capable of producing. [NEED_CITE: impact of manual pallet handling on block plant throughput]
Voltage, frequency, and PLC display language are sometimes left unconfirmed until the machine arrives. A 50 Hz machine running on a 60 Hz supply will vibrate at the wrong frequency, producing blocks with inconsistent density — a problem that is not obvious until the first batch fails a strength test.
Why Source the QT4-16 Line Here
The QT4-16 and its QT4-16 block production line supporting equipment are specified as one matched system rather than assembled from separate vendors, so cycle times are calculated across every station before the line is built. Mould design covers the block formats your market actually sells, including custom drawings when standard moulds do not fit the product range. Automation level is selectable, so a buyer can commission a semi-automatic line today and add automatic stacking or cubing later without replacing the press.
The factory test runs the complete line — mixer, press, pallet return, and stacker — before dismantling for shipment, so timing issues surface in the workshop rather than on your floor. Installation support includes operator training focused on the PLC interface, mould change procedure, and daily maintenance checkpoints specific to this configuration.
Documentation & Verification
- Line layout drawing showing each station footprint and material flow path for the QT4-16
- Capacity calculation stating the specific block format and mix design assumed
- Pallet material and dimension specification matched to your curing rack system
- Hydraulic and electrical schematic with PLC I/O mapping
- Factory test record covering press cycle, pallet circulation, and stacker timing
- Operation and maintenance manual with wear parts and mould replacement list
Installation, Commissioning & Support
- Foundation plan sized for the 7400 × 1950 mm machine footprint and 5 T operating mass
- Power supply confirmation for voltage, frequency, and dedicated circuit rating before dispatch
- PLC display language set to operator preference during factory configuration
- On-site commissioning with cycle timing verification across every connected station
- Mould change training covering hydraulic release and alignment for each block format
- Wear parts list with reorder intervals for vibration springs, hydraulic seals, and pallet guides
What We Need to Size Your Line
Send us the block formats you plan to produce, the daily volume target for each, and the raw materials available locally including aggregate type and gradation. Confirm your workshop dimensions and ceiling height, the voltage and frequency at your site, and whether you have existing curing racks or forklifts the line must integrate with. If you are replacing a press in a running plant, share your current pallet size and any upstream or downstream equipment that stays in place.
Frequently Asked Questions
Q: How is daily output calculated for each block format on this line?
A: Output depends on the specific mould loaded, the mix design, and the curing time required. We provide a capacity table showing cycle time per format — hollow, solid, paver — so you can calculate daily volume based on your actual shift length and the formats your market demands, rather than a single generic figure.
Q: Which supporting equipment stations must match the QT4-16 to prevent idle time?
A: The raw material batching and mixing station, pallet feeder, exit conveyor, automatic stacker, and curing rack handler must each complete their movement within the press cycle window. If any station runs slower, the PLC pauses the press and real throughput drops accordingly.
Q: Can the 900 × 550 mm pallet work with my existing curing racks and forklift?
A: We confirm this before production starts. Share your rack slot dimensions and forklift fork width so we verify compatibility. If your existing infrastructure uses a different pallet footprint, we adjust the line design or recommend the pallet change needed to avoid handling bottlenecks.
Q: Does the PLC control connect to batching accuracy and stacking automation?
A: The PLC manages press cycle logic, malfunction diagnosis, and remote monitoring. It communicates with the batching system to time material discharge and with the stacker to coordinate pallet release. Batching precision and stacking speed are configured during commissioning to match your production rate.
Q: Does the quotation cover the full line or just the press?
A: Our standard quotation specifies every station — mixer, press, pallet system, stacker, and curing rack handling — as one package. If you only need the press, we note which supporting equipment you are sourcing separately and confirm that its cycle timing is compatible.


